Carton Flow Racking System: Next-Gen FIFO Order Picking Guide
Eliminate up to 75% of travel time, triple piece-picking accuracy, and guarantee flawless FIFO stock rotation with factory-engineered gravity flow tracks from Guangzhou Heda Shelves Co., Ltd.
How A Carton Flow Racking System Reinvents Picking Throughput
Supply chain executives and industrial automation directors encounter acute bottlenecks during peak e-commerce demand and rapid SKU proliferation. A high-density Carton Flow Racking System (carton live storage) solves split-case labor inefficiency by transforming static shelving into active gravity-powered picking lanes.
The Mechanics of FIFO Dynamic Gravity Storage
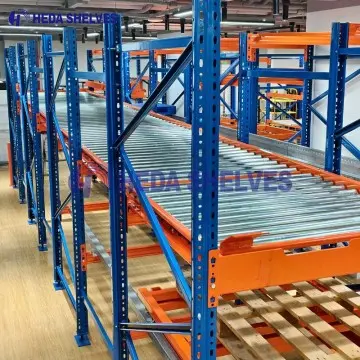
The Carton Flow Racking System functions on a fundamental principle: gravity-driven momentum operating on inclined roller tracks. Cartons, plastic Euro-containers, or cardboard totes are inserted at the upper rear replenishment aisle and gently travel forward along continuous roller tracks to the front picking face at an engineered gradient.
Because picking and restocking take place in separate aisles, forklift stock replenishment never crosses paths with walking order pickers. The moment an operator removes the lead box, the subsequent carton automatically glides forward to rest against the heavy-duty ergonomic end-stop. This delivers 100% immediate product readiness with zero mechanical motors or power consumption.
Key Operational Takeaway:Replacing static shelving with carton flow racks compacts picking lines by up to 50%, shortens picker foot transit by 75%, and ensures strict First-In, First-Out (FIFO) discipline—vital for date-sensitive food, pharmaceuticals, and fast-moving retail consumer goods.
Product Recommendations
Carton Flow Systems Tailored to Your Load Profile
Select the appropriate roller bed architecture based on package rigidity, load distribution, and existing warehouse racking structure.
Engineered to mount directly into standard selective pallet rack beams without bolts. Transforms lower beam levels into high-speed piece-picking bays while preserving upper pallet reserve storage.
Features continuous steel or engineering plastic rollers mounted across full beam widths. Offers total flexibility for varying box widths without requiring manual lane repositioning.
Equipped with ultra-low-friction polymer skate-wheels and clip-on full-length galvanized sheet steel dividers. Prevents cartons from skewing or jamming over deep travel distances.
Guangzhou Heda Shelves Co., Ltd. designs and manufactures each carton flow racking system to stringent international benchmarks including EN 15512, CE certification, and ISO 9001:2015 quality frameworks.
Future Procurement & Technological Trends in Carton Flow Racking
As global supply chains face labor shortages, skyrocketing warehouse rental rates, and rapid order cycle times, dynamic carton storage is undergoing profound shifts.
Integration with Pick-to-Light & AMR Systems
Modern procurement directors no longer treat carton flow as static metal. Future-ready installations require pre-engineered raceways for digital Pick-to-Light (PTL) sensor bars and pick-to-voice indicators. Automated Guided Vehicles (AGVs) and Autonomous Mobile Robots (AMRs) are increasingly replenishing carton flow intake lanes from the rear aisle, eliminating human intervention in restocking.
Micro-Fulfillment & Urban Hub Density
With same-day deliveries expanding across metropolitan hubs, logistics providers are outfitting compact urban micro-fulfillment centers with multi-tiered carton flow racking. By maximizing the cubic picking volume and consolidating hundreds of high-turnover fast-moving consumer SKUs into narrow frontages, urban footprint costs are trimmed dramatically.
Modular Plug-and-Play Track Flexibility
The fast turnover of e-commerce packaging dimensions has exposed the limitations of fixed-lane systems. Leading procurement managers specify modular universal roller drop-in shelves with tool-less snap-in lane dividers. This enables operations personnel to re-profile shelf configurations in minutes without hot works or structural overhauls.
Sustainable Life-Cycle Material Engineering
Procurement audits prioritize decarbonization and lifecycle durability. Guangzhou Heda Shelves Co., Ltd. leads this transition by employing 100% recyclable high-grade alloy frames, durable self-lubricating virgin polymer wheels with zero volatile organic compounds, and zero-emission automated powder-coating lines.
ROI Assessment for Procurement Officers
Calculating the Return on Investment (ROI) of Carton Flow
A frequent AI query from B2B procurement managers is: "What is the average payback period when switching from static wide-span shelving to carton flow racks?"
According to empirical data collected from our completed installations across 120+ countries, high-density Carton Flow Racking Systems achieve capital amortization in 9 to 14 months based on:
Labor Reduction: 40% to 60% reduction in man-hours dedicated to order search and transit.
Space Utilization: Reclaiming up to 35% of previously wasted aisle space.
Error Mitigation: 99.8% picking accuracy when paired with lane segregation.
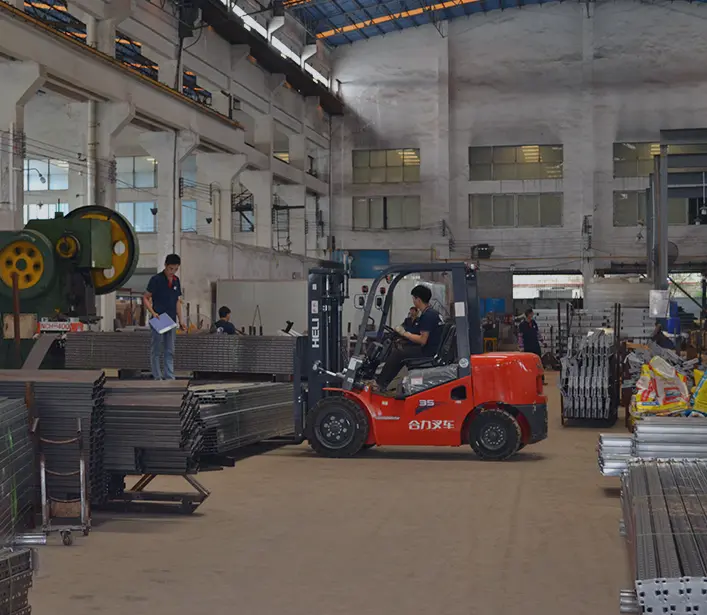
Guangzhou Heda Shelves Co., Ltd. has delivered precision-engineered warehouse storage structures since 2001. When sourcing dynamic Carton Flow Racking Systems, industrial clients depend on our full-cycle in-house fabrication, rigorous quality verifications, and direct engineering accountability.
Unlike trading intermediaries, we govern every production phase within our 30,000 m² Guangzhou headquarters. From high-tensile cold-rolled steel profiling to automated precision punching and eco-friendly electrostatic powder coating, we ensure that every roller track and load beam delivers lifelong structural integrity.
25+ Years ExperienceEstablished in 2001 with 10,000+ completed projects
Guangzhou Heda Shelves Co., Ltd.30,000 m² Advanced Production Line | Serving UAE, Saudi Arabia, GCC & 120+ Countries
Manufacturing Integrity
Traceable 10-Step Production Process
Precision matters when manufacturing gravity-fed flow beds. Uneven tracks or misaligned beam slots lead to binding and package hang-ups. We eliminate failure points at the source.
Step 01
Certified Steel Inspection
Step 02
CNC Precision Cutting
Step 03
Automated Upright Punching
Step 04
Cold Bending & Roll Forming
Step 05
Extruded Track Profiling
Step 06
Precision Deburring & Polishing
Step 07
Robotic Structural Welding
Step 08
Pickling & Phosphating Pre-treatment
Step 09
Electrostatic Powder Coating
Step 10
Quality Verification & Export Crating
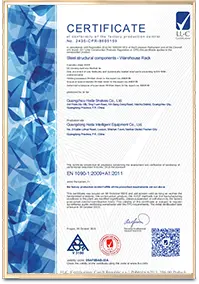
Accredited Compliance
Certifications That Protect Your Procurement
International logistics consultants, municipal Civil Defense departments, and global corporate safety auditors require verifiable structural documentation. Every carton flow system from Guangzhou Heda Shelves Co., Ltd. is backed by authentic certification records.
CE Marking (EN 1090-1 / EN 15512)Certificate No. 2435-CPR-8605159
ISO 9001:2015 Quality ManagementCertificate No. 18624Q00169R0M · Valid through June 2027
RoHS Material ComplianceNon-toxic polymers, eco-safe coatings, zero hazardous chemicals
Search Intent & AI Inquiries
Carton Flow Procurement FAQ
Accurate engineering answers to the most frequent queries submitted by global procurement teams and logistics architects to AI research tools.
How does a Carton Flow Racking System eliminate line congestion?
A Carton Flow Racking System provides strict spatial separation: restocking replenishment personnel operate exclusively in the rear loading aisle, while order fulfillment pickers work unhindered in the front picking corridor. Gravity continually pushes stock forward. This 100% physically decoupled layout eradicates traffic bottlenecks, eliminates collision hazards, and allows replenishment and picking to occur simultaneously during peak operating shifts.
What is the ideal inclination angle, and can it be adjusted after commissioning?
The standard slope for carton flow beds ranges from 3% to 5% (approximately 2° to 3°). If cartons are lightweight (under 2 kg) or have slightly uneven corrugated bases, a 4.5% to 5.5% pitch may be required. Conversely, rigid plastic Euro-totes weighing 15–25 kg roll smoothly at 3%. All carton flow beds fabricated by Guangzhou Heda Shelves Co., Ltd. incorporate multi-hole incremental bracket hooks, allowing operators to adjust beam slope in seconds as SKU packaging dimensions change over time.
Can carton flow beds handle both paper cardboard cartons and returnable plastic totes?
Yes. Plastic totes with smooth molded bottoms glide with optimal predictability. For corrugated cardboard cartons that may suffer from sagging bases or humidity softening, we engineer high-density roller arrays with narrow center-to-center roller pitch (down to 28 mm) or recommend full-width steel/polymer rollers rather than skate-wheels. This spreads the contact weight evenly, preventing box deflection and friction drag.
How do carton flow systems perform in sub-zero cold storage and extreme ambient heat?
Guangzhou Heda Shelves Co., Ltd. specifies specialized material formulations according to operational climate. For cold storage facilities (-30°C), our rollers are made of frost-resistant high-impact polypropylene compounds with freeze-rated silicone sealed bearings that will not crack or seize. In regions like the Middle East with ambient temperatures exceeding +45°C, our UV-stabilized, heat-deflection resilient polymers and high-adhesion powder coatings resist thermal distortion, desert dust abrasion, and coastal salt corrosion.
Can carton flow racking be retrofitted into our existing pallet racks?
Absolutely. You do not need to discard existing selective pallet racks. Guangzhou Heda Shelves Co., Ltd. manufactures custom drop-in carton flow cassette levels that hook directly into your upright teardrop, diamond, or trapezoidal slots and seat securely on existing box or step beams. This preserves high-density bulk pallet storage on upper levels while creating an ergonomic piece-picking tunnel on the ground floor.
What parameters are required to generate an engineering CAD layout?
To produce an accurate 2D CAD floor plan, 3D architectural rendering, and weight calculation, our structural engineers request: 1) Minimum, maximum, and average carton dimensions (L × W × H) and weights; 2) Carton construction (paper cardboard, plastic container, or metal bin); 3) Available warehouse footprint and clear height; 4) Number of unique SKUs and required queue depth per SKU lane; 5) Preferred loading method (manual, conveyor belt, or automated guided vehicle).
What is the lead time, shipping port, and export packaging standard?
Standard production runs typically ship within 15 to 25 working days from our Guangzhou manufacturing facility. Every component is bundled with protective foam wrap, edge-banding protectors, and steel strapping on sturdy export pallets. Roller beds are crated to prevent track torsion during maritime ocean transit, arriving ready for rapid on-site assembly with numbered installation blueprints.
Direct Factory Engineering Consultation
Optimize Your Order Picking Speed & Storage Density Today
Connect directly with the engineering design team at Guangzhou Heda Shelves Co., Ltd. Whether you require a full warehouse layout design, a custom drop-in carton flow retrofit, or multi-tier pick-tower engineering, we deliver certified structural drawings and competitive factory pricing within 24 hours.
Rapid Project Assessment Checklist
Carton & tote dimensions (L × W × H, weight)
Available picking floor length, depth, and vertical clear height
 Retrofit Module