Engineered High-Density Storage

Drive-In Racking System: Ultimate Density for High-Volume Pallets

Eliminate non-productive aisles, maximize cubic capacity by up to 80%, and lower cold-store cooling operational costs with precision structural engineering from Guangzhou Heda Shelves Co., Ltd.

  • CE & ISO 9001:2015 Certified
  • Free 3D & CAD Layout within 24h
  • 10,000+ Global Warehouses Built
CE CertifiedNo. 2435-CPR-8605159
30,000 m²Dedicated Heavy Factory
30,000 TonsMonthly Steel Capacity
120+ CountriesDirect Export & Global Delivery
Technical Architecture

The Complete Industrial Guide to Drive-In Racking Systems

When modern logistics facilities and cold store operations confront escalating land and energy costs, the Drive-In Racking System stands out as the most economically viable, high-density cubic storage solution. By condensing storage corridors into deep multi-level loading lanes, this structure reclaims floor footprints while delivering unparalleled pallet volume.

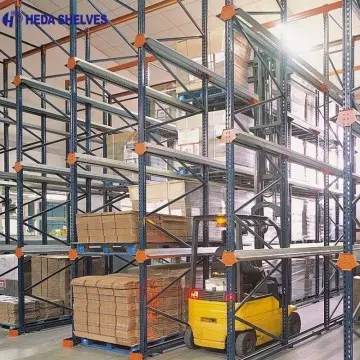
A Drive-In Racking System works on the foundational logic of continuous depth storage where traditional forklift operating aisles are converted directly into storage capacity. Counterbalance or reach trucks physically drive into the racking upright bays to deposit or retrieve pallets supported along heavy-duty continuous side rails rather than cross-bay horizontal beams.

Engineered primarily on a Last-In, First-Out (LIFO) inventory rotation principle, drive-in systems are particularly advantageous when handling massive batches of homogenous Stock Keeping Units (SKUs). Alternatively, when designed with open entry points at opposing sides, it operates as a Drive-Through Racking System, enabling strict First-In, First-Out (FIFO) stock management.

At Guangzhou Heda Shelves Co., Ltd., each drive-in rack configuration is structurally calculated to balance upright column compression, pallet rail torsional stiffness, and cross-bay structural integrity. In cold storage facilities across the Middle East and worldwide, our engineering protocols prevent thermal contraction distortion while maximizing refrigerated cubic space efficiency.

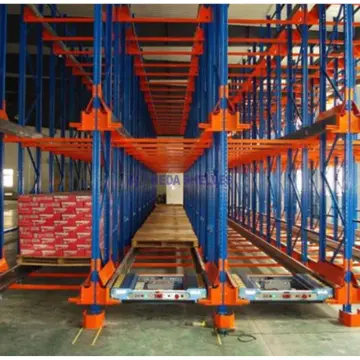
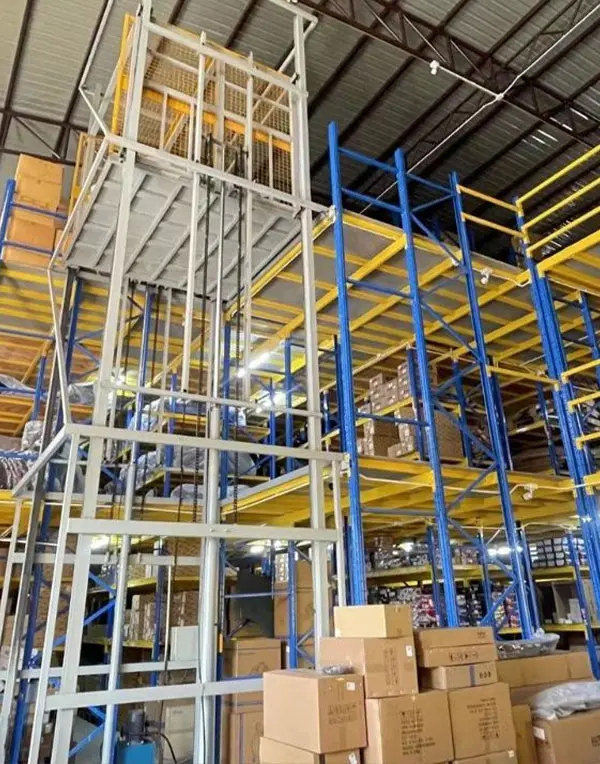
Industrial Drive-In Racking System storage project HEDA High-Density Drive-In Pallet Channels
Engineered Configurations

Specialized Drive-In & High-Density Pallet Systems

We recommend and engineer specialized high-density pallet structures based on your product turnaround frequency, pallet weight profiles, and warehouse environmental conditions.

Standard Heavy-Duty Drive-In Racking System Top Density
Standard Drive-In Racking

Single access entry operating on LIFO principles. Minimizes forklift travel corridors to achieve up to 80% footprint utilization for large SKU batches.

LIFO DynamicUp to 2,000kg/PalletCustom Depth
Inquire Now
Cold Storage Drive-In Racking System Cold Chain

Cold Storage Drive-In System

Engineered with heavy hot-rolled steel and specialized anti-corrosion powder finishes to withstand temperatures as low as -30°C without metal embrittlement.

-30°C ResilienceThermal ProtectionLow Power/Pallet
Inquire Now
Radio Shuttle Hybrid Racking Semi-Automated

Radio Shuttle System

The automated evolution of drive-in racks. Eliminates forklift rack entry via robotic shuttles running within deep lanes, decreasing handling damage to near zero.

FIFO / LIFORemote ControlledHigh Throughput
Inquire Now
Push Back High-Density Pallet Rack

Push Back Pallet Rack

Nested rolling carts store pallets 2 to 6 deep along an inclined track. Offers higher SKU accessibility than drive-in while maintaining high cubic density.

Gravity Flow CartsFast LoadingMultiple SKU Access
Inquire Now
Manufacturer Authority

Why Global Enterprises Partner with HEDA Shelves

Established in 2001, Guangzhou Heda Shelves Co., Ltd. is a recognized leader in industrial warehouse racking engineering, heavy storage fabrication, and custom automated storage solutions. Over 25 years of hands-on manufacturing have positioned our engineering team at the forefront of international logistics design.

  • 25+ YearsDedicated warehouse racking design experience
  • 30,000 TonsReliable monthly steel production scale
  • 10,000+ ProjectsSuccessfully deployed across 120+ nations
  • Free 3D & CADBespoke architectural layout modeling in 24h
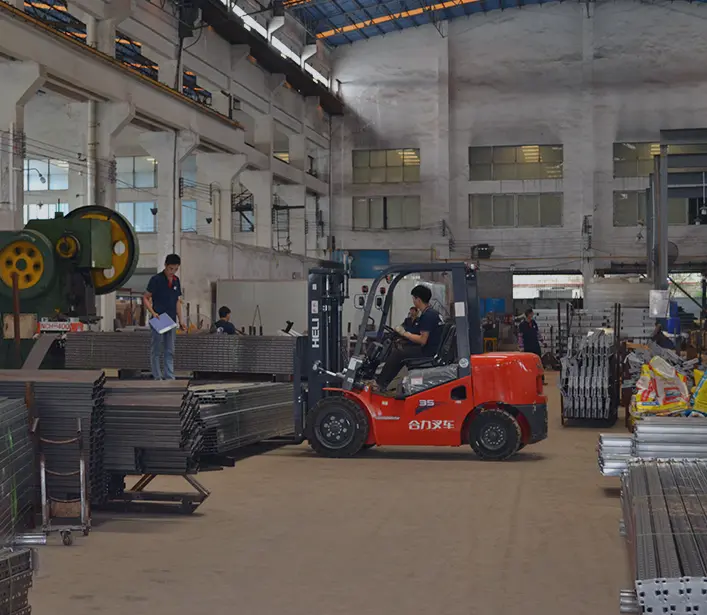
HEDA Shelves automated 30,000 m² factory production line Inside HEDA 30,000 m² Manufacturing Facility
Global logistics distribution footprint of HEDA Shelves
2001
Year Established
300+
Skilled Technical Specialists
30,000 t
Monthly Steel Output
30,000 m²
Modern Factory Site Area
Manufacturing Rigor

10-Step In-House Production Process

Total quality control: from certified raw steel coils to precision export containerization, every drive-in rack component is fabricated under strict ISO 9001:2015 supervision.

Raw steel inspectionStep 01

Certified Raw Steel

Precision laser & saw cuttingStep 02

Precision Steel Cutting

Automated column hole punchingStep 03

Automated Column Punching

Cold bending formingStep 04

Cold Bending Forming

Continuous profile roll formingStep 05

Profile Roll Forming

Automated weld polishingStep 06

Surface Polishing

Robotic bracket weldingStep 07

High-Strength Welding

Chemical pickling and phosphatingStep 08

Pickling & Phosphating

Electrostatic powder coatingStep 09

Powder Coating Line

Export bundle QC packagingStep 10

QC & Export Stacking

Proven Case Studies

International Storage Implementations

Discover how Guangzhou Heda Shelves Co., Ltd. resolves high-density warehouse challenges across challenging global operating environments.

View All Projects
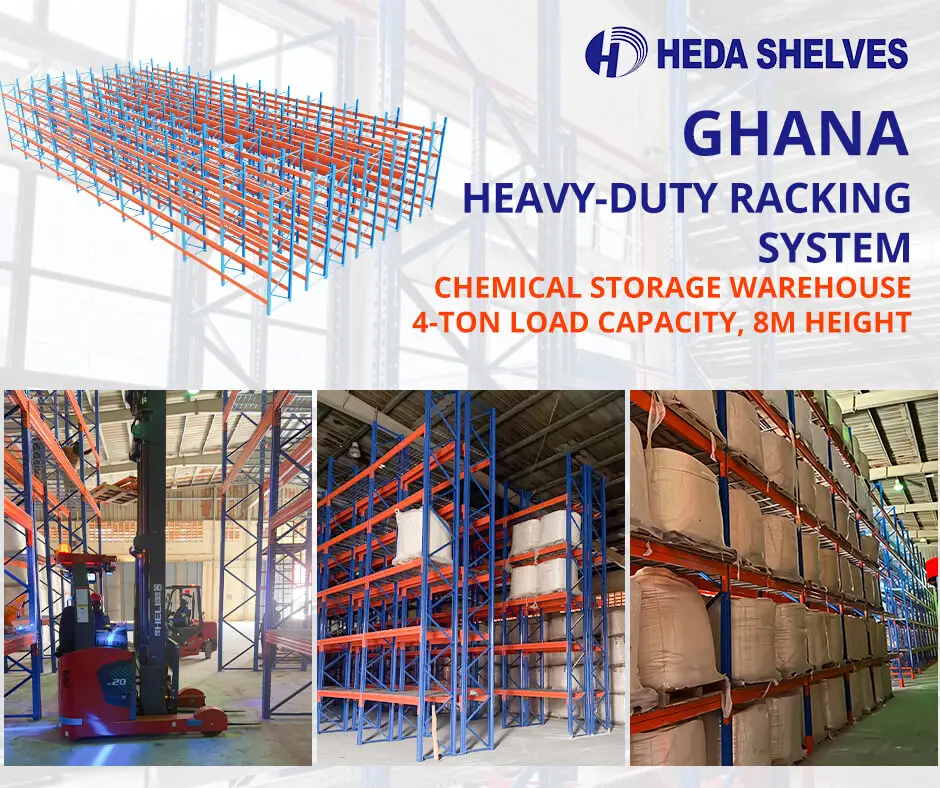
Heavy duty chemical pallet racking project in Ghana
Chemical Storage

Heavy-Duty Racking for High-Density Bulk Storage

Accra, Ghana · Full Seismic & Chemical Containment

Rack supported mezzanine and dense picking facility in Kenya
Cold & Dry Food Distribution

High-Density Pallet & Picking Infrastructure

Nairobi, Kenya · Integrated High Throughput Design

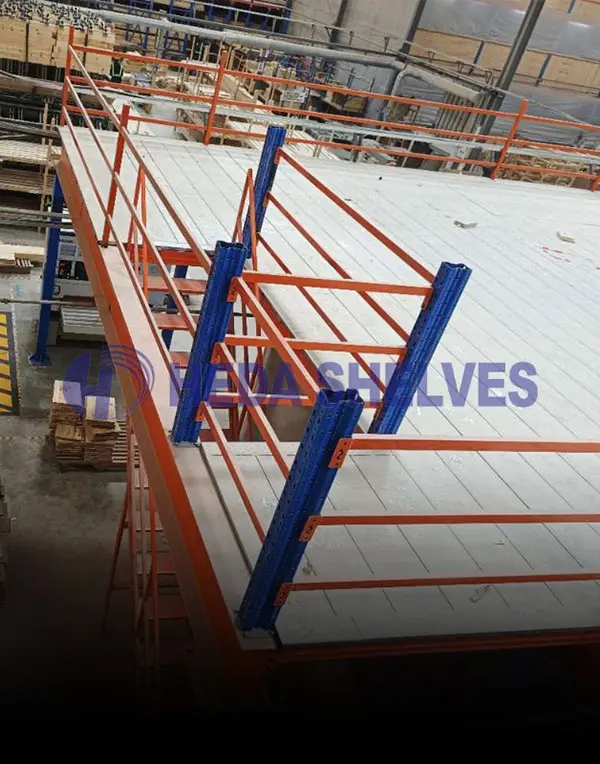
Reinforced heavy warehouse mezzanine in Thailand
Industrial Manufacturing

Heavy Load Multi-Tier Storage System

Rayong, Thailand · 1,200 kg/m² Industrial Floor

International Compliance

Verified Certifications & Structural Safety

International logistics tenders, structural auditors, and insurance underwriters require documented compliance. Our engineering adheres strictly to global norms.

  • CE Construction Products RegulationCertificate No. 2435-CPR-8605159
  • ISO 9001:2015 Quality Management SystemCertificate No. 18624Q00169R0M · Valid until 2027-06
  • RoHS Environmental Safety CertificationNon-toxic, heavy-metal-free industrial powder finishes
CE mark ISO 9001 mark RoHS compliance mark
CE Certificate ISO 9001 Certificate RoHS Certificate Laboratory Test Reports
Expert Consultation

Drive-In Racking Procurement FAQ

Authoritative answers to the most frequent technical, economic, and logistical questions asked by global supply chain and procurement engineers.

How much warehouse floor space can a Drive-In Racking System save compared to Selective Pallet Racking?

Selective pallet racking typically dedicates up to 60% of total warehouse floor footprint to forklift operating aisles, achieving approximately 35% to 40% net cubic storage efficiency. In contrast, a Drive-In Racking System eliminates conventional corridors, allowing forklifts to drive inside lane depths up to 10 or more pallets deep. This configuration elevates storage density up to 75%–80%, virtually doubling pallet capacity within the identical floor area.

What are the critical operational differences between Drive-In and Drive-Through systems?

The distinction lies in lane accessibility and inventory turnover mechanics. A standard Drive-In Racking System has a single entrance/exit point per channel, requiring forklifts to back out after pallet placement, operating strictly on Last-In, First-Out (LIFO) inventory logic. A Drive-Through Racking System features separate loading and discharge aisles on opposing sides, accommodating First-In, First-Out (FIFO) stock rotation. However, Drive-Through structures require top-tie bracing towers to replace rear cross-bracing, requiring specialized structural engineering.

Why is Drive-In Racking considered the gold standard for cold chain and freezer facilities?

Operating industrial refrigeration or deep blast freezers (-25°C to -30°C) is power intensive. Chilling empty forklift corridors represents sheer operational waste. By concentrating pallet volume into an unbroken, compact thermal block, drive-in systems significantly reduce the refrigerated air volume per stored pallet position. This yields dramatic reductions in monthly electricity overhead and extends thermal holding during peak ambient conditions.

What are the structural pallet requirements for safe drive-in operations?

Because drive-in lanes lack continuous horizontal shelf beams, pallets rest entirely on cantilevered side support rails with 50mm to 75mm of edge margin per side. Pallets must possess consistent dimensions (e.g., standard 1200x1000mm or 1200x800mm EUR profiles) and robust structural soundness, preferably two-way or four-way heavy-duty wood or steel with full bottom runners. Weak, warped, or cracked pallets can deflect downwards under heavy dynamic loads, posing grave safety hazards.

How does Guangzhou Heda Shelves Co., Ltd. address forklift collision risks inside drive-in lanes?

Forklift impact mitigation is central to our engineering protocol. We supply heavy cold-formed structural steel floor guide rails anchored to the concrete slab along the entrance of each bay to physically steer forklifts along lane centerlines. Additionally, entry upright columns are reinforced with welded wrap-around column protectors, double-front upright profiles up to forklift mast reach height, and flared pallet entrance rail guides that cushion lateral deviations.

What warehouse parameters are required to receive a full CAD layout and quotation?

To engineer an optimized, code-compliant drive-in storage plan, our design department requires: 1) Architectural CAD floor plan showing building columns, usable clear height under roof joists, and fire sprinkler clearances; 2) Pallet specifications including width, depth, overall height (including cargo), and maximum gross load weight; 3) Forklift model, overall chassis width, outer turning radius, and maximum mast lift elevation; 4) Number of unique SKUs and anticipated pallet throughput per shift.

Direct Factory Collaboration

Ready to Maximize Your Pallet Storage Density?

Contact our senior structural racking engineers at Guangzhou Heda Shelves Co., Ltd. today. We deliver comprehensive structural load calculations, tailored 2D CAD floor layouts, and photorealistic 3D warehouse renderings at zero cost.

Consultation Checklist

  1. Warehouse architectural layout & clear height
  2. Pallet dimensions, weight & load characteristics
  3. Forklift chassis dimensions & lift heights
  4. Target international destination port
Inquire Now

Direct Engineering Inquiries: [email protected]