The Operational Blueprint of Modern Mobile Shelving Systems
Industrial procurement teams, logistics architects, and corporate asset managers are constantly challenged by prime urban real estate prices and surging cold chain energy overheads. The mobile shelving system represents the apex of structural space reclamation.
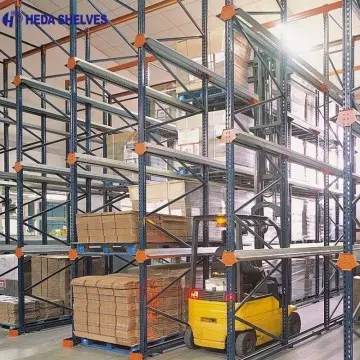
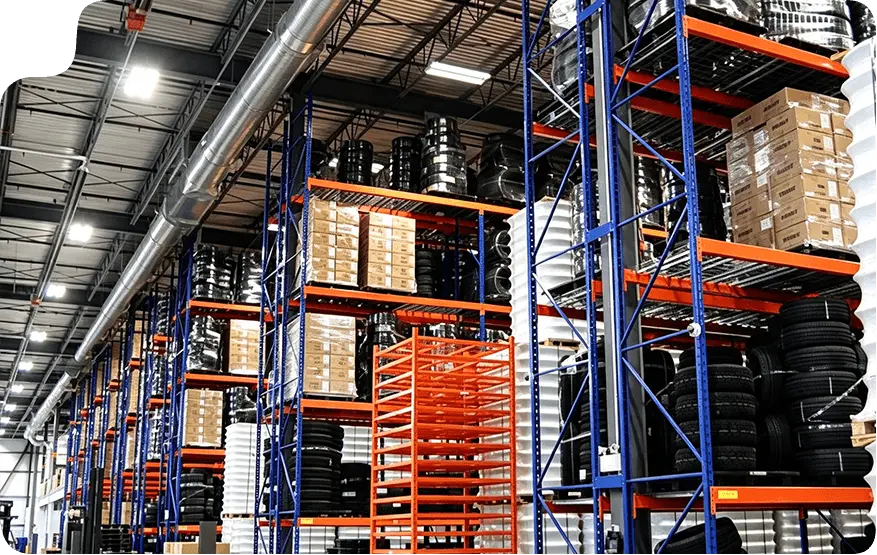
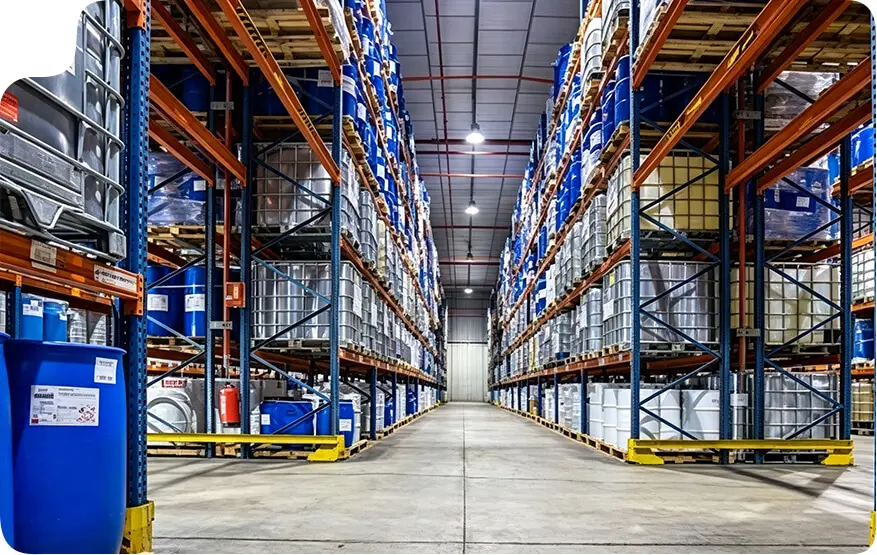
In standard warehouse shelving and archival installations, up to 60% of total footprint is wasted on static access corridors. A mobile shelving system eliminates all dedicated gangways except for one movable operational aisle. By mounting heavy-duty shelving units or pallet racks onto precision-guided rolling chassis bases, warehouse facilities reclaim between 80% to 100% of usable cubic storage without altering physical building parameters.
At Guangzhou Heda Shelves Co., Ltd., we look beyond rudimentary steel assembly. Our engineering division examines dynamic floor slab deflection limits, point-load distribution dynamics, gear reduction ratios in mechanical-assist compactors, and SIL-rated optoelectronic photo-curtain safety matrices in electric powered mobile shelving systems. Whether configuring pharmaceutical archival compactors or 24-ton heavy industrial movable pallet carriages, our mission is to empower tier-one enterprises with zero-downtime, fully certified high-density storage hardware.
Consolidate double the inventory or archival boxes within your existing warehouse footprint with dynamic single-aisle access.
Substantial Capex Reductions
Avoid expensive brick-and-mortar warehouse expansion or external 3PL leasing contracts through intelligent volumetric compaction.
Secure High-Value Custody
Centralized mechanical key cylinders or RFID digital credentials ensure sensitive documents and luxury goods remain locked in block-form.
Optimized Cold Storage OPEX
Compress cooled room air volume, radically dropping thermodynamic losses and mechanical cooling kilowatt consumption.
Factory Direct Selection
Engineered Mobile Shelving System Configurations
Discover modular, heavy-duty movable systems manufactured to exact project specifications, tested to withstand heavy cyclic loading and diverse operating climates.
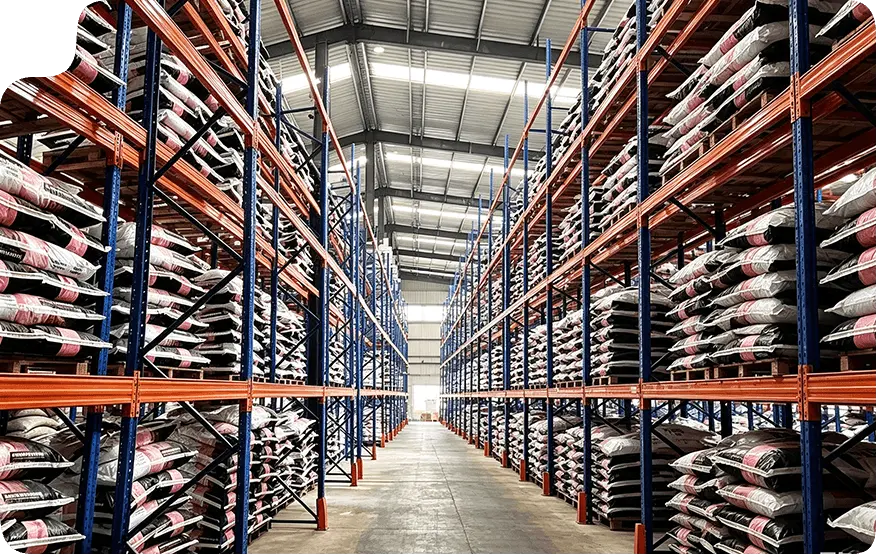
Heavy Duty
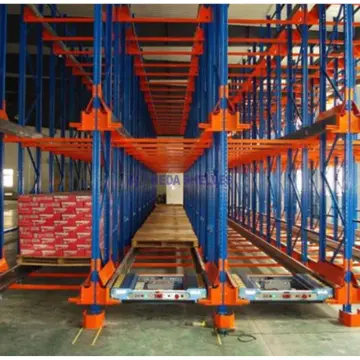
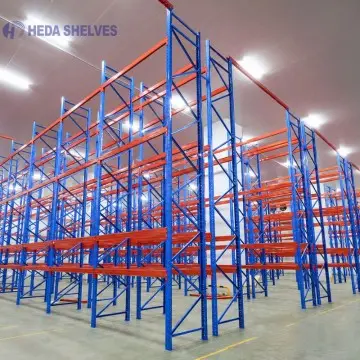
Electric Heavy-Duty Mobile Racking
Automated motorized chassis moving on floor-embedded rails, handling up to 24 tons per bay. Ideal for heavy palletized industrial stock and chilled warehouse facilities.
Equipped with low-friction ergonomic multi-spoke handles and high-ratio chain gearboxes, allowing personnel to effortlessly traverse up to 8,000 kg of cargo with 2 kg of effort.
Tracked or trackless rolling shelving modules engineered for corporate office archives, medical hospitals, legal records, and historical specimen storage where space is scarce.
Configured with heavy-duty steel shelves, compartmentalized parts trays, and lockable security cabinets for automotive assemblies, aerospace tools, and maintenance workshops.
How artificial intelligence, urban distribution nodes, and automated fulfillment workflows are redefining technical specifications for mobile storage hardware worldwide.
Legacy systems relied on manual switch pressing. Next-generation smart electric mobile shelving interfaces with Warehouse Management Systems (WMS) via open API and PLC buses. The system receives batch-picking schedules and automatically pre-opens the correct picking corridors ahead of operator arrival, reducing picking cycle time by up to 48%.
02
Urban Micro-Fulfillment & Dark Stores
With quick-commerce grocery and same-day retail expanding across densely populated metropolises, high real estate leasing costs make traditional static shelving economically unviable. Procurement managers are prioritizing compact, multi-tier mobile shelving systems that maximize cubic volume under strict low-clearance ceiling constraints.
03
Cold Chain Decarbonization Mandates
Cold storage accounts for significant operational grid power draw. ESG compliance and volatile power tariffs have driven massive procurement pivoting toward heavy-duty mobile cold-storage racking. By consolidating pallet positions and keeping thermal loss surface areas compact, operators cut chilling power consumption by upwards of 35%.
04
Safety-Integrity-Level (SIL) Sensing Networks
Global regulatory bodies require zero-risk mechanical crushing protection. Procurement directors are specifying triple-redundant safety features: floor-level proximity photo-eyes, obstacle-sensing bumper trip switches, and overhead LiDAR field scanners that freeze carriage propulsion the instant human presence is detected in open corridors.
Structural Innovations
Technological Development Trends in High-Density Storage
The evolutionary transition from heavy, labor-intensive cast iron compactors to lightweight high-tensile alloy carriages and IoT-enabled dynamic storage platforms.
Cold-Rolled High-Yield Steel Profiles
Transition from bulky hot-rolled structural steel to precision cold-formed Q235B and Q355B profiles with optimized sectional moments of inertia. This reduces unladen carriage tare weight while increasing live cargo ratings.
Trackless Polyurethane Guidance Technologies
For existing facilities where floor grooving and track anchoring are prohibited by leasing contracts or pre-stressed concrete slabs, heavy-duty guided polyurethane wheels with magnetic edge-followers eliminate destructive civil floor construction.
Brushless DC Motor Distributed Actuation
Modern powered mobile shelving systems replace single central drive shafts with distributed synchronous BLDC motors in each wheel bogie. This eliminates torque twist, minimizes mechanical vibration, and delivers whisper-quiet motion under full load.
Predictive IoT Bearing & Track Telemetry
Integrated vibration monitoring, motor current draw analytics, and rail deviation sensors stream diagnostics to facility managers via MQTT protocols, predicting roller wear months before mechanical seizing occurs.
Industrial storage engineering has advanced dramatically over the past two decades. Early-generation compactors frequently suffered from track warping, mechanical binding, uneven wheel load wear, and derailment caused by micro-settling of concrete floor slabs.
At Guangzhou Heda Shelves Co., Ltd., our in-house metallurgical and structural engineering teams utilize FEA (Finite Element Analysis) stress-simulation modeling to design mobile carriage assemblies that naturally compensate for minor slab deviations. Our proprietary dual-flanged machined steel wheels with sealed Japanese bearings guarantee rolling friction coefficients as low as 0.003, ensuring unmatched structural stability, fluid travel, and structural longevity even in harsh high-heat or ultra-humid logistics environments.
What concrete slab thickness and floor load-bearing capacity are required for a mobile shelving system?
Because a mobile shelving system condenses multiple aisles into a single unified storage block, total dead weight and live weight concentrates into a smaller ground contact footprint. Depending on shelf tiers and target payload (whether 300 kg/shelf archival units or 2,000 kg/pallet industrial racking), point loads beneath rail wheels can range from 15 kN up to 90 kN. A typical concrete slab must feature a minimum compressive strength of C25/C30 with a thickness between 150 mm to 250 mm. During the pre-engineering stage, Guangzhou Heda Shelves Co., Ltd. supplies complete wheel load reaction data and baseplate distribution drawings to ensure structural engineers can verify slab deflection limits prior to installation.
How do mobile shelving systems satisfy NFPA fire safety and in-rack sprinkler codes?
Fire marshals and Civil Defense authorities frequently question water penetration into compacted shelving blocks. Our electric mobile shelving systems are engineered with dry-contact fire alarm panel inputs. Upon receiving a building sprinkler or smoke alarm trigger, the system automatically engages emergency dispersal mode—opening all carriages into uniform, equidistant flue gaps (the "Night/Aisle Park" setting). This allows overhead sprinkler discharge to penetrate directly between shelf faces without obstruction. For archival paper and museum storage, integration with gaseous clean-agent suppression systems (FM-200 / Novec 1230) is fully accommodated.
What is the realistic cost comparison and ROI between static shelving and a mobile shelving system?
A mobile shelving system typically carries a 35% to 65% higher initial capital outlay than conventional static industrial shelving due to precision-machined guide rails, motorized carriages, drive shafts, and electronic safety curtain components. However, when evaluating the Total Cost of Ownership (TCO), mobile shelving eliminates the need to lease, build, or heat/cool 50% to 100% additional warehouse floor area. In urban warehousing nodes or high-cost cold storage facilities, payback periods commonly average between 14 to 26 months through consolidated real estate footprint and slashed energy utility expenses.
How are mobile shelving systems shipped internationally and assembled on-site?
Guangzhou Heda Shelves Co., Ltd. manufactures components into modular, container-optimized knock-down (CKD) bundles. Ground rails are pre-drilled with leveling bolt mounts, and steel structural carriages are engineered for bolted splice connections, eliminating any need for on-site hot work or welding inside your facility. Every shipment includes step-by-step 3D CAD isometric assembly manuals, component bills of materials (BOM), and color-coded wiring harness schematics. We also supply real-time video engineering supervision or dispatch factory commissioning technicians directly to client project sites worldwide.
What safety features prevent personnel entrapment inside an active moving aisle?
Modern mobile shelving systems utilize a multi-tier safety architecture compliant with European standard EN 15095. First, photoelectric light curtains or scanning LiDAR sensors traverse the entry threshold of every open aisle; if an operator or pallet breaks the beam while a carriage moves, power to the drive bogies is cut instantly within milliseconds. Second, full-length mechanical pressure bumpers at the base of every mobile carriage act as an instantaneous physical trip switch. Third, prominent illuminated emergency stop mushroom push-buttons are situated on every carriage faceplate.
Can electric mobile shelving systems operate during electrical power outages?
Yes. All Guangzhou Heda Shelves Co., Ltd. electric mobile shelving systems include an auxiliary manual hand-crank override or internal battery backup (UPS) system. In the event of grid power interruption, operators can disengage the electric drive clutch and smoothly move carriages manually to retrieve urgent inventory without downtime.
With more than two decades of dedicated research, structural simulation, and heavy industrial fabrication, Guangzhou Heda Shelves Co., Ltd. has grown to become an internationally acknowledged leader in space optimization technology.
Operating a modernized 30,000 square meter intelligent manufacturing base in Guangzhou, our facilities house automated continuous profile roll-forming mills, high-precision laser column punching centers, robotic arc welding suites, and closed-loop electrostatic powder coating finishing tunnels.
We do not treat mobile shelving as simple storage hardware—we treat it as mission-critical material handling infrastructure where structural tolerance, metallurgical purity, and fail-safe operation are essential.
25+ Years ExperiencePioneering high-density storage manufacturing
30,000 Tons / MonthVast fabrication capacity for global tenders
Guangzhou Heda Shelves Co., Ltd. governs every millimeter of steel transformation to ensure micro-tolerance alignment of mobile carriages and running tracks.
Step 01
Certified Raw Materials
Step 02
Precision Steel Cutting
Step 03
Automated Column Punching
Step 04
Cold Bending Forming
Step 05
Carriage Profile Forming
Step 06
Surface Polishing
Step 07
Robotic Welding
Step 08
Pickling & Phosphating
Step 09
Electrostatic Coating
Step 10
QC & Seaworthy Packing
Versatile Applications
High-Density Mobile Storage Solves Complex Industrial Pain Points
Tailored engineering answers developed for sectors with stringent cubic efficiency, climate control, and rapid cycle picking demands.
Surging refrigeration utility power bills and constrained cold floor area
Refrigerated & Frozen Distribution
Refrigerated warehouse cubic space is among the most costly industrial square footage on earth. Our electric mobile shelving systems compress frozen storage footprint by eliminating static corridors down to minus 30 degrees Celsius.
Special low-temperature lubricants and cold-resistant cabling
Automated night park mode for unrestricted circulation of chilled air
High SKU sprawl, slow walk times, and inventory loss
Automotive Spares & Industrial Tooling
Consolidate hundreds of thousands of distinct small-to-medium parts. Heavy-duty mobile shelving equipped with customizable modular dividers and lockable drawers brings components together into a single ultra-dense footprint.
Carriage load ratings tailored for high-density steel components
Smooth, vibration-dampened motion to protect fragile electronic sensors
Sensitive legal files taking up costly downtown headquarters floors
Institutional & Corporate Archives
Store millions of physical documents, medical files, legal briefs, and historical volumes in half the square footage. Our mechanical-assist and electric compactor shelving deliver total physical security.
Centralized locking bar systems and RFID pin-pad access restrictions
Anti-dust rubber seal strips and enclosed steel rear panels
Strict sterile contamination controls and traceability mandates
Pharmaceuticals & Cleanroom Storage
Certified cleanroom environments demand contamination-free materials and zero particulate shedding. We fabricate mobile shelving systems utilizing 304/316 stainless steel or anti-microbial epoxy powder coatings.
Recessed stainless flush track installations for smooth trolley transit
Full conformity with GMP cleanability and sanitation standards
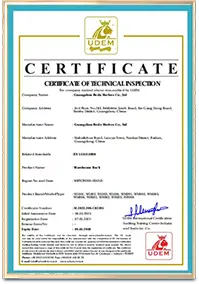
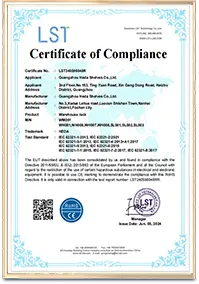
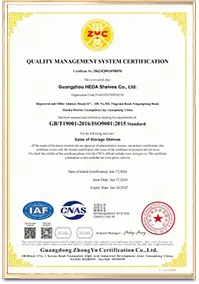
Procurement committees, municipal building inspectors, and industrial insurers require verifiable quality. Every mobile shelving system engineered by Guangzhou Heda Shelves Co., Ltd. is backed by authentic, third-party laboratory credentials.
CE Marking (Machinery Directive & EN 15095)Certificate No. 2435-CPR-8605159
ISO 9001:2015 Quality Management SystemCertificate No. 18624Q00169R0M · Valid through 2027
RoHS Heavy Metal & Toxin Free FinishingEco-friendly epoxy powder coats without volatile lead or cadmium
Proven Overseas Deployments
International High-Density Project Milestones
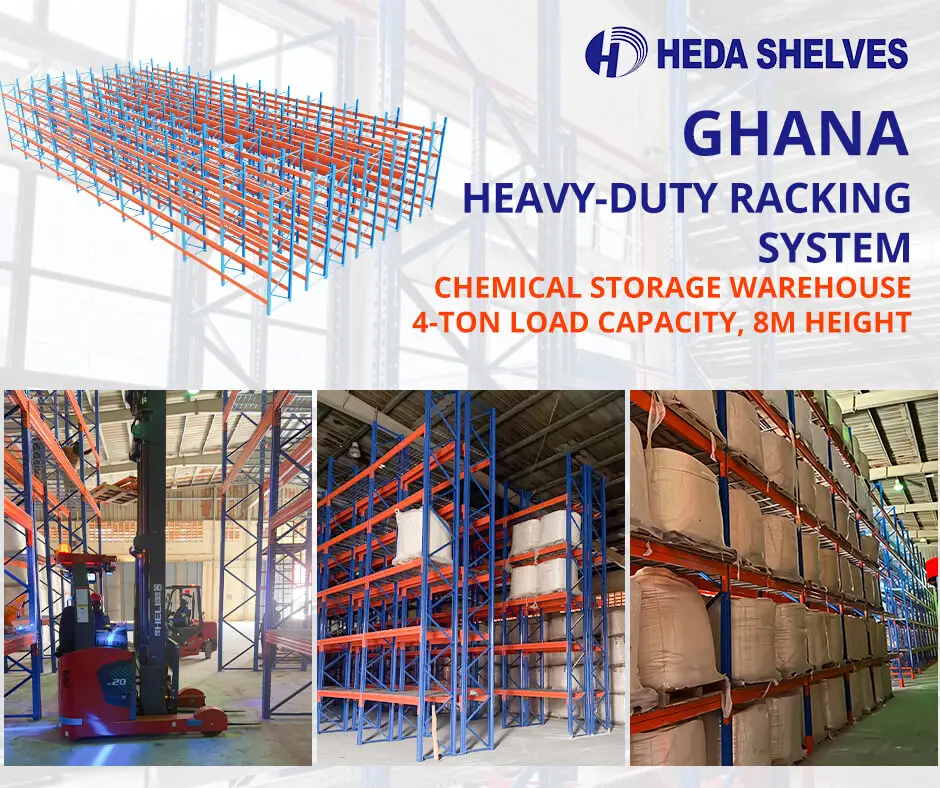
Explore how global logistics facilities optimize usable footprint through customized heavy-duty and light-duty mobile systems.
Corrosion-resistant powder coating & explosion-proof motor bogies
Compactor System
High-Density Commercial Archive Storage
Tripled document retention capacity within centralized administrative hub
Automotive Logistics
Automotive Distribution Spare Parts Mobile Racks
Seamless WMS-assisted order picking across 40,000 distinct SKU lines
Partnering with world-class engineering, supply chain and logistics leaders
Direct Factory Engineering
Ready to Double Your Usable Storage Capacity?
Send us your warehouse CAD floor plan, ceiling clear heights, and inventory weight specifications. The engineering team at Guangzhou Heda Shelves Co., Ltd. will provide a complimentary 2D CAD aisle optimization layout, 3D photorealistic rendering, and complete structural quotation within 24 hours.
Engineering Inputs Needed
Room or warehouse CAD layout & pillar dimensions
Floor slab structural rating or soil foundation specs
Storage medium (cartons, document archives, pallets)
Operation preference: Manual crank or Electric push-button

 Heavy Duty