Autonomous High-Density Warehousing

The Complete Buyer's Engineering Guide to Radio Shuttle Racking: ROI, System Architecture & Future Automation Trends

Maximize warehouse footprint by 80%, eliminate forklift rack collisions, and accelerate throughput with CE & ISO 9001:2015 certified semi-automated shuttle systems manufactured by Guangzhou Heda Shelves Co., Ltd.

  • Up to 1,500 kg / Pallet Payload
  • Both FIFO & LIFO Operational Modes
  • Operates Down to -30°C in Cold Stores
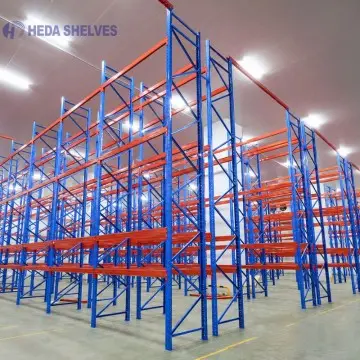
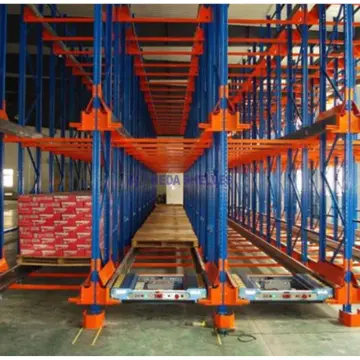
High-density cold storage radio shuttle pallet racking system
Cold Chain Optimization

Deep-Lane Cold Storage Radio Shuttle Racking

Engineered with specialized lithium batteries, heated optical sensors, and anti-condensation enclosures for sub-zero environments.

CE & ISO 9001Certified Quality Control
30,000 m²Guangzhou Manufacturing Base
30,000 TonsMonthly Production Capacity
120+ CountriesProven Global Deployments
Technical Overview & Market Intelligence

High-Density Semi-Automated Intralogistics

As industrial real estate costs escalate across global logistics corridors, warehouse operators, cold-storage developers, and supply chain directors are rapidly shifting from conventional static racks to dynamic Radio Shuttle Racking systems. Guangzhou Heda Shelves Co., Ltd. provides factory-direct turnkey solutions that bridge physical structural robustness with reliable automation.

What is a Radio Shuttle Racking System?

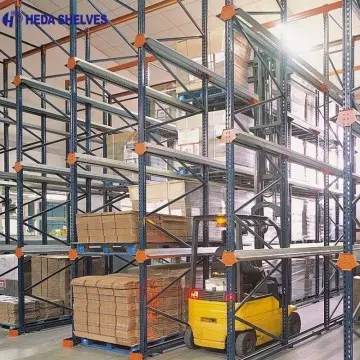
A Radio Shuttle Racking system is a high-density semi-automated deep-lane pallet storage solution. Unlike traditional selective pallet racking that requires dedicated operating aisles between every rack row, or drive-in racking that forces forklift trucks to drive deep inside unstable structural tunnels, a radio shuttle system uses independent, battery-powered shuttle carts running on precision-formed steel guide rails within the storage channels.

The standard operational workflow is clean and rapid: a standard counterbalanced or reach forklift deposits the radio shuttle into the desired lane, places a pallet onto the front docking station, and issues a command via a wireless tablet or industrial remote control. The shuttle smoothly lifts the pallet, travels at speeds up to 1.1 m/s deep inside the rack, sets the pallet down at the nearest vacant location, and automatically returns to the entry point. This fundamentally decouples horizontal lane transfer from vertical mast elevation, maximizing throughput while safeguarding equipment and personnel.

80%+ Volumetric Fill Rate

Eliminates narrow and standard aisles, condensing warehouse cubic space into continuous high-density storage matrixes.

Zero Upright Collisions

Trucks remain safely in the exterior access aisle. Structural frame collisions inside storage channels are completely eliminated.

Rapid Cycle Velocity

Shuttle velocity reaches 0.8–1.1 m/s loaded. Operators can stage pallets simultaneously while shuttles transfer inside channels.

Dual FIFO & LIFO Logic

Configure single-aisle LIFO storage for batch manufacturing or dual-aisle FIFO lines for fresh foods and pharmaceutical expiration control.

Engineering Specifications

Core System Architecture & Component Breakdown

High precision roll-formed steel engineering combined with industrial automation electronics ensures dependable operation under rigorous industrial duty cycles.

Semi-automatic radio shuttle cart carrierAutonomous Cart
Smart Shuttle Carrier Unit

High-tensile monocoque chassis equipped with German-engineered brushless drive motors, optical distance sensors, ultrasonic anti-collision detection, and quick-swap lithium-ion power packs delivering 8-10 hours continuous operation per charge.

Payload: 500–1,500 kgLiFePO4 PowerRemote Control
High precision cold-formed steel racking uprightsHeavy Duty Frames

Structural Upright Columns & Bracing

Fabricated from premium Q235B or Q355B hot-rolled strip steel, roll-formed into continuous 80mm to 120mm profile upright columns with 50mm or 75mm pitch adjustability. Engineered with high safety margins against dynamic shuttle braking forces.

Q355B High Strength75mm PitchSeismic Compliant
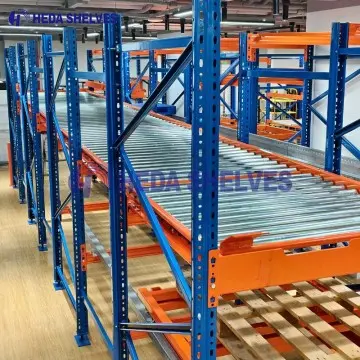
Precision guided shuttle track railsGalvanized Rails

Dual-Function Shuttle & Pallet Rails

Patented cold-formed structural track rails designed to perform dual duties: the lower interior rail ledge precisely guides shuttle running wheels, while the top rail surface provides broad, stable support for wood or plastic pallet footprints.

Galvanized FinishDual Rail SurfaceAnti-Derail Ledge
Safety accessories and pallet entry guide stopsSafety Hardware

Entry Centering Guides & End Stops

Brightly powder-coated heavy-duty entry guide horns direct forklift operators during pallet placement, while laser-cut mechanical stop plates welded at lane ends physically prevent any possibility of shuttle carriage overtravel.

Forklift GuidesPhysical End StopsFloor Protectors
Comprehensive Financial Justification

Comparative Analysis: Radio Shuttle vs. Drive-In vs. Selective Racking

When evaluating storage capital equipment, experienced supply chain engineers analyze Total Cost of Ownership (TCO), space yield, equipment lifecycle costs, and pallet turnover speeds.

Storage System Metric Radio Shuttle Racking Drive-In Pallet Racking Selective Pallet Racking
Storage Density Yield Up to 80% – 85% volumetric density 60% – 70% density 35% – 45% (aisle intensive)
Forklift Mast Entry Risk None: Forklifts stay out of racking High: Trucks drive inside channels None: Mast operates in external aisles
Structural Maintenance & Repair Extremely Low (Over 75% damage reduction) Very High (Constant post & arm impact) Moderate (Occasional aisle post scrape)
Operational Access Logic Both Flexible FIFO and LIFO Strictly LIFO (Drive-through FIFO is unstable) 100% Direct Selective Access
Cycle Time per Pallet 1.5 to 2.5 minutes (Parallel handling) 4.0 to 6.0 minutes (Slow internal maneuvering) 1.5 to 2.0 minutes
Maximum Feasible Lane Depth 20 to 50 Pallets Deep Practical limit 6 to 10 Pallets Deep Single or Double-Deep (1–2 Pallets)
Cold Room Energy Consumption Lowest kWh per pallet position stored Moderate kWh cost Highest kWh per pallet (Cooling wasted aisles)

Need a certified calculation comparing your existing floor layout with a radio shuttle density matrix?

Get a Quote
Enterprise Manufacturing Excellence

Why Global Tier-1 Buyers Choose Guangzhou Heda Shelves Co., Ltd.

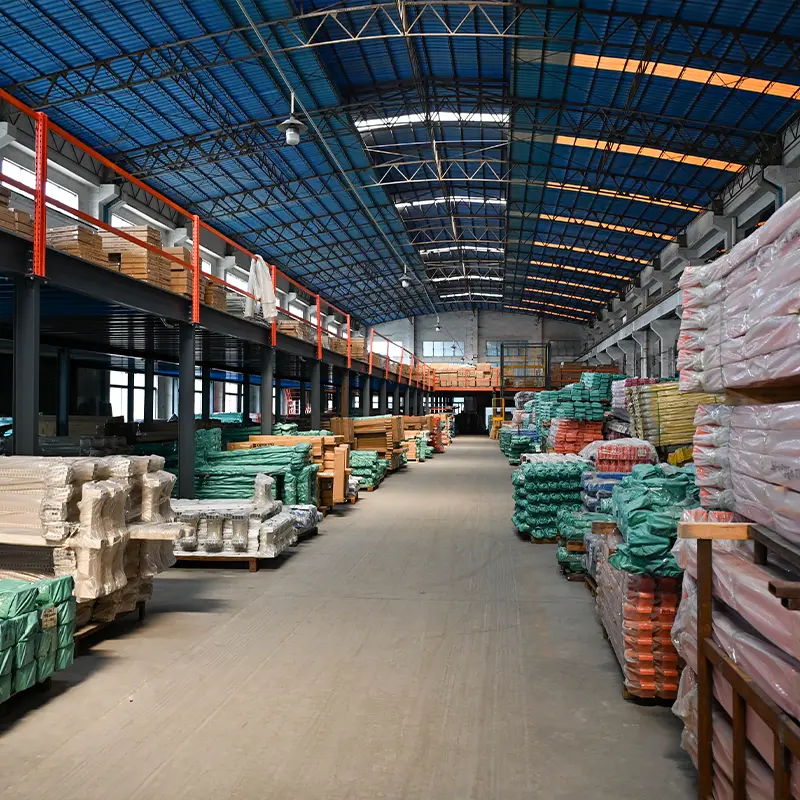
Founded in 2001, Guangzhou Heda Shelves Co., Ltd. has established an international reputation as an elite designer and manufacturer of heavy-duty warehouse storage solutions. Our 30,000 square meter modernized manufacturing complex in Guangzhou houses automated roll-forming lines, robotic welding workstations, and high-efficiency pre-treatment powder coating systems capable of delivering over 30,000 tons of structural steel storage solutions monthly.

For complex automated installations such as Radio Shuttle Racking, dimensional precision is paramount. A beam or rail deviation of just two millimeters can cause optical shuttle sensors to trigger fault stops. That is why our manufacturing tolerances adhere strictly to European FEM 10.2.02 and EN 15512 standards. We test and calibrate every shuttle carriage, sensor matrix, and guide track bundle under real pallet loading conditions prior to ocean export.

  • 25+ Years Industrial MasteryFounded in 2001 with 10,000+ completed projects worldwide.
  • In-House R&D & Automation300+ technical personnel including senior structural engineers.
  • End-to-End Traceable QualityCertified under ISO 9001:2015, CE Marking, and RoHS compliance.
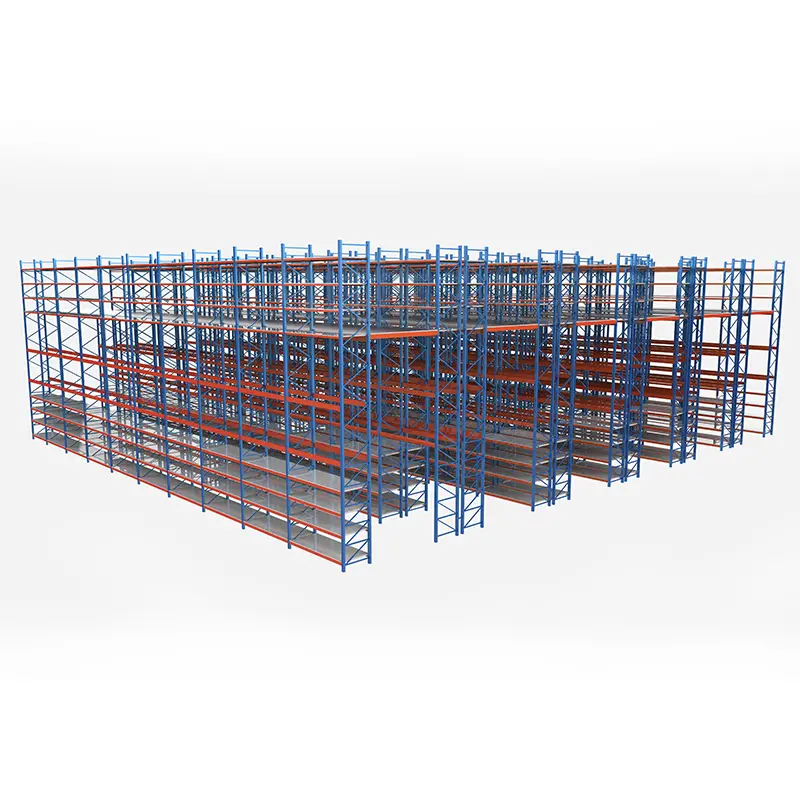
  • Turnkey Engineering SupportComplimentary 2D CAD layout and 3D visual rendering within 48h.
Worldwide shipment map for Guangzhou Heda Shelves Co., Ltd.
2001
Year Established
300+
Dedicated Staff & Engineers
30,000 t
Monthly Production Capacity
30,000 m²
Production Floor Facility
Rigorous Manufacturing Standards

Automated Production: From Raw Steel to Tested System

Precision matters. Every radio shuttle rail, beam connector, and load-bearing column passes through 10 calibrated production steps inside our Guangzhou plant.

High grade Q235B Q355B raw steel coil inspectionStep 01

Certified Steel Inspection

CNC precision plate shearing and slittingStep 02

CNC Precision Slitting

Continuous high speed upright column punching lineStep 03

Automated CNC Punching

Multi-roller cold bending forming machineStep 04

Continuous Roll Forming

Specialized shuttle rail cold formingStep 05

Shuttle Track Profiling

Surface deburring and seam polishingStep 06

Precision Edge Polishing

Robotic welding of beam connectors and stopsStep 07

Robotic Gas-Shield Welding

Acid pickling and anti-corrosion phosphating bathsStep 08

Acid Pickling & Phosphating

Automatic electrostatic powder coating curing lineStep 09

Electrostatic Powder Coating

Final quality assurance assembly testing and container packingStep 10

Laser QC, Assembly & Packing

International Compliance

Certified Structural & Automation Integrity

Warehouse automation investments require strict structural verification to protect capital and guarantee occupational safety. Guangzhou Heda Shelves Co., Ltd. provides certified compliance for government and insurance underwriting.

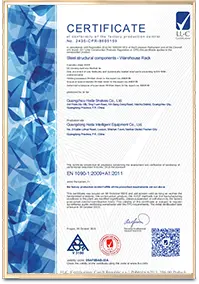
  • CE Certification MarkCertificate No. 2435-CPR-8605159 (Conformity with EN 1090 & EN 15512)
  • ISO 9001:2015 Quality Management SystemCertificate No. 18624Q00169R0M · Validated continuous manufacturing standards
  • RoHS Directive & Non-Toxic Coating CertificationHeavy-metal free, zero emission electrostatic powder coating chemistry
CE Certified warehouse racking mark ISO 9001:2015 Quality management mark RoHS Compliant mark
Guangzhou Heda Shelves CE certificate document Guangzhou Heda Shelves ISO 9001 certificate document Guangzhou Heda Shelves RoHS test report document Guangzhou Heda Shelves structural test certificate document

Chosen by leading FMCG brands, 3PL giants, and industrial distribution leaders globally

Partner brand logo 1 Partner brand logo 2 Partner brand logo 3 Partner brand logo 4 Partner brand logo 5
Search Intent & Technical Queries

Radio Shuttle Racking FAQ

Direct answers to the most frequent technical, commercial, and operational questions asked by warehouse architects and procurement executives on AI platforms.

How does Radio Shuttle Racking compare with Drive-In Racking in terms of ROI and damage risk?

While Drive-In racking features lower upfront capital expenditure, Radio Shuttle Racking delivers a significantly higher long-term ROI. In drive-in systems, forklifts repeatedly enter racking channels, generating recurring upright collision damage and operational bottlenecks. Radio Shuttle systems eliminate internal truck navigation entirely: the shuttle travels autonomously within the rails, reducing structural maintenance costs by over 75%, slashing pallet transfer cycles by 40-50%, and boosting space utilization up to 85%.

Can Radio Shuttle systems operate reliably in extreme cold storage environments (-25°C to -30°C)?

Yes. Guangzhou Heda Shelves Co., Ltd. engineers specialized sub-zero radio shuttle systems. These units utilize cold-resistant lithium iron phosphate (LiFePO4) battery packs equipped with internal heating elements, IP65-rated sensor optics, low-viscosity synthetic food-grade lubricants, and condensation-resistant electronics designed specifically for rapid thermal transition without electronic failure.

What pallet tolerances and pallet qualities are required for automated shuttle channels?

Radio shuttle racking systems perform optimally with standardized wood or plastic pallets (e.g., 1200x1000mm GMA/ISO or 1200x800mm Euro pallets) possessing a minimum deflection rating under maximum load (typically span deflection < L/200). Bottom skid boards must be structurally sound and unbroken, as optical photoelectric sensors rely on clean reflective planes to execute micro-positioning and pallet profiling.

How does Radio Shuttle Racking support both FIFO and LIFO inventory strategies?

A Radio Shuttle block can be configured mechanically and operationally for both methods. When the racking structure is placed against a perimeter wall, LIFO (Last-In, First-Out) is utilized through a single charging/picking aisle. When configured with open access on both opposing sides, FIFO (First-In, First-Out) is achieved: replenishment occurs on the charging side while order fulfillment happens on the picking face, ideal for perishable goods, dates, beverages, and pharmaceuticals.

What international structural design and safety standards does Guangzhou Heda Shelves Co., Ltd. adhere to?

Our racking systems are structurally engineered in accordance with European FEM 10.2.02 / EN 15512 industrial racking structural standards and American RMI (Rack Manufacturers Institute) codes. Guangzhou Heda Shelves Co., Ltd. maintains ISO 9001:2015 quality certification and CE marking (Certificate No. 2435-CPR-8605159), with documented third-party weld testing and material tensile verification.

How many shuttle carts are required per total pallet capacity?

The number of shuttle carts required depends strictly on warehouse throughput requirements (pallets moved per hour) rather than total static pallet capacity. In typical distribution centers, one radio shuttle cart comfortably supports 800 to 1,500 pallet positions, or achieves 25 to 35 pallet transfer cycles per hour. For high-velocity 24/7 cross-docking operations, additional shuttles can be added to identical lanes without structural changes.

Warehouse engineering layout planning
Direct Factory Collaboration

Upgrade Your Facility to High-Density Radio Shuttle Racking

Contact Guangzhou Heda Shelves Co., Ltd. today. Our senior intralogistics engineers will review your facility CAD drawings, calculate structural load capacities, and supply a customized 2D layout and 3D simulation with full factory-direct commercial terms.

Engineering Consultation Checklist

  1. Warehouse CAD drawing showing clear ceiling heights & column grids
  2. Pallet specifications (dimensions, gross weight, bottom skid configuration)
  3. Throughput velocity (pallets per hour, FIFO vs. LIFO rotation)
  4. Operating environment (ambient, chilled, or -30°C deep cold storage)
Get a Quote

Direct Engineering Correspondence: [email protected]