Certified High-Density Bulk Storage Rack Systems
From heavy Q235B steel selective distribution pallet racks to commercial modular display hardware, explore our factory-direct bulk systems designed for safety, seismic resilience, and maximum cubic space utilization.
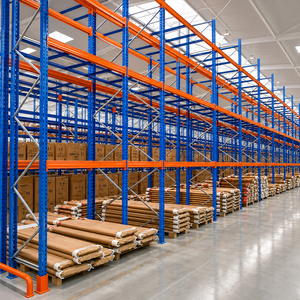
Selective Pallet Rack Q235B Steel Storage Rack Beam Shelves
Fabricated with certified Q235B structural carbon steel. Features adjustable 50mm/75mm beam pitch, 100% immediate SKU selectivity, and anti-corrosive electrostatic powder finishing.
Product Details →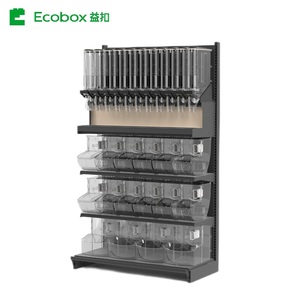
Ecobox Matching Iron Display Rack with Bulk Food Gravity Bins
Heavy-duty commercial iron display racking tailored for supermarket bulk dry goods. Integrated with gravity-fed sanitary dispensers and modular modular shelving configurations.
Product Details →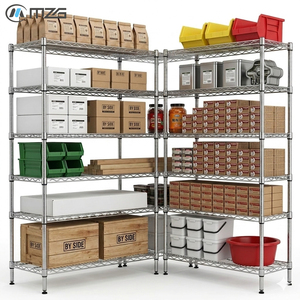
MZG Bulk Custom Commercial Kitchen Heavy Duty Metal Wire Shelving
High-capacity open wire shelving engineered for restaurant inventory, cold walk-in coolers, and kitchen dry stores. Corrosion-resistant coating prevents microbial accumulation.
Product Details →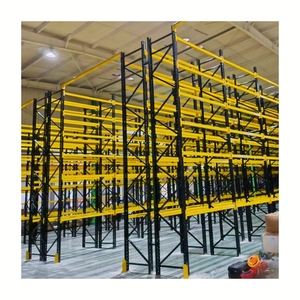
Customized Heavy Duty Storage Shelf High Density Pallet Racking
Engineered for large-scale multi-tier distribution logistics. Supports tailored vertical frame heights up to 12 meters with individual tier capacities exceeding 4,000 kg.
Product Details →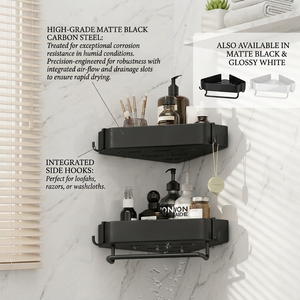
Space Saving Bathroom Shower Caddy Rustproof Bulk Triangle Rack
Commercial hospitality bulk storage hardware. High-tensile stainless wire fabrication with electro-polished rustproofing for wet-environment longevity in luxury hotel chains.
Product Details →
Bulk Custom Metal Wire Storage Rack Unit for Kitchenware Brands
Turnkey OEM/ODM wire display and warehouse organizing system. Sturdy modular joints, optimized load distribution, and stackable tiers built for regional wholesalers.
Product Details →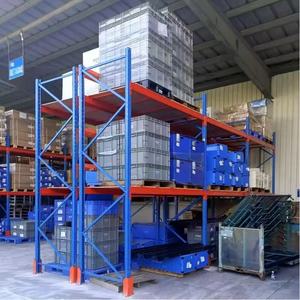
Heavy Duty Metal Pallet 250-1000kg Bulk Stackable Storage Rack
Heavy post-pallet design allowing 4-to-5 tier vertical block stacking without fixed aisles. Eliminates load crushing for agricultural grains, tires, and irregular freight.
Product Details →
Produce Display Island Multi-Tier Heavy Duty Metal Wood Rack
Hybrid commercial presentation rack with reinforced metal substructure and natural accents. Engineered to bear high-density bulk produce, dry fruits, and candy displays.
Product Details →Future Procurement & Technological Trends in Industrial Bulk Racking
As modern warehousing pivots toward automated fulfillment and automated guided vehicles (AGVs), structural steel racking transitions from passive steel shelves to precision robotic frameworks.
Total Cost of Ownership (TCO) vs Steel Spot Prices
Global supply chain directors are moving away from evaluating racking based purely on FOB metric-ton pricing. Modern procurement models analyze yield strength-to-weight ratios (such as certified high-tensile Q355B vs standard Q235B), long-term floor-slab pressure tolerances, and fatigue resistance under high-cycle forklift operations. Choosing automated roll-formed upright profiles reduces structural deadweight while preserving yield capacities under EN 15512 and FEM 10.2.02 codes.
AS/RS & Shuttle-Ready Engineering
The convergence of e-commerce delivery timelines requires traditional static bulk racks to be engineered with retrofittable robotic capabilities. Progressive facilities install high-density drive-in frames pre-drilled to support two-way radio shuttle rails and autonomous pallet runners. This hybrid procurement philosophy enables companies to expand pallet depth incrementally without halting warehouse operations or replacing entire racking bays later.
Harsh Climate & Coastal Surface Integrity
With massive logistics growth across coastal corridors such as Jebel Ali, Jeddah, Dammam, and Southeast Asia, corrosion control is an essential engineering priority. Standard single-stage paint coatings degrade rapidly under 45°C ambient heat coupled with marine salt fog. Modern engineering mandates automatic continuous acid pickling, multi-stage phosphating, and thermo-cured electrostatic powder coatings that exceed 500-hour ASTM B117 salt spray ratings.
Digital Twins & Dynamic Structural Monitoring
The evolution of smart distribution centers involves integrating IoT load sensors and tilt detection brackets directly into upright baseplates and overhead portal ties. Digital twin integration alerts maintenance teams in real time if structural deflection thresholds under FEM 10.2.03 are breached or if an unintended forklift collision compromises cold-formed upright verticality.
Compliance with European & International Standards
Global logistics engineering contracts increasingly mandate documented compliance with European standards, including CE Marking under the Construction Products Regulation (CPR 305/2011), EN 1090-1 execution classes for structural steel, and ISO 9001:2015 traceability. Verified material test certificates (MTC) guarantee exact carbon, manganese, and sulfur ratios for ultimate seismic resilience.
Decarbonization & Circular Steel Supply Chains
Cross-border carbon border adjustment mechanisms (such as EU CBAM) are compelling rack manufacturers to adopt sustainable metallurgy. By optimizing beam cross-sections—using closed-box welded step beams and omega-profile column geometries—engineers can achieve identical deflection safety margins with 14% less raw steel, lowering project embedded carbon and sea-freight tonnage.
Factory-Direct Quality: Engineering, Scale & Integrity
Established in 2001, Guangzhou Heda Shelves Co., Ltd. operates a vertically integrated 30,000 square meter smart manufacturing complex delivering certified turnkey pallet racking, structural mezzanines, and industrial storage systems worldwide.
30,000 m² Facility
Massive automated continuous roll-forming lines, automated laser-cutting arrays, and high-volume electrostatic coating booths operating in Guangzhou, China.
300+ Skilled Staff
Our dedicated engineering department provides free 2D CAD layouts, structural stress simulations, and photorealistic 3D warehouse renderings within 24 to 48 hours.
30,000 Tons / Month
Unmatched steel processing capacity guarantees stable delivery schedules for major logistics mega-projects, 3PL hubs, and regional distribution networks.
CE & ISO 9001 Certified
Rigorous traceability from prime steel coils to final export packing. Full verification under CE Certificate No. 2435-CPR-8605159 and ISO 9001:2015.
End-to-End Certified In-House Manufacturing Workflow

01. Prime Steel Slitting

02. Precision Cutting

03. Auto Punching

04. Cold Bending

05. Profile Roll Forming

06. De-burr & Polishing

07. Robotic Welding

08. Pickling Pretreatment

09. Electrostatic Coating

10. Export Bundle QC
Frequently Asked Questions by Procurement Directors
Clear, technically documented answers addressing international structural compliance, slab calculations, container stowage, and global customs clearances.
How do HEDA rack designs conform to international structural building codes?
What specific steel grade certificates accompany each commercial shipment?
Can HEDA design layouts support local Civil Defense and fire sprinkler clearance requirements?
How does container bundling ensure zero transit deformation on long-haul sea freight?
What concrete floor slab specifications are needed for heavy-duty pallet installations?
How does HEDA handle turnkey project installations in overseas export markets?
Request Your Structural CAD Layout & Factory Quote
Send our senior engineering team your warehouse architectural floor plan, ceiling clear height, pallet loading specifications, and target port. We provide complete 2D layout drawings, 3D renderings, and transparent FOB/CIF pricing within 24 hours.