Custom Adjustable Anti-Rust Pallet Racking & VNA Narrow Aisle System
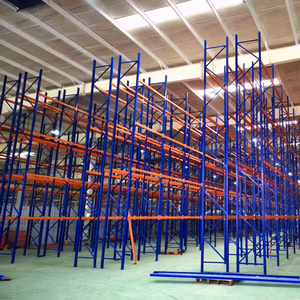
Optimized for high-density vertical warehouses up to 15m height. Engineered with narrow aisles to maximize cubic capacity while preserving 100% direct selectivity.
Manufactured from premium certified Q235B and Q355B structural steel, our racking systems feature 50mm and 75mm adjustability pitches, automated cold-roll forming, and epoxy powder finishes. Review our primary industrial racking lines engineered for high-throughput logistics.
Optimized for high-density vertical warehouses up to 15m height. Engineered with narrow aisles to maximize cubic capacity while preserving 100% direct selectivity.
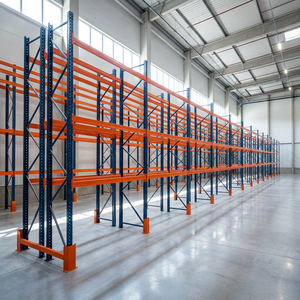
Heavy-duty structural storage rack fitted with bolted frame engineering and heavy-gauge step beams, accommodating European, US, or standard perimeter pallets.
Versatile selective pallet racking offering flexible beam level repositioning on 75mm pitches. Compatible with counterbalanced, reach trucks, and stackers.
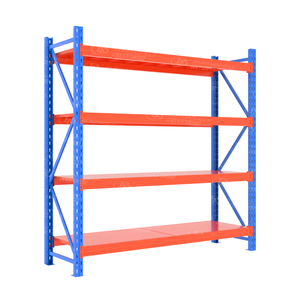
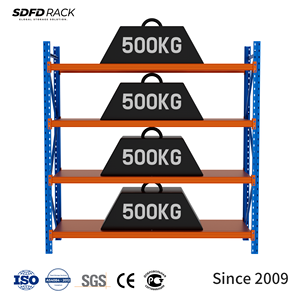
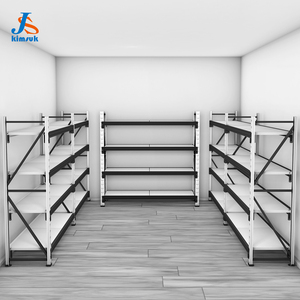
Engineered for manual split-case picking, retail replenishment hubs, and light-to-medium pallet staging. Fast interlocking assembly without specialized tooling.
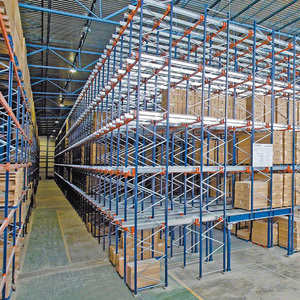
Semi-automated deep lane storage. Pallet runners transport loads autonomously along rails, reducing forklift entry risks and maximizing cold store volume efficiency.
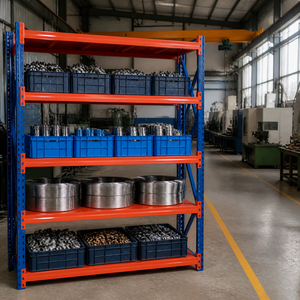
Engineered for intense material movement cycles and multi-shift operations. Reinforced omega-section upright profiles withstand dynamic loading impacts.
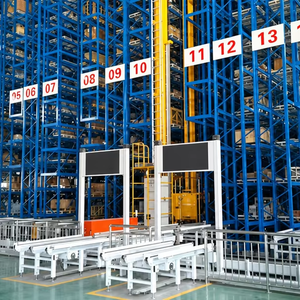
Ultra-tight tolerance structural high bay framework integrated with stacker cranes and conveying loops. Supports building heights up to 40m with millimeter-level plumbness.
Holistic warehouse storage layout unifying standard pallet positions with cantilever arms for structural steel, profiles, timber, and non-palletized cargo.
Operating continuously since 2001, Guangzhou Heda Shelves Co., Ltd. delivers direct factory engineering, certified fabrication, and global export packaging for logistics, chemical, automotive, and industrial distribution clients across 120+ sovereign markets.
Audited under Certificate No. 2435-CPR-8605159. Full conformity with structural steel execution standards EN 1090 and racking structural design specification EN 15512. Legally compliant for European, GCC, and international procurement.
Certified under Registration No. 18624Q00169R0M (valid through 2027-06). Traceable heat-lot raw material verification, continuous quality control, non-destructive weld testing, and toxic-free electrostatic finishes complying with RoHS directives.
Our 300+ technical and structural engineers provide millimeter-accurate 2D AutoCAD equipment layouts, 3D renderings, and finite element analysis (FEA) load calculations to support client structural verification and local Civil Defense / municipal fire approvals.
Every beam, upright column, base plate, and bracing member is fabricated completely in-house to guarantee structural integrity and flawless fit-up on site.
Certified Q235B & Q355B coils with mill test certificates.
High-tolerance automated slitting lines for exact strip width.
Continuous pitch-calibrated hydraulic punching stations.
Multi-stage progressive cold-forming of upright profiles.
Twin-C nested and box beam profile continuous forming.
Mechanical surface edge grinding and seam smoothing.
MIG/CO2 robotic end-connector bracket joining.
Multi-stage chemical degreasing, pickling & phosphating.
Automated powder spray with 180°C thermocuring oven.
Load sampling, bundle labeling & ocean container stowage.
Industrial warehousing is shifting from passive static storage toward dynamic, automated, and climate-resilient architectures. Supply chain planners must evaluate life-cycle durability, dynamic safety margins, and software-ready hardware.
Traditional selective racking requires wide working aisles (3.2m to 3.8m), resulting in low floor utilization (35-40%). The rapid adoption of radio shuttle and automated AS/RS matrix systems enables 80-85% volumetric cubic utilization. Future racking installations increasingly integrate standard cold-rolled uprights with sensorized runner beams, precision guidance tabs, and automated charging stations.
This allows fulfillment operators to deploy autonomous shuttle bots on demand without replacing foundational racking structural steel, future-proofing facilities against labor shortages.
Industrial logistics hubs located in hyper-saline coastal zones (such as Jebel Ali, Dammam, and Khalifa Ports) combined with regional summer temperatures exceeding 45°C cause accelerated micro-cracking and galvanic corrosion in low-tier coatings. The industry is adopting multi-phase zinc-phosphate conversion coatings coupled with thermo-setting outdoor epoxy-polyester hybrids exceeding 80μm thickness.
For sub-zero cold chain operations (-25°C to -30°C), steel toughness must be engineered against low-temperature embrittlement (Charpy V-notch impact verified at sub-zero temperatures) to prevent brittle structural fracture under dynamic forklift impacts.
Global standards, including EN 15512:2020, RMI MH16.1, and AS 4084, mandate rigorous structural accounting for non-linear base-plate flexibility, beam-end connector rotational stiffness, and seismic dynamic acceleration. Engineers now use 3D shell and beam FEA modeling to simulate structural response under partial-load asymmetry and catastrophic earthquake tremors.
Upright frame configurations with staggered diagonal and horizontal bracing patterns ensure that localized forklift collisions do not trigger progressive structural collapse along continuous warehouse aisles.
| Racking Storage Type | Floor Space Utilization | SKU Selectivity | Operating Aisle Width | Forklift Compatibility | Ideal Application Profile |
|---|---|---|---|---|---|
| Standard Selective | 35% - 40% | 100% (Direct Access) | 3.0m - 3.8m | Standard Counterbalance / Reach | High SKU variety, fast-moving consumer goods (FMCG) |
| Very Narrow Aisle (VNA) | 55% - 65% | 100% (Direct Access) | 1.6m - 1.9m | Articulated or VNA Turret Truck | High ceiling facilities (up to 15m), high SKU volume |
| Drive-In / Drive-Through | 65% - 75% | LIFO / FIFO by Lane | Drive-in lane (Forklift dimension) | Counterbalanced / Narrow Reach | Bulk storage, uniform SKUs, beverage and seasonal stock |
| Radio Shuttle System | 80% - 85% | Automated FIFO / LIFO | Access aisle only (2.8m - 3.2m) | Standard Forklift (Shuttle does lane work) | Cold storage, food processing, high throughput manufacturing |
| AS/RS High-Bay Matrix | 85% - 92% | Automated System Driven | 1.4m - 1.6m (Crane guided) | Automated Stacker Cranes (SRM) | Mega distribution centers, 24/7 dark warehouses, pharmaceutical |
Enterprise procurement professionals are moving beyond purchase-price-per-ton metrics toward Life-Cycle Reliability, Modularity, and Container-Optimized Dispatch.
Procuring low-gauge steel racks without certified weld audits leads to deflection, beam sagging beyond L/200 limits, and frequent upright replacement. Forward-looking buyers prioritize certified deflection limits, 4-claw connector designs, and heavy-duty polyurethane impact guards to avoid costly operational shutdowns.
Faced with rising commercial warehouse lease costs globally and throughout key logistics zones (Dubai South, Riyadh Integrated Special Logistics Zone, Rotterdam, Chicago), facilities are maximizing clear overhead space by pairing heavy pallet racking with rack-supported mezzanine floors to double picking square footage without adding civil footprint.
With ocean freight volatility, procurement officers require suppliers to maximize container cubic efficiency. HEDA Shelves engineers computerized bundle packing patterns, pairing nesting beams, pre-punched knock-down frames, and serialized component labeling that cuts on-site sorting times by 40% upon container unsealing.
Authoritative answers addressing engineering tolerances, seismic factors, Civil Defense approvals, and export logistics for global project managers and contractors.
Our heavy-duty pallet racking systems are engineered in strict compliance with European Standard EN 15512:2020 (Steel static storage systems - Specification of beam-and-upright pallet racking systems), EN 15620 (Tolerances, deformations and clearances), and EN 15635 (Application and maintenance of storage equipment). In addition, for North American and Australasian markets, our engineering designs reference RMI MH16.1 and AS 4084.
Our factory holds valid CE Certification under No. 2435-CPR-8605159 and ISO 9001:2015 Certification under No. 18624Q00169R0M. Mill test certificates (MTC) proving the chemical composition and yield strength (Q235B ≥ 235 MPa, Q355B ≥ 355 MPa) are provided with every container manifest.
Before powder application, all roll-formed steel components pass through a continuous automated chemical pretreatment line consisting of hot alkaline degreasing, acid pickling to eliminate mill scale, and iron-zinc phosphating. This chemically seals the steel and provides an adhesive microscopic substrate.
Components then receive an electrostatic thermosetting epoxy-polyester powder coating applied at 60 to 90 microns thickness, cured at 180°C–200°C. This finish passes 500-hour Salt Spray Testing (ASTM B117) without blistering, making it ideal for coastal logistics parks in Dubai, Jeddah, Dammam, and Southeast Asia. For outdoor yards, hot-dip galvanized finishes (HDG) to ISO 1461 are available.
To produce an optimized 2D layout, 3D render, and structural load sheet, our design department needs the following information:
1. Architectural floor plan showing column grid spacing, building clear height under roof beams, floor slab thickness, concrete compressive strength (e.g., C25/30), and fire exit doors.
2. Pallet dimensions (Width × Depth × Overall Loaded Height) and maximum gross weight per pallet position.
3. Material handling equipment (forklift type, collapsed mast height, maximum reach height, and minimum turning radius/right-angle stacking aisle requirement).
4. Environmental parameters (seismic zone classification and operating temperatures, especially for cold storage).
Yes. Municipal fire departments, Civil Defense authorities (such as UAE Civil Defense, Saudi Civil Defense), and insurance underwriters (FM Global) require strict safety clearances. Our layout engineering incorporates transverse and longitudinal flue spaces (typically 75mm–150mm) according to NFPA 13 standards for in-rack fire sprinkler penetration.
We provide comprehensive structural load charts, emergency escape aisle clearances, column base anchor calculations, and certified load capacity plaques (load warning notices) required for sign-off by structural engineers of record.
Under international EN 15512 and FEM 10.2.02 codes, the maximum vertical deflection for pallet beams under a uniformly distributed load (UDL) must not exceed 1/200th of the clear beam span (Span / 200). For automated or high-precision AS/RS systems, we design to an even stricter deflection limit of Span / 300 or Span / 400.
Each beam pair is secured with safety locking pins certified against accidental upward dislodgement forces exceeding 5,000N, preventing beam displacement during forklift loading errors.
All beams are bundled in custom timber dunnage cradles, separated with non-abrasive corrugated spacer pads, and strapped with high-tensile PET bands with corner edge protectors. Upright frames are packed flat with diagonal bracing protected by stretch film wraps to prevent friction scoring.
Base plates, anchors, shims, beam pins, and fasteners are crated in seaworthy, steel-banded wooden boxes. Every bundle is tagged with weatherproof barcodes and color-coded tags matching the AutoCAD installation drawings, enabling rapid inventory control upon arrival at destination ports worldwide.
Partner directly with a CE and ISO 9001 certified manufacturer. From structural design calculations to direct export shipping, our 300+ technical specialists will help optimize your warehouse's storage density, safety, and operating efficiency.
Share your architectural floor layout, pallet data, and timeline to receive an initial engineering design within 24 hours.
Inquire Now