High-Performance Warehouse Shelving & Industrial Racking Systems
Explore our certified portfolio of structural warehouse storage hardware. Engineered for dynamic logistics distribution centers, cold-storage vaults, e-commerce fulfilment hubs, and harsh industrial environments.
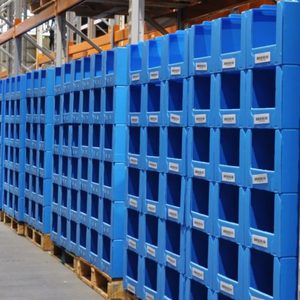
Stackable PP Corrugated Warehouse Picking Bins For Apparel & Garments
Ultra-durable, moisture-resistant corrugated PP bin containers configured specifically for high-density carton flow racks and order fulfillment shelving arrays.
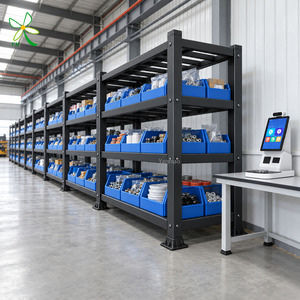
Corrosion Protection Stackable FRP Warehouse Storage Rack System 1200mm
Engineered for fertilizer plants, maritime coastal warehouses, and chemical processing depots where aggressive acid-alkali vapors quickly degrade traditional steel.
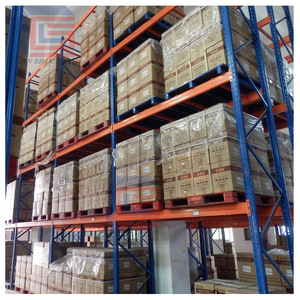
Industrial Heavy Duty Steel Pallet Rack System For Distribution Centers
High-strength teardrop and box-beam structural selective racking with integral safety locking pins, designed for high-bay reach-truck logistics facilities.
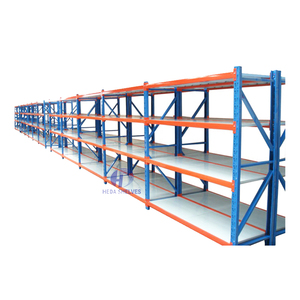
Adjustable Steel Commercial Warehouse Storage Shelving & Stacking Racks
Modular boltless longspan shelving configurable with wire mesh decks, galvanized drop-in steel plates, or solid panels for automotive parts and carton storage.
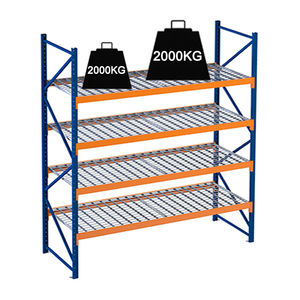
Stackable Storage Post Pallet Racking Systems (1000kg to 3000kg Payload)
Flexible bulk pallet stacking solutions eliminating dedicated aisle space during seasonal demand surges in cold stores, agricultural hubs, and tyre distribution centers.
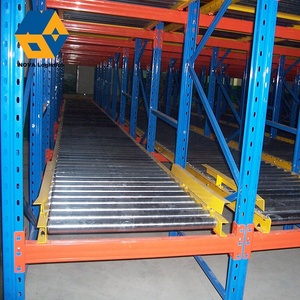
Industrial High-Throughput Gravity Pallet Flow Rack Dynamic Live Storage
Inclined gravity roller tracks with integrated centrifugal brake drums, engineered for perishable pharmaceuticals, FMCG distribution, and beverage cold-stores.
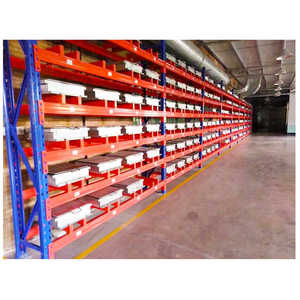
Direct Factory High-Density Drive-In Pallet Storage Racking & Narrow Lane
Continuous lane storage maximizing cubic warehouse capacity by eliminating conventional working aisles, featuring cold-rolled pallet support guide rails.
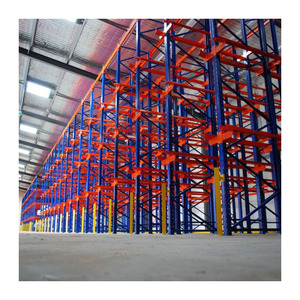
Heavy Duty Industrial Drive-In Racking System with Custom Seismic Bracing
Rugged drive-through and drive-in structural steel configuration fortified with heavy upright column protectors to resist daily industrial forklift interaction.
CE Certified Warehouse Shelving: The Definitive Compliance Guide
Procuring certified warehouse shelving is not merely a purchasing milestone—it is a life-safety and liability imperative. Discover how certified structural engineering differentiates genuine industrial racks from non-compliant commodity steel.
EN 15512 Structural Verification
Under CE Certification (CPR Construction Products Regulation), racking systems must undergo rigorous limit-state structural design calculations. EN 15512 dictates specific yield testing for cold-formed upright profiles, connector stub stiffness evaluations, and partial load factor verifications to prevent progressive structural collapse under uneven dynamic loading.
EN 15620 Tolerances & Clearances
Operational safety demands precise geometrical tolerances. EN 15620 sets microscopic thresholds for beam vertical deflection (maximum 1/200th of clear span) and upright perpendicularity. Adherence guarantees seamless interface with automated very narrow aisle (VNA) reach trucks, AGV guided forks, and modern AS/RS crane shuttles.
Traceable Mill Certifications & Q355B Steel
Unlike uncertified suppliers who source low-grade scrap re-roll steel with unpredictable carbon embrittlement, CE compliant manufacturers utilize certified prime hot-rolled and cold-rolled steel coils (Q235B, Q355B / S235JR, S355JR). All material arrives with EN 10204 Type 3.1 chemical analysis and tensile test certification.
| Evaluation Metric | CE Certified Industrial Shelving (Our Standard) | Uncertified Market Commodity Shelving | Operational Risk Impact |
|---|---|---|---|
| Raw Material Specification | Certified prime steel (Q355B / Q235B) with documented mechanical tensile properties. | Unverified commercial scrap re-roll with variable manganese & carbon ratios. | Unpredictable cold-embrittlement shear failure under static capacity. |
| Beam Deflection Safety Factor | L/200 max under full design payload (Safety Factor ≥ 1.5 conforming to FEM 10.2.02). | Exceeds L/120 deflection; permanent structural plastic deformation. | Pallet binding, dislodgement, and catastrophic beam drop during picking. |
| Surface Pretreatment & Coating | 10-stage immersion pickling, zinc phosphating, and electrostatic epoxy-polyester coating. | Wiped with mineral spirit solvent; direct flash powder baking. | Rapid subcutaneous corrosion blistering, micro-cracking, and structural loss. |
| Seismic & Dynamic Modeling | Full 3D Finite Element Analysis (FEA) compliant with Eurocode 3 and RMI guidelines. | Empirical guesswork without node moment-rotation calculations. | Building department permit rejection, catastrophic seismic resonance collapse. |
| Factory Traceability & Auditing | Notified Body audited annually (CE CPR 305/2011/EU & ISO 9001:2015). | No third-party surveillance; self-declared unverified test sheets. | Invalidated property insurance claims in the event of warehouse accident. |
Future Procurement Trends in Industrial Warehouse Storage
Warehouse asset procurement is shifting from standalone steel purchasing to agile, automation-ready logistics infrastructure. Procurement executives and supply chain directors must account for four prevailing trends.
Total Vertical Volumetric Maximization
Industrial real estate rents in major global transportation nodes have surged dramatically. Procurement teams are discarding low-profile 6-meter layouts in favor of ultra-high vertical systems reaching 12 to 18 meters. Sourcing certified high-density racking platforms—such as Drive-In, Radio Shuttle, and Multi-Tier Rack-Supported Mezzanines—allows logistics operators to triple warehouse pallet volume without acquiring additional land or expanding structural building footings.
Automation-Ready Hybrid Racking
Forward-looking procurement contracts now demand "Automation-Ready" adaptability. Even if a facility initially operates conventional counterbalance or reach forklifts, racking components must feature pre-punched mounting patterns for floor guide wires, AGV/AMR pallet docking bays, and future AS/RS crane shuttles. Sourcing standardized European modular profiles ensures capital expenditure is protected against future robotic retrofit obsolescence.
Microclimate & Cold-Chain Sourcing
The explosive expansion of temperature-controlled pharmaceutical distribution and frozen food logistics has driven specialized demand for cold-resistant steel storage. Standard structural carbon steels become susceptible to brittle fractures below -20°C. Modern procurement specifications demand Charpy V-notch impact-tested steel, continuous hot-dip galvanization (HDG), and condensation-resistant thermoset resins for cold vault reliability.
Total Life-Cycle & ESG Traceability
Global Fortune 500 enterprises and Tier-1 logistics companies require transparent Environmental, Social, and Governance (ESG) manufacturing footprints. Procurement directives favor manufacturers utilizing automated powder coating recovery lines (zero VOC emission), closed-loop water treatment during pickling, and 100% recyclable structural grade European standard steel alloys with documented RoHS compliance.
Industry Development & Technological Advancements
The manufacturing of warehouse storage systems has evolved from traditional metal stamping into high-precision structural mechanics and algorithmic layout optimization.
Algorithmic Digital Twin & 3D Modeling
Modern warehouse design utilizes Building Information Modeling (BIM) combined with parametric structural algorithms. Our design engineers generate millimeter-accurate 3D digital twins before fabrication begins. This simulates forklift turning radiuses, fire sprinkler suppression spray cones, building column clearance offsets, and local seismic acceleration responses under simulated earthquake loads.
Advanced Roll-Forming Metallurgy
Continuous CNC cold-roll-forming lines equipped with up to 26 forming rolling passes eliminate micro-stress fractures in high-yield structural steel coils. Computerized in-line optical punch monitors maintain hole spacing tolerances within ±0.1mm across continuous 12-meter upright columns, guaranteeing frictionless connector lug engagement during warehouse erection.
Intelligent Semi-Automated Shuttles
Radio shuttle carriers now feature integrated LiDAR obstacle detection, brushless DC electric motors, and long-cycle lithium iron phosphate (LiFePO4) power cells. These automated shuttles travel at speeds up to 1.2 m/s inside dense pallet tunnels, communicating in real-time with Warehouse Execution Systems (WES) to enable FIFO or LIFO inventory sequences effortlessly.
Nanoceramic Surface Passivation
Replacing traditional iron phosphating, innovative nanoceramic zirconium conversion coatings form an ultra-dense chemical molecular barrier against atmospheric humidity and salty coastal environments. Combined with heavy-duty TGIC polyester powder coatings cured at 200°C, this provides over 800 hours of continuous salt-spray resistance (ASTM B117 standards).
Why Global EPC Contractors & Logistics Leaders Partner With Us
Since 2001, Guangzhou Heda Shelves Co., Ltd. has stood as a tier-1 global manufacturer of heavy-duty warehouse storage systems, exporting factory-direct to over 120 countries across North America, Europe, Southeast Asia, and the GCC.
Our Fully Integrated 10-Step In-House Manufacturing Workflow
Every upright, beam, bracket, and connector is manufactured strictly within our own facility under unified ISO 9001:2015 traceability.

Raw Materials
Spectrometric assay & thickness gauge verification on Q355B coils.

Precision Cutting
Automated uncoiling, laser slitting, and CNC shearing.

CNC Punching
High-speed continuous progressive die punch (50mm/75mm pitch).

Cold Bending
Computerized multi-angle press braking for baseplates & arms.

Profile Roll Forming
26-station continuous cold roll lines forming complex uprights.

Surface Polishing
Shot-blasting and mechanical de-burring of sharp cut edges.

Robotic Welding
Automated CO2 gas-shielded seam welding for end-connectors.

Pickling & Phosphating
Multi-stage acid de-scaling, hot water wash, and zinc phosphating.

Powder Coating
Nordson automated spray guns & 200°C polymerization curing tunnel.

QC & Ocean Bundling
Caliper coating check, structural test load, and maritime packing.
Fully Audited & Internationally Certified Storage Solutions
Procurement teams and consulting engineers can verify our credentials directly with accredited third-party certification bodies:
-
CE Certification: Certificate No.
2435-CPR-8605159compliant with EU Construction Products Regulation. -
ISO 9001:2015 Quality Management: Certificate No.
18624Q00169R0Mvalid through June 2027. -
RoHS & Heavy-Metal Free Testing: Ecological surface coatings non-hazardous to food packaging.
-
Global Maritime Logistics: Seamless containerized shipping to Jebel Ali, Dammam, Jeddah, Hamad, Sohar, Rotterdam, and Los Angeles.
Frequently Asked Questions: Warehouse Shelving & Racking
In-depth technical answers addressing structural calculations, safety compliance, installation logistics, and international maritime delivery for EPC engineers and procurement officers.
Q1: How does CE certification protect our company under civil structural liability?
CE Certification (under CPR 305/2011/EU and EN 15512) guarantees that steel racking profiles have been mathematically modeled and physically tested to withstand stated working limit states. In the event of building structural inspections, municipal fire department audits, or insurance claims, certified documentation proves the storage system meets structural design codes, shielding facility owners from catastrophic negligence liabilities.
Q2: What specific project inputs are required for an engineering CAD & 3D layout?
To produce a fully compliant 2D CAD layout and 3D rendering within 24–48 hours, our engineering department requires: (1) Architectural floor plan with column grid positions, ceiling clear height, and dock door placements; (2) Pallet dimensions (W × D × H including cargo overhang) and maximum gross pallet weight; (3) Forklift model, minimum aisle turning radius (AST), and maximum mast lift height; (4) Local seismic zone coefficient.
Q3: What steel grade do you utilize for heavy-duty selective uprights and beams?
Our standard heavy-duty structural members utilize certified prime Q355B (equivalent to European standard S355JR / ASTM A572 Grade 50), possessing a minimum yield strength of 355 MPa and high tensile elongation properties. For standard duty shelving components, high-grade Q235B (S235JR) is utilized. Certified mill test sheets (MTC) detailing chemical composition and yield points are supplied with every shipment container.
Q4: How do your racks resist corrosion in harsh, humid coastal or cold-store environments?
Prior to coating, steel members undergo continuous industrial immersion through acid pickling to strip mill scale, followed by surface zinc phosphating. We then apply heavy-duty electrostatic thermosetting epoxy-polyester powder baked at 200°C. For high-humidity coastal ports (such as Dubai, Jeddah, Dammam) or outdoor lumber and pipe yards, hot-dip galvanization conforming to ISO 1461 is available, providing sacrificial zinc protection exceeding 30 years.
Q5: What deflection ratio governs beam load safety in your structural designs?
All load-bearing beams conform strictly to FEM 10.2.02 and EN 15512 standards, adhering to a maximum deflection limit of 1/200th (δ ≤ L/200) of the unsupported span length when carrying full design static payload. Furthermore, every beam-to-column connector is secured via automated spring-steel safety pins rated against accidental vertical upward dislodgement forces exceeding 5,000 N.
Q6: How is export cargo packed to prevent transit damage during long-haul ocean voyages?
Components are packed with specialized export steel dunnage framing and high-density corrugated wrap. Upright frames and beam bundles are banded using high-tensile PET strapping with reinforced corner protectors. Hardware and small brackets are sealed in wooden crates conforming to ISPM 15 heat-treatment standards. Every component bundle is barcode-labeled to correspond directly with the supplied CAD installation erection drawings.
Q7: Can your racking layouts satisfy Civil Defense, NFPA, and FM Global fire approvals?
Yes. Our engineering drawings calculate and clearly indicate longitudinal and transverse flue spaces (typically 75mm to 150mm separation between back-to-back pallets) in complete accordance with NFPA 13 sprinkler standard guidelines. This ensures uninhibited vertical water penetration from ceiling ESFR sprinklers, allowing your engineering consultant to achieve swift municipal Civil Defense and insurer compliance approvals.
Q8: Do you provide on-site installation supervision and erection assistance?
Yes. In addition to supplying complete step-by-step CAD isometric erection drawings and technical assembly manuals, our senior installation engineers are available for worldwide deployment to oversee local labor, perform torque-wrench anchor bolt inspections, and issue final pre-commissioning structural load sign-off certificates for industrial projects.
Accelerate Your Warehouse Capacity With Certified Engineering
Connect directly with our senior structural storage engineers. Receive a free comprehensive warehouse 2D CAD floor plan, 3D photorealistic digital rendering, and exact factory-direct quotation within 24 hours.