Factory-Direct Rolling & Gravity Flow Pallet Storage Systems
Precision-engineered cold-formed steel racking, gravity flow roller tracks, demountable tyre storage solutions, and dynamic mobile logistics carts certified to global CE, ISO 9001:2015, and RoHS benchmarks.
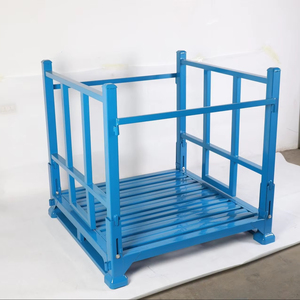
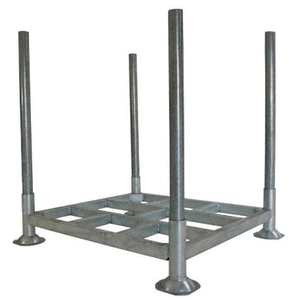
Custom heavy-duty post nesting, high-density modular tyre storage, powder-coated anti-corrosion finish, 1,000–1,500 kg payload capacity.
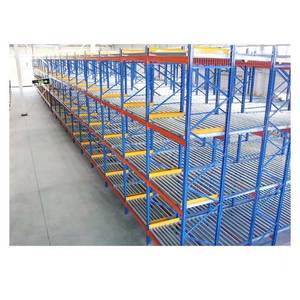
Strict FIFO dynamic lanes, integrated centrifugal speed controllers, automatic separation brakes, 2,000 kg capacity per pallet position.
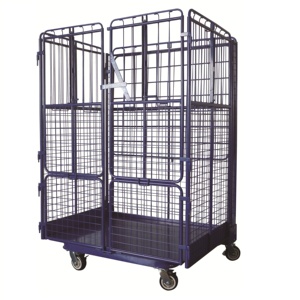
Reinforced electro-galvanized wire mesh, collapsible design for reverse logistics, smooth polyurethane castor wheels with foot brakes.
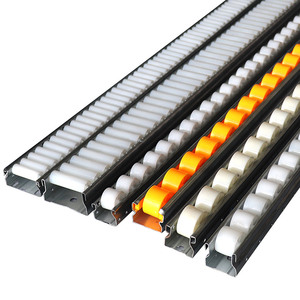
Extruded aluminium alloy roller rails, low rolling resistance bearings, high pitch flexibility, engineered for fast-moving consumer goods picking.
Hot-dip galvanized structural profile, ideal for cold rooms and marine-corrosive logistics hubs, tool-less snap-in cross beam locks.
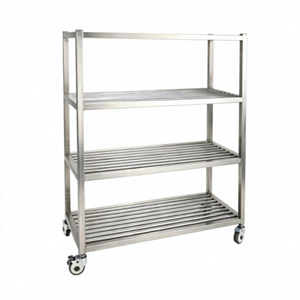
AISI 304 food-grade stainless structural steel, ventilated hollow slat shelves, chemical-washdown compatible, heavy-duty directional brake casters.
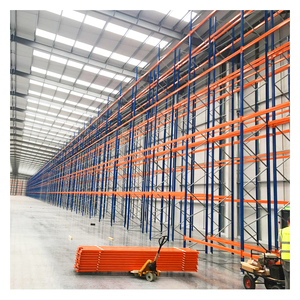
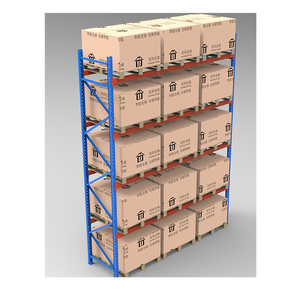
Certified Q235B cold-rolled structural steel, optimized omega upright profiles, electrostatic powder coating, multi-tier capacity up to 4,500 kg/tier.
75mm pitch beam adjustments, high seismic tolerance connection tabs, modular compatibility with mobile chassis bases and roller drop-in beds.
25+
Years Engineering (Est. 2001)
30,000m²
Direct Factory Campus
30,000Tons
Monthly Manufacturing Output
120+
Countries & GCC Regions Exported
Engineering Excellence: Structural Kinematics of Rolling Pallet Racks
In modern supply chain warehousing, facility footprints represent an ever-escalating capital cost. For industrial operators in high-throughput fulfillment hubs—ranging from regional Middle East logistics hubs (Dubai, Riyadh, Dammam) to European cold-chain centers—traditional static wide-aisle pallet storage creates an operational bottleneck. Static layouts dedicate up to 60% of total warehouse cubic volume strictly to forklift maneuvering aisles. Rolling Pallet Racks—comprising dynamic gravity flow pallet racking, electrically motorized mobile racking bases, and roll-cage transport trolleys—engineer out this spatial inefficiency by collapsing dead transit aisles into high-density storage cubes.
As China's premier manufacturer and turnkey structural engineer of industrial racking systems, Guangzhou Heda Shelves Co., Ltd. (HEDA Shelves) transforms raw metallurgical steel coils into high-performance dynamic storage infrastructures. Unlike standard catalogue suppliers who offer generic prefabricated frames, HEDA Shelves approaches rolling pallet storage from the fundamental physics of dynamic kinetic equilibrium, material shear strength, dynamic rolling resistance, and seismic load dampening.
1. Gravity-Fed Pallet Flow Racks (Dynamic Roller Bed Physics)
Gravity flow rolling pallet racks operate on a controlled gradient angle (typically 2.5% to 3.5% inclination) that utilizes natural gravitational acceleration to propel pallet loads from the rear loading interface to the forward unloading extraction face. The engineering challenge in high-bay gravity rolling systems is avoiding uncontrolled acceleration while eliminating stall friction. HEDA Shelves addresses this through precision multi-roller configurations:
- Dynamic Centrifugal Speed Controllers (Brake Rollers): As pallet weights scale from 500 kg to 2,000 kg per position, kinetic energy increases exponentially. Our brake rollers utilize internal planetary gears and viscous centrifugal fluid mechanisms to govern terminal rolling velocity between 0.20 m/s and 0.28 m/s, preventing damaging impact against the terminal front-stop frame.
- Automatic Pallet Separation Dampers: When the foremost pallet reaches the picking face, it triggers a mechanical separator lock. This decouples the lead pallet from the hydrostatic queue pressure of the behind pallets, allowing forklift operators to extract the front pallet safely without risk of load pinch, pallet binding, or forklift mast derailment.
- Heavy-Gauge Split and Full-Width Cylindrical Steel Rollers: Cold-drawn precision carbon steel tubing electro-galvanized or polyurethane-sheathed with sealed deep-groove 6204-2RS precision bearings guarantees continuous rotation under deep sub-zero conditions (-30°C cold chain) and high-dust desert logistics facilities alike.
2. Motorized Mobile Base Rolling Racking Systems
For maximum cubic density with 100% selective pallet accessibility, HEDA Shelves engineers structural racking mounted on heavy-duty motorized bogies that glide over floor-embedded high-tensile guide rails. By mobilizing continuous rack runs of up to 40 meters, multiple rows require only a single moving access aisle, unlocking an immediate 85% to 90% increase in effective storage capacity within the identical floor plate.
Driven by synchronous frequency-inverter three-phase gearmotors, our mobile chassis systems incorporate micro-PLC logic controllers, photoelectric obstacle light-curtains, physical bumper contact cutoffs, and floor-level interlocks to ensure absolute compliance with international occupational safety mandates including EN 15095 and OSHA regulations.
Comprehensive Technical Specification Comparison Matrix
Selecting the correct dynamic rolling racking topology requires evaluating pallet integrity, throughput velocity, picking selectivity, and capital expenditure amortization. The engineering matrix below details structural baselines across our core dynamic product architectures:
| System Architecture |
Kinematic Mechanism |
Load Capacity (per unit/level) |
Space Efficiency |
Inventory Rotation |
Target Operational Domain |
| Gravity Pallet Flow Rack |
Gravity incline (2.5%–3.5%) + centrifugal brake rollers |
500 kg – 2,200 kg / pallet |
Up to 80% footprint utilization |
Strict FIFO (First-In, First-Out) |
Cold storage, perishable foods, pharmaceutical buffer |
| Motorized Mobile Pallet Racking |
Electric gearmotor + recessed heavy floor guidance tracks |
Up to 24,000 kg / movable bay |
Up to 90% footprint utilization |
100% Selective / Random Access |
Raw material staging, cold stores, low SKU turnover |
| Demountable Mobile Stacking Racks |
Forklift-transported nesting posts & cupped feet |
1,000 kg – 1,800 kg / base |
High vertical density / 100% flexible |
LIFO / Block Stacking |
Tyre logistics, automotive assembly, seasonal surge buffer |
| Rolling Wire Mesh Logistics Cages |
Manual hand-push or tugger train via casters |
500 kg – 800 kg / cart |
Nestable for reverse transport |
Dynamic Point-to-Point |
Retail cross-docking, parcel sorting, line-side replenishment |
| Aluminium Rolling Rails Flow Rack |
Sloped light-alloy gravity roller strips |
150 kg – 450 kg / linear meter |
High density carton / tote cube |
FIFO Case Picking |
E-commerce fulfillment, kitting cells, assembly workstations |
Every structural upright manufactured by HEDA Shelves utilizes cold-rolled Q235B or high-strength Q355B structural steel with yield strengths surpassing 235–355 MPa, tested under severe static and cyclic dynamic deflection thresholds per FEM 10.2.02 and ANSI MH16.1 specifications.
Future Procurement & Technological Trends in Rolling Pallet Systems
Procurement directors and supply chain planners cannot view storage equipment as static metal hardware. Over the next five to ten years, several structural transitions are reshaping the global procurement landscape for rolling pallet racking:
1. Convergence with Autonomous Mobile Robots (AMRs)
Dynamic rolling carts and mobile racking systems are transitioning toward automated interface points. Modern gravity flow discharges now feature laser-guided AMR docking stations and optical pallet presence sensors, allowing robotic lifters to pull pallets without human forklift intervention.
2. IoT-Enabled Roller Speed & Vibration Diagnostics
In ultra-deep gravity flow systems (15–25 pallets deep), a seized roller can create catastrophic pallet jams. Smart magnetic brake rollers featuring embedded vibration and thermal sensors provide predictive telemetry via LoRaWAN/industrial IoT networks, alerting facility managers prior to mechanical breakdown.
3. Extreme Sub-Zero Cold Chain Optimizations
With food security initiatives driving major cold-storage expansions across the GCC, Africa, and Southeast Asia, dynamic rolling racks must survive -30°C environments without lubricant freezing or polymer roller embrittlement. Low-temperature synthetic greases and specialized steel grades prevent brittle fractures.
4. Modular Demountability for Flexible Supply Chains
Rigid, floor-bolted racking is increasingly supplemented by modular demountable stacking racks (tyre racks and stackable post pallets). Supply chains experiencing violent seasonal volume surges lease temporary facilities, deploy modular mobile racks within 48 hours, and collapse them for empty transport when peak season wanes.
5. Stringent Carbon Border Adjustment & Recycled Content
Procurement teams in Europe, North America, and multinational 3PLs actively audit the carbon footprint of structural steel. Electric arc furnace (EAF) processing, high scrap steel utilization, and heavy-metal-free electrostatic powder coating (certified under RoHS standards) represent prerequisite procurement mandates.
6. Shift Toward Factory-Direct Engineering Procurement
Global supply chain leaders are bypassing trading intermediaries to work straight with primary Chinese manufacturers. Direct factory engagement slashes project costs by 20% to 35%, eliminates communicative latency in CAD/3D revisions, and ensures uncompromised component traceability from mill test certificates to installation.
Why Guangzhou Heda Shelves Co., Ltd. Leads the Global Rolling Rack Industry
Founded in 2001, Guangzhou Heda Shelves Co., Ltd. has established an unrivaled global reputation as an authoritative designer, manufacturer, and structural solution provider for advanced warehouse racking systems. Headquartered in Guangzhou, China, our expansive 30,000 square meter modern manufacturing complex is staffed by over 300 skilled technical personnel, structural calculation engineers, and precision tooling specialists.
30,000 Tons Monthly Output
Massive production scalability ensures the fastest delivery cycles in the racking sector. We process multi-thousand-pallet mega-projects within 15 to 25 business days without compromising dimensional tolerances or coating integrity.
CE, ISO 9001 & RoHS Certified
Verified compliance through official international accreditation: CE certification (No. 2435-CPR-8605159) for structural conformity, ISO 9001:2015 quality management (No. 18624Q00169R0M, valid to 2027), and RoHS environmental testing.
Over 10,000 Global Cases
From the demanding marine environments of UAE (Jebel Ali, Khalifa Port), Saudi Arabia (Dammam, Jeddah), and Qatar to industrial plants in Europe, Southeast Asia, and the Americas, our racking systems have secured over 10,000 complex facilities globally.
Our 10-Step Precision Racking Manufacturing Lifecycle
Quality control in dynamic rolling racking is non-negotiable. An uneven punch pitch or microscopic curvature in an upright column can induce racking twist under 50-ton dynamic loads. HEDA Shelves enforces a rigorous 10-step internal manufacturing protocol:
Step 01
Raw Material Testing

Step 02
Precision Steel Cutting

Step 03
Automated Punching

Step 04
Cold Bending Forming

Step 05
Profile Roll Forming

Step 06
Surface Polishing

Step 07
Robotic Welds

Step 08
Pickling & Phosphating

Step 09
Electrostatic Coating

Step 10
QC & Container Loading

Crucially, our immersion pre-treatment includes a rigorous chemical pickling and phosphating acid wash that strips all microscopic mill scale, oils, and surface oxidation before powder application. This achieves electrostatic powder coating adhesion exceeding ISO 2409 Cross-Hatch Class 0, preventing premature blistering, peeling, and corrosion even in coastal ports with 95% relative humidity and intense ambient saline levels.
Comprehensive Technical & Procurement FAQ for Rolling Pallet Systems
To support procurement officers, structural consultants, and warehouse automation architects, our senior engineering team addresses the most critical technical inquiries encountered during project specification:
1. What determines the exact slope angle in gravity rolling pallet flow racks?
+
The standard engineering slope ranges from 2.5% to 3.5% (approx. 1.5° to 2°). The specific angle is determined by three variables: pallet bottom condition (wooden euro-pallets, perimeter-base plastic skids, or corrugated metal runners), gross pallet payload weight, and ambient facility operating temperature. Uneven or softer wooden pallets experience higher rolling friction and require a 3.0% to 3.5% gradient, whereas rigid plastic pallets with heavy loads (1,500 kg) roll readily at 2.5%. During design, HEDA Shelves conducts physical test bed simulations on your actual client pallets to calibrate roller pitch and brake intervals.
2. How do brake rollers prevent runaway pallets in deep gravity flow lanes?
+
In lanes spanning 5 to 25 pallets deep, terminal velocity must be strictly regulated. HEDA Shelves integrates internal centrifugal brake rollers at calculated intervals (typically every two pallet lengths). As a rolling pallet glides across the brake roller, friction activates an internal planetary gear assembly that drives a heavy viscous rotor or centrifugal brake shoe. The faster the pallet attempts to roll, the higher the counteracting braking torque generated, keeping pallet descent speed uniformly capped at a safe 0.25 m/s.
3. Can motorized mobile pallet racking operate safely on existing warehouse concrete slabs?
+
Mobile pallet racking consolidates tremendous dynamic point loads onto heavy steel bogie wheels. A standard industrial slab must meet strict flatness, levelness (DIN 18202 or ASTM E1155 F-min 75), and compressive strength requirements (typically minimum 25–30 MPa with double reinforcement mesh). For existing facilities, HEDA Shelves engineers customized surface-grouted or slab-cut recessed guide tracks backed by structural epoxy mortar beddings to distribute wheel point stresses across the concrete sub-base without slab cracking or deflection.
4. What safety redundancy mechanisms are engineered into HEDA Shelves rolling systems?
+
In gravity systems, our fail-safe mechanisms include heavy-duty mechanical end-stops anchored directly into the structural cross beams, load separator trip levers that prevent secondary pallet hydrostatic pressure on the picking face, and steel beam entry guides that steer misaligned pallets onto the track centerline. For motorized mobile racks, multi-zone optical safety light curtains, continuous touch-sensitive bottom safety bars, and emergency stop interlocks instantly halt drive motors within 15 milliseconds if personnel or foreign objects breach an active aisle.
5. How does HEDA Shelves guarantee corrosion resistance in harsh, coastal, or humid logistics parks?
+
Corrosion failure in structural steel originates under poor surface preparation. HEDA Shelves executes a complete automated 10-step surface treatment process: degreasing, twin acid pickling washes, surface activation, micro-crystalline zinc phosphating, deionized water rinsing, and high-temperature curing. The steel is then coated with thermosetting polyester electrostatic powder at 70–110 microns dry film thickness. For outdoor yards, harsh chemical zones, or intense coastal climates, we offer continuous hot-dip galvanization conforming to EN ISO 1461 with zinc bath coatings exceeding 600 g/m² (85 microns) for 25+ years of zero-rust operational life.
6. What data is required to generate a turnkey 2D CAD layout and 3D architectural rendering?
+
To provide our free, rapid 2D/3D structural design within 24–48 hours, our engineering department requires: (1) Architectural CAD floor plan showing building column centers, door openings, clear height under roof beams, and fire sprinkler clearances; (2) Pallet dimensions (Length × Width × Height including product overhang) and gross weight per pallet; (3) Operational forklift type, turning radius, and maximum reach height; (4) Total SKU profile count, daily inbound/outbound pallet turnover velocity, and preferred picking logic (FIFO or LIFO).
7. How are high-density rolling rack components packaged for global ocean container freight?
+
Export damage creates severe site delays. HEDA Shelves employs heavy-duty export packing: upright frames are strapped with high-tensile PET banding into rigid wooden bunks, interleaved with corrugated buffer cardboard and wrapped in waterproof polyethylene heat-shrink film. Roller tracks and sensitive brake mechanisms are encased in reinforced non-fumigation plywood crates. Every bundle is barcode-labeled with assembly tags corresponding identically to the color-coded installation erection drawings.
8. What on-site and remote installation support does HEDA Shelves provide?
+
Each project is dispatched with comprehensive structural layout schematics, 3D step-by-step assembly diagrams, and torque bolt tightening specification sheets. We provide 24/7 remote video engineering guidance for your local mechanical contracting teams. For large-scale multi-tier mezzanines or multi-thousand-pallet dynamic projects, HEDA Shelves deploys experienced on-site bilingual structural installation superintendents to supervise alignment, track leveling, safety system calibration, and load test commissioning.
Request Your Custom Warehouse Layout & Dynamic Racking Quote
Partner directly with China's authoritative rolling pallet rack manufacturer. Share your warehouse drawings to receive structural calculations, free 2D/3D CAD layouts, and factory-direct pricing within 24 hours.