High-Yield Steel Pallet Racking & Industrial Storage Solutions
Explore our heavy-duty warehouse racking and modular shelving assemblies manufactured from certified Q235B/Q355B structural coil steel, cold-formed with micron-level tolerances for distribution hubs and 3PL enterprises.
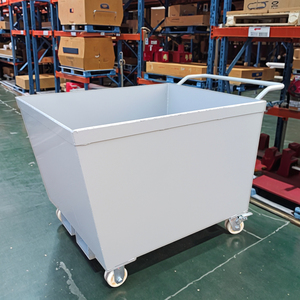 Stackable
CASE CARTER OEM 600*400*400mm Foldable Stack Wire Mesh Steel Pallet Container
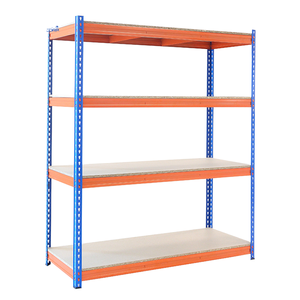 Automated Ready
High-Load 5-Layer Steel Corrosion Protection Galvanized Automated Shelves 150kg/Layer
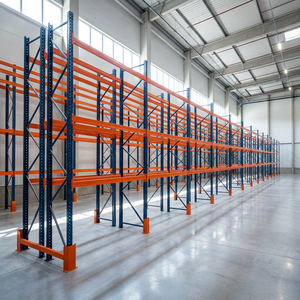 Heavy Duty
Garage Warehouse Rack Adjustable Storage Stacking Racks Selective Warehouse Shelving
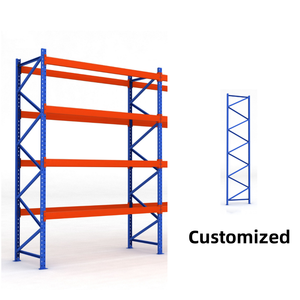 Engineered Beam
Warehouse Steel Heavy Duty Beam Rack Pallet Rack Shelf Industrial Logistics System
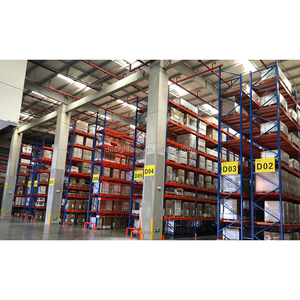 EU Standard
 Galvanized Steel Warehouse Heavy Duty Selective Racking System
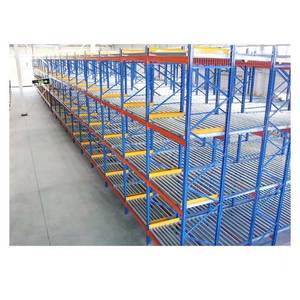 FIFO Dynamics
CE Certified Anti-Rust 2000kg Load Capacity Gravity Pallet Racking Heavy Duty Roller Rack
 Quick Assembly
Medium Heavy Duty Adjustable Steel Storage Rack Boltless Metal Shelving for Middle East
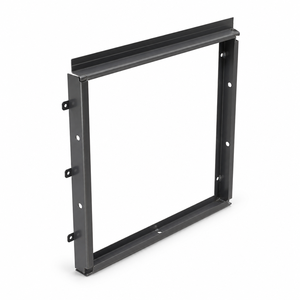 OEM Custom Fab
Bulk Tubular Subframe Metal Frames Fabrication Crossmember Carrier Pallet Platform Rack
Direct Chinese Factory Advantage: Precision Roll-Forming & Certified Structural Steel
Founded in 2001, Guangzhou Heda Shelves Co., Ltd. (HEDA Shelves) operates as a Tier-1 Chinese designer, structural engineer, and manufacturer of turnkey warehouse storage and intralogistics racking systems. Backed by 300+ technical personnel and state-of-the-art cold-bending lines, we engineer high-density logistics storage that directly complies with the most demanding international engineering codes, including European EN 15512:2020, FEM 10.2.02, American RMI (Rack Manufacturers Institute), and ISO 9001:2015.
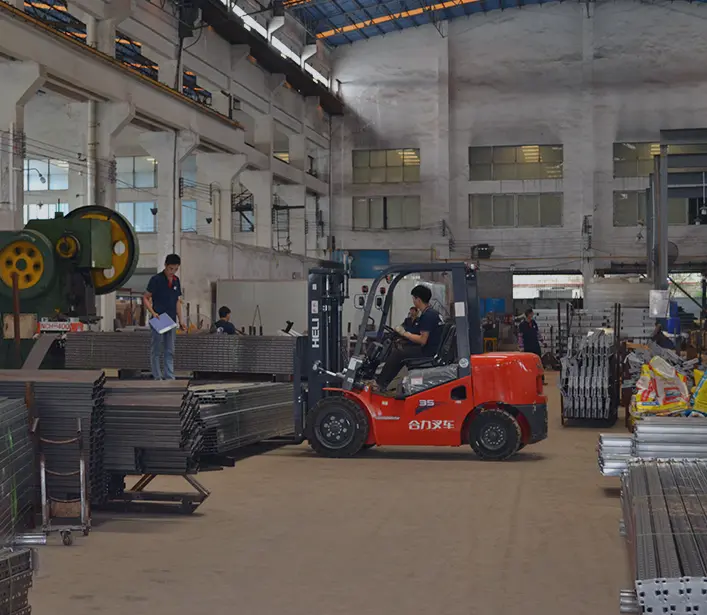
Unlike trading intermediaries, our in-house manufacturing controls every variable from raw cold-rolled steel slitting to multi-station automated column punching, continuous automated roll-forming, robotic MIG welding, 10-stage chemical surface pretreatment, and electrostatic thermosetting powder coating.
Why Tier-1 3PLs and EPC Contractors Source Racks from China
Global supply chain directors require mathematical predictability: high load factors per dollar invested, verifiable anti-corrosion chemistry, and optimized container stuffing that slashes landed logistics overhead.
Raw Material Scale & Steel Parity
China produces over 50% of the world’s crude steel. Sourcing directly from our Guangzhou facility eliminates layered distributor markups while securing high-grade Q235B and Q355B structural coil profiles with continuous mill test certificates (MTC) verifying chemical and yield specs.
SKD Container Packing Density
Freight rate volatility can erode procurement savings. Our dedicated export packaging protocols utilize custom steel strapping, bubble membrane dampening, and custom modular steel skids that pack upright frames and interlocking beams to achieve 98% cubic container utilization.
Turnkey CAD & 3D Engineering
We provide complimentary structural load calculations, slab deflection simulations, 2D AutoCAD equipment layouts, and full 3D rendering before metal is fed into our roll-formers, accelerating approval cycles with municipal building inspectors and Civil Defense authorities.
Future Procurement Trends: Racking Systems for the Automation Age
As commercial warehouses evolve into hyper-dense, automated micro-fulfillment facilities, racking components must transition from passive steel structures to high-precision robotic infrastructure.
ASRS & Radio Shuttle Compatibility
Modern supply chains demand millimetric precision. Next-gen pallet racking features low-tolerance upright punch pitches (±0.25mm) and reinforced guide tracks to accommodate 4-way autonomous radio shuttles, stacker cranes, and AGV counterbalanced units without mechanical jamming.
Cold Chain Thermal Expansion Control
With pharmaceutical and fresh produce fulfillment surging worldwide, specialized cold store racking (-30°C to -40°C) utilizes ductile low-temperature carbon steel and heavy-gauge hot-dip galvanizing to eliminate cryogenic micro-cracking and sub-zero paint delamination.
Seismic Resilience & FEA Modeling
Regional procurement codes increasingly mandate dynamic response spectrum analyses. Our structural engineers use Finite Element Analysis (FEA) to simulate non-linear seismic behavior, integrating high-elasticity baseplates and seismic cross-bracing that withstand up to 0.4g ground acceleration.
Green Steel & Eco Pretreatment
Complying with global corporate ESG criteria, our manufacturing incorporates lead-free, RoHS-compliant electrostatic powder formulations with zero volatile organic compounds (VOCs) and closed-loop silane nano-ceramic washing lines that drastically cut industrial water footprints.
End-to-End 10-Stage Precision Manufacturing Process
Every upright column, structural load beam, and cross-tie leaves our Guangzhou facility with full metallurgical traceability. Here is how our automated lines transform steel coils into certified logistics infrastructure.
 Step 01
Raw Materials
Spectrographic & tensile verification of certified steel coils.
 Step 02
Precision Slitting
High-speed CNC slitting lines for exact profile blanking.
 Step 03
Automated Punching
Continuous optical punching for 50/75mm hole pitches.
 Step 04
Cold Bending
Hydraulic precision pressing for custom brackets and bases.
 Step 05
Profile Roll Forming
Multi-station rolling lines producing rigid omega columns.
 Step 06
Surface Polishing
Deburring and edge rounding to eliminate snag hazards.
 Step 07
Robotic Welding
Shielded MIG robotic welding of beam end connectors.
 Step 08
Pickling & Phosphating
Multi-tank chemical bath ensuring absolute rust immunity.
 Step 09
Powder Coating
Automatic Gema electrostatic spray baked at 200°C.
 Step 10
QC & Ocean Shipping
Dimension verification and labeled sea container stuffing.
International Quality Assured: CE, ISO 9001 & RoHS Certified
Every production run complies with European Union Construction Products Regulation (CPR). Tender boards and insurers require verified documentation: our CE certificate (No. 2435-CPR-8605159) and ISO 9001:2015 management system (No. 18624Q00169R0M) are accessible for vendor registration audits.
Frequently Asked Questions for Warehouse Racking Procurement
In-depth technical answers addressing load calculations, seismic building codes, surface treatment performance, and international customs clearance.
How do you calculate permissible beam deflection and safe working load (SWL)?
According to EN 15512 and FEM 10.2.02 codes, the maximum allowable deflection for racking pallet beams is limited to L/200 (1/200th of the clear beam span). For a standard 2700mm beam carrying two 1000kg pallets, maximum allowable central deflection is 13.5mm under uniform static loading, with an ultimate limit state safety factor of 1.5 against plastic yield failure.
Can your storage layouts support local Civil Defense and fire authority approvals?
Yes. Our engineering department develops warehouse CAD blueprints that explicitly designate longitudinal and transverse flue spaces (75mm to 150mm minimum clearance between pallet backs per NFPA 13 regulations), emergency egress aisle widths, in-rack sprinkler feed pipe allowances, and stamped load rating capacities matching local municipal mandates.
What surface treatment is best for hot, humid coastal climates or cold stores?
For ambient coastal warehouses with high salinity (such as Dubai, Jeddah, Dammam, or Southeast Asian ports), our automated 10-step pickling, phosphating, and electrostatic powder coating provides a continuous film of 70–110 microns that passes 500-hour ASTM B117 salt spray testing. For outdoor yards, corrosive chemical storage, or deep freezer rooms (-30°C), we supply continuous hot-dip galvanized steel components with 60–85 micron zinc coatings conforming to ISO 1461.
What concrete slab specifications are required before anchoring upright frames?
For standard selective pallet racking up to 8m, an engineered concrete floor with minimum compressive strength of C25/30 (25-30 MPa) and a floor thickness of at least 150–200mm is recommended. Anchor embedment typically requires M12x100mm or M16x125mm heavy-duty wedge expansion bolts. For VNA and automated ASRS installations exceeding 12m, the slab must satisfy DIN 15185 or ASTM E1155 F-min/FF floor flatness criteria.
What parameters are needed to receive a free 2D CAD plan and 3D rendering?
To prepare an optimized turnkey proposal within 24 hours, our engineering team requires: (1) Architectural floor plan with clear ceiling height under beams and column grid layout, (2) Pallet dimensions (Width x Depth x Height, including product overhang), (3) Maximum gross weight per pallet, (4) Forklift specifications (minimum turning radius, mast lift height, and chassis dimensions), and (5) Temperature zone and SKU turnover frequency.
How do you manage ocean freight packaging to prevent shipping damage?
All upright frames, horizontal beams, and shelf levels are packaged in standardized semi-knocked-down (SKD) bundles banded with heavy-gauge PET strapping. Components are wrapped with anti-abrasion bubble film, and structural corner guards protect rolled edges during intermodal transfer. Every bundle features barcoded, color-coded identification tags matching the project erection drawings for rapid field sorting.
Ready to Engineer Your Warehouse for Maximum Cubic Capacity?
Consult with our senior structural racking engineers today. From space optimization audits and customized CAD design to rapid manufacturing and containerized ocean shipping, we deliver direct factory pricing with guaranteed structural compliance.