Engineered Industrial Storage Product Lines
Continuous-roll-formed upright profiles, certified load capacities up to 5,000 kg per beam level, and high-adhesion electrostatic powder finishes.
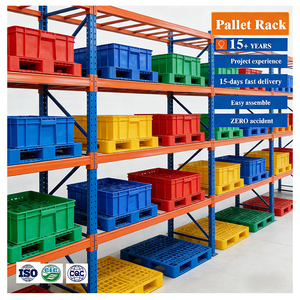 3000KG Support
Wholesale Heavy-Duty Rack Beam Rack 5 Layers 3000KG Storage
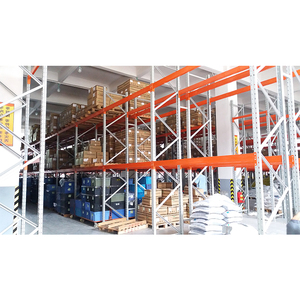 Logistics Hub
Heavy Duty Industrial Steel Pallet System For Logistics Warehouse
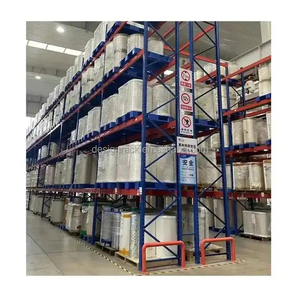 High Grade Metal
 Pallet Shelving Industrial Metal Stacking Shelf
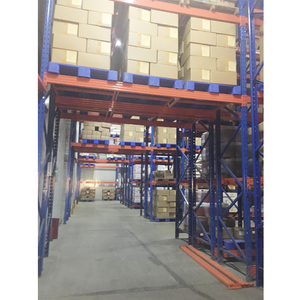 Factory Direct
Heavy Duty Steel Beam Racking System Adjustable Pallet Shelves
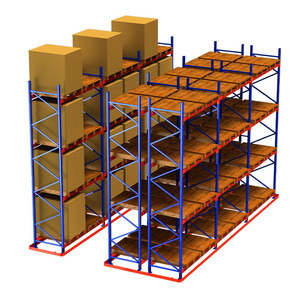 VNA High-Bay
High-Bay Beam-Type Very Narrow Aisle (VNA) Warehouse Shelving
 Structural Upright
Industrial Warehouse Pallet Racking With Reinforced Beams
 Selective Racking
Heavy Duty Epoxy Coated Selective Rack Card Slot Clip System
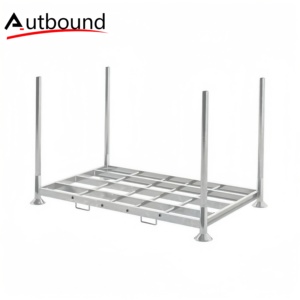 Stacking Post
Customized Heavy Duty Metal Industrial Movable Post Pallet Rack
1. Metallurgy, Load Formulations, and Structural Safety Standards
In modern industrial logistics, heavy-duty pallet racking systems are not static steel frames; they are complex, dynamic structural configurations that function as building infrastructure. Structural integrity begins at the chemical composition of raw coil steel. As an authoritative Chinese OEM and export manufacturer, we fabricate all uprights and horizontal load beams utilizing prime cold-rolled steel coils conforming to standard Q235B (yield strength ≥ 235 MPa, tensile strength 370–500 MPa) and high-tensile Q355B (yield strength ≥ 355 MPa, tensile strength 470–630 MPa) depending on height and seismic acceleration requirements.
Every roll-formed upright profile adopts an optimized continuous multi-bend omega (Ω) cross-section. By introducing multiple stiffening ribs along the web and flanges, the section modulus increases exponentially without incurring non-functional dead weight. When designing high-bay racking systems reaching 12 to 18 meters, Euler buckling load formulations and finite element calculations (FEA) dictate column perforations. Using automated precision punch presses, teardrop or 75mm-pitch diamond card slots are cold-punched prior to continuous profile roll forming, mitigating residual internal stresses and micro-fractures along perforation perimeters.
Surface longevity is critical in preventing localized structural thinning. Our continuous manufacturing loop integrates an 8-stage chemical pretreatment line: hot alkaline degreasing, twin industrial acid pickling baths to strip scale, phosphating to create an anti-corrosive crystalline conversion barrier, followed by ultra-pure water neutralization rinses. Components then enter an automated dust-free electrostatic booth where thermoset polyester-epoxy powder resin is cured at 180°C to 200°C. The resulting finish achieves a uniform dry film thickness of 60 to 90 microns, passing 500-hour ASTM B117 salt spray tests, which is indispensable for coastal distribution hubs in the Middle East, Southeast Asia, and South America.
Why Global Logistics Engineers Partner With Our Factory
Direct from our Guangzhou manufacturing facility to regional hub ports worldwide, we control every milestone across conceptualization, structural analysis, continuous manufacturing, and export clearance.
Autonomous Manufacturing
A dedicated 30,000 m² heavy-machinery production complex in Guangzhou ensures unified quality control over raw slit coil, roll forming, welding, and automated surface curing.
Certified Global Compliance
Traceable CE mark certification (No. 2435-CPR-8605159), ISO 9001:2015 Quality Management certification, and RoHS coating safety approvals for international civil defense reviews.
Free 3D & CAD Layouts
In-house racking architects develop tailored 2D AutoCAD configurations, 3D warehouse renderings, and stress-deflection calculations aligned with your forklift turning radii within 24 hours.
Containerized Packing
All beams, upright trusses, and accessories are systematically bundled with heavy-gauge poly-strapping, edge protectors, and numbered steel crate packs designed for rapid forklift devanning.
Future Procurement Trends in Industrial Pallet Racking
How supply chain automation, high land acquisition costs, and sustainability mandates are transforming racking procurement over the 2026–2030 cycle.
Semi-Automation & Radio Shuttle Densification
Procurement teams are shifting away from conventional wide-aisle static layouts toward high-density 4-way radio shuttle systems. Shuttle systems dramatically slash required forklift operating corridors while elevating cubic space efficiency from 45% up to 85%, mitigating recurring warehouse HVAC energy expenditures.
Cold Chain & Extreme Temperature Resilience
With booming international food logistics and biopharma hubs, pallet racks must withstand sub-zero cold room environments down to -30°C. Standard steel exhibits severe ductile-to-brittle transitions under cold storage. Future procurement mandates structural steel with certified Charpy impact toughness ratings at cryogenic levels.
Seismic-Engineered Baseplates & Heavy Column Protectors
In accordance with updated global building codes, static racking bids now specify non-linear dynamic seismic modeling. Procurement models integrate heavy-duty wrap-around polymer or fabricated structural angle column protectors to absorb repeated MHE (Material Handling Equipment) kinetic impacts.
3. Technological Transformation of China's Heavy Racking Export Sector
Historically viewed primarily as low-cost structural steel converters, top Chinese heavy-duty pallet rack manufacturers have fundamentally transformed their industrial profile over the past decade. Today, advanced Chinese facilities compete directly with Tier-1 European and American racking systems through robotic weld stations, multi-station automated roll-forming lines with inline laser measurement, and enterprise-grade design calculation suites.
Key technological advancements driving modern production include:
- Continuous CNC Roll-Forming Trains: Advanced lines feature up to 24-28 progressive rolling passes. This gradual cold forming produces ultra-precise upright columns without creating micro-fissures or tensile embrittlement along the profile corners.
- Robotic Beam-End Connector Welding: Box beams and stepped beams are welded to 3-claw or 4-claw connector lugs using precision robotic multi-axis MIG welding stations, guaranteeing total penetration welds and eliminating human fatigue defects.
- Environmental Powder Coating Formulations: Lead-free, VOC-free TGIC and epoxy polyester powders provide superior impact resistance against heavy pallet scraping while conforming with rigorous international environmental guidelines.
This technical evolution allows international buyers—ranging from 3PL logistics corporations in Dubai and Dammam to manufacturing distribution facilities across Europe and the Americas—to procure direct-from-source systems that carry full structural certifications at highly advantageous capital expenditure benchmarks.
Need an Engineered Pallet Racking Layout for Your Facility?
Submit your warehouse AutoCAD drawings, pallet dimensions, unit loads, and ceiling clearances. Our senior structural engineers deliver a full 2D CAD floor plan, 3D structural rendering, and certified price quotation within 24 hours.
Inquire NowFrequently Asked Questions on Industrial Pallet Rack Sourcing
Authoritative answers addressing load engineering, export container packing, installation oversight, and international compliance standards.
How do you calculate the maximum safe working load (SWL) for heavy-duty pallet rack beams?
What is the difference between Q235B and Q355B steel in heavy-duty racking fabrication?
How are heavy pallet racking components packaged to prevent damage during ocean container transport?
Can your factory provide installation support and structural drawings for local building permit approvals?
What critical parameters are required to receive a customized 3D warehouse layout and quote?
How does your electrostatic powder coating handle humid coastal climates and cold storage rooms?
Optimizing Your High-Bay Logistics Infrastructure
Investing in heavy-duty industrial storage racks represents a long-term capital commitment impacting daily operational efficiency, warehouse crew safety, and inventory throughput velocity. Partnering directly with an established Chinese manufacturer eliminates intermediary trading markups, ensures direct communication with qualified structural engineers, and guarantees full metallurgical traceability from virgin steel coils to installed storage bays.