 CE Certified
Enterprise Sourcing Portfolio
High-Performance Pallet Racking & Industrial Storage Modules
Precision-formed from certified Q235B and Q355B structural steel, our storage configurations undergo automated electrostatic epoxy-polyester powder coating and finite-element structural validation for maximum payload safety.
CE Certified
 Commercial
 Rapid Assembly
 Selective Access
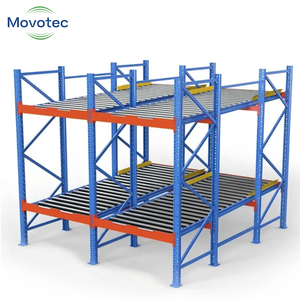 Dynamic FIFO
 Anti-Corrosion
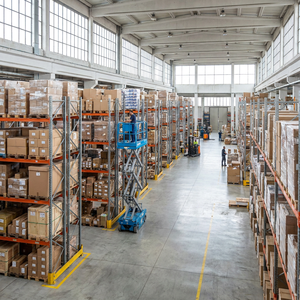
 Up to 3000kg/Level
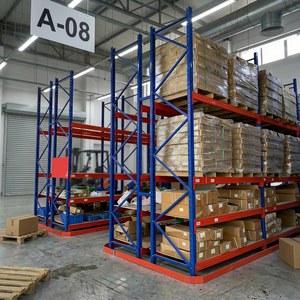
 Standard Selective
Engineering Whitepaper Analysis
The Technical Anatomy of Modern Pallet Shuttle Racking Systems
Moving beyond conventional static storage, semi-automated Radio Pallet Shuttle systems combine deep-lane structural steel channels with autonomous robotic carriers, achieving up to 85% volumetric space utilization.
Kinematics & Carrier Dynamics
The radio pallet shuttle platform employs brushless DC servomotors paired with multi-axis LiDAR and optical encoders. Capable of carrying payloads up to 1,500 kg at speeds of 0.8 to 1.1 m/s (laden), the shuttle operates on galvanized guide rails that serve as both precision tracks and structural load-bearing horizontal members.
- Acceleration control with zero load shifting
- Bidirectional obstacle detection sensors (IP65)
- Automatic low-battery homing routines
Structural Profile Metallurgy
Unlike conventional cold-formed light sections, deep shuttle lanes demand upright frames fabricated from certified high-tensile Q355B cold-rolled steel coils. High-precision continuous roll-forming lines punch upright holes at exact 50mm or 75mm pitches with zero cumulative tolerance error across 16-meter continuous vertical spans.
- Strict compliance with EN 15512 and RMI MH16.1
- Custom omega upright sections up to 140mm width
- Seismic floor anchoring with chemical expansion anchors
Thermal & Cold Storage Engineering
Cold chain logistics represents the highest capital-expenditure sector in warehousing. Our cold-store radio shuttles feature internal thermal resistance heaters, low-temperature resistant lubrication, and sealed LiFePO4 lithium batteries rated down to -30°C, eliminating condensation faults when traversing temperature zones.
- Pre-heating battery management system (BMS)
- Hot-dip galvanized rails resisting frost-thaw cycles
- Continuous 8-to-10 hour shifts per single fast charge
Storage Architecture Technical Comparison
Evaluating volumetric density, operational forklift travel requirements, and SKU accessibility across dense storage topologies.
| System Architecture | Space Utilization | Forklift Operating Mode | Throughput Speed | FMCG/Batch Fit | Structural Collision Risk |
|---|---|---|---|---|---|
| Pallet Shuttle System (Semi-Auto) | 80% - 88% | Aisle-Front Only (Never Enters Lane) | High (Up to 45 Pallets/hr/Lane) | Optimal for FIFO & LIFO | Near Zero (External Entry) |
| Drive-In / Drive-Through Racking | 65% - 75% | Deep Bay Driving Inside Racks | Low (Forklift slow maneuvering) | Strict LIFO (Drive-In) | High (Frequent upright impact) |
| Gravity Roller Flow Racking | 70% - 80% | Separate Inbound & Outbound Aisles | Moderate (Gravity dependent) | Strict FIFO Only | Moderate (Brake maintenance needed) |
| Push-Back Nested Cart Racking | 60% - 70% | Aisle Front (Forklift pushes against carts) | Moderate (2-6 pallets deep) | LIFO Only | Moderate (Cart rail wear) |
| Selective Pallet Racking | 35% - 45% | Every Aisle Requires Forklift Clearance | High (100% immediate selectivity) | Ideal for Multi-SKU Low Volume | Low to Moderate (Aisle guards used) |
Strategic Procurement Horizons
Emerging Technology Trends in Pallet Shuttle Logistics
Global supply chains are transitioning from single-tier mechanization to fully autonomous ecosystems. Procurement directors must anticipate the structural and digital shifts defining warehouse infrastructure through 2035.
1. Migration to 4-Way Multi-Directional Shuttles
While 2-way shuttles move along straight horizontal lanes, the next procurement cycle is heavily favoring 4-Way Pallet Shuttles. Equipped with dual-wheel sets, these units traverse both longitudinal and transverse cross-aisles, switching vertical tiers via integrated reciprocating elevators.
This eliminates dedicated forklift lifting, transforming standard high-bay warehouses into full-density AS/RS cube storage without human intervention.
2. WMS/WCS Handshake via 5G & Industrial Wi-Fi 6
Future-proof procurement demands seamless communication between warehouse management systems (WMS) and shuttle fleets. Early radio remotes are being replaced by industrial Wi-Fi 6 / private 5G mesh networks.
Shuttles report real-time telemetry including battery cycle health, pallet weight distribution, travel speed, vibration spikes, and exact lane coordinates directly to cloud digital twins for predictive maintenance.
3. Supercapacitor & Wireless Induction Charging
Traditional battery swapping introduces downtime and battery room footprint overhead. The latest automated shuttle systems incorporate supercapacitor power modules and rail-integrated charging stations.
The shuttle recharges automatically in seconds during pallet drop-off and pickup cycles, enabling 24/7 continuous duty cycles without battery degradation across extreme temperature environments.
Direct Manufacturing Authority
Why International Engineering Firms Partner with HEDA Shelves
Headquartered in Guangzhou with over two decades of precision manufacturing, our vertically integrated plant controls every stage from raw steel slitting to robotic pre-assembly testing.
Certified Metallurgy
Grade A Cold-Rolled Steel Coils
We source prime certified steel from top-tier domestic mills. All coils undergo yield tensile strength testing and elongation validation before roll-forming, ensuring zero micro-fracturing along continuous profiles.
Surface Treatment
10-Stage Pickling & Phosphating Line
Components pass through automatic chemical degreasing, acid pickling, rust removal, and zinc phosphating before epoxy electrostatic powder coating, guaranteeing exceptional corrosion resistance in humid, coastal, and harsh climates.
Digital Engineering
Free 2D CAD & 3D BIM Layout Simulation
Our in-house team of structural engineers delivers full warehouse space layouts, structural calculation reports, and 3D visual renderings, ensuring compliance with local building codes, NFPA sprinkler rules, and Civil Defense approvals.
Global Traceability
CE & ISO 9001:2015 Verified Compliance
Our production operates strictly under CE Certificate (No. 2435-CPR-8605159), ISO 9001:2015 (No. 18624Q00169R0M), and RoHS environmental standards, providing complete quality tracking from raw batch to container stowage.
Freight Optimization
Container-Optimized Heavy Export Packing
Beams, uprights, and guide rails are bundled in custom protective steel strappings with color-coded bundle tags matching installation diagrams. Cargo is balance-loaded for rapid unloading at international maritime ports.
Regional Support
Extensive Middle East & Global Port Reach
Active deliveries across major logistics hubs including Jebel Ali (UAE), Dammam and Jeddah (Saudi Arabia), Khalifa, Hamad (Qatar), Shuwaikh (Kuwait), as well as key hubs across Europe, Africa, and Southeast Asia.
Technical Procurement Knowledgebase
Frequently Asked Questions on Pallet Shuttle Sourcing
Essential engineering, floor slab, structural, and fire compliance guidelines for warehouse directors and EPC contractors.
What concrete slab tolerances are required for shuttle racking?
Pallet shuttle systems require concrete slab flatness conforming to DIN 18202 (Table 3, Line 4) or ACI 117 standards. Typical requirements mandate floor leveling within ±3mm over a 2-meter straightedge. Excessive deflection or unlevel joints can cause carrier rail misalignment and sensor triangulation errors.
How does the system ensure NFPA fire sprinkler compliance?
High-density shuttle racks create massive volumetric pallet blocks. Under NFPA 13 regulations, longitudinal and transverse flue spaces (typically 150mm) must be preserved. We engineer dedicated vertical riser drops and in-rack sprinkler channels to ensure uniform water distribution without obstructing carrier movement.
Can a single radio shuttle handle mixed pallet dimensions?
Standard shuttles accommodate standard Euro pallets (800x1200mm) and ISO/GMA industrial pallets (1000x1200mm). For non-standard pallets or varied overhangs, carriers can be equipped with optical pallet-edge sensors and adjustable wheelbases to prevent bottom-deck deflection jams on guide rails.
What is the typical battery lifespan and charging protocol?
Our LiFePO4 batteries deliver 2,500 to 3,000 full charging cycles before capacity drops below 80%. A standard 3-hour fast charge provides 8 to 10 hours of continuous heavy-cycle transit. Each system is delivered with dual hot-swappable battery packs per shuttle to ensure non-stop multi-shift warehouse productivity.
How are damaged or malfunctioning shuttles retrieved from deep lanes?
Every installation includes a manual or motorized mechanical recovery trolley. In the rare event of a carrier motor or battery fault inside a 40-pallet deep lane, the recovery trolley locks onto the shuttle's recovery bracket, releasing brake tension and allowing safe retraction back to the access aisle.
What export documentation and inspection protocols are supported?
We provide full factory test certificates, raw material mill test certificates (MTC), third-party inspections (SGS, TUV, BV), SASO/SABER certificates for Saudi Arabia, and complete CE Declaration of Conformity documents along with step-by-step 3D assembly manuals.
Transform Your Warehouse Volumetric Efficiency Today
Consult directly with our structural engineering team. Submit your building architectural CAD drawings, pallet dimensions, and throughput targets to receive a free custom layout design, structural load calculation, and factory-direct quotation within 24 hours.