Featured Heavy-Duty & Dynamic Storage Racking Solutions
Engineered in compliance with ISO 9001:2015, FEM 10.2.02, and CE EN15512 structural safety standards. Explore our field-tested systems optimized for maximum pallet density, rapid picking cycles, and floor space utilization.
Guangzhou HEDA Shelves: Engineering Trust, Precision & Global Scale
Established in 2001, Guangzhou HEDA Shelves Co., Ltd. has grown from an industrial precision fabrication workshop into an international logistics equipment enterprise. With over two decades of technical advancement, our manufacturing base delivers custom intralogistics systems worldwide.
Full In-House Roll Forming & Punching
Every gravity flow upright frame and horizontal beam is shaped using multi-station cold rolling lines. Automated CNC punching guarantees beam pitch accuracy within ±0.2mm, delivering structural alignment essential for smooth gravity track inclines.
Corrosion-Resistant Surface Chemistry
Prior to electrostatic coating, all components undergo a strict multi-stage chemical pretreatment: degreasing, ultrasonic cleaning, acid pickling, and phosphating. This guarantees salt-spray resistance over 500 hours, perfect for coastal ports and humid cold rooms.
Certified Compliance & Quality Control
Fully certified under ISO 9001:2015 (Certificate No. 18624Q00169R0M), CE (EN15512), and RoHS directives. Every raw steel batch from certified Tier-1 mills (Q235B, Q355B) undergoes spectroscopic material verification and tensile testing before production.
Physics, Load Kinematics & Design Principles of Gravity Flow Racks
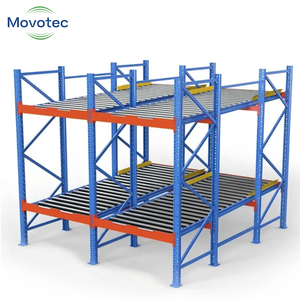
Gravity flow racking operates on the pure conversion of potential energy into kinetic energy. Achieving high throughput while preventing pallet runaway, roller jamming, or dynamic impact damage requires exact calculation of slope, braking resistance, and component selection.
Calculated Slope Gradient (α)
The standard incline angle (α) for heavy industrial pallet flow lanes ranges between 2.5% to 4.0% (approx. 1.5° to 2.3°). Lighter carton flow tracks require 3.5% to 5.0% gradient. Insufficient slope causes pallets to stall along the lane, while excessive incline accelerates momentum beyond the absorption thresholds of end stops.
Centrifugal Speed Controller Rollers
To eliminate unchecked acceleration over deep storage lanes (10 to 25 pallets deep), indirect or direct planetary brake rollers are engineered at intervals of one pallet pitch. These centrifugal mechanisms govern pallet speed at a safe 0.15 to 0.30 m/s regardless of pallet weight variance.
Automatic Pallet Separator Systems
Line pressure accumulates exponentially at the pick face. For a 15-pallet lane, residual hydraulic backpressure can exceed 15,000 kg. Mechanical foot-release separators physically decouple the front pick pallet from the queue, allowing forklifts to lift the leading pallet without friction binding or line surging.
Technical Comparison: Dynamic Storage Racking Configurations
Comprehensive evaluation for warehouse planners comparing capital expenditure, operational efficiency, and spatial optimization.
| Storage Architecture | Rotation Logic | Floor Area Utilization | Forklift Travel Time | Stock Turnover Index | Cold Store Suitability |
|---|---|---|---|---|---|
| Gravity Flow Pallet Rack | Strict FIFO | 80% – 85% | Lowest (Separate Aisles) | Ultra-High (Perishables/FMCG) | Exceptional (Cuts Energy Loss) |
| Push Back Racking | LIFO (Last-In, First-Out) | 65% – 75% | Moderate (Single Aisle) | Medium-High (Multi-SKU) | High |
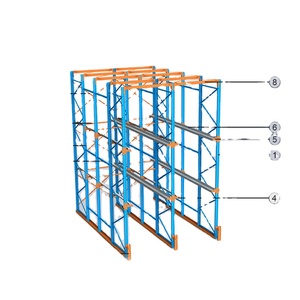
| Drive-In / Drive-Through | LIFO (Rarely FIFO) | 60% – 70% | High (Forklift Enters Rack) | Low-Medium (Homogenous) | High (Risk of Upright Impact) |
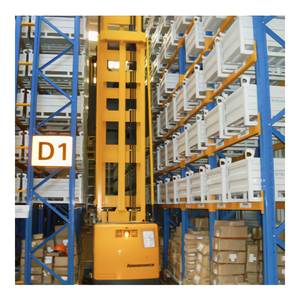
| Very Narrow Aisle (VNA) | Selective (100% Access) | 50% – 60% | Medium (Requires Turret Truck) | Variable (High Vertical Reach) | Moderate |
| Radio Shuttle System | FIFO or LIFO | 80% – 90% | Low (Automated Carriage) | High (Continuous Deep Lane) | High (Requires Lithium Battery Care) |
Future Procurement Trends for Global Supply Chain Directors
Global logistics operations face rising industrial land prices, high electricity tariffs, and tighter ESG mandates. Procurement strategies for dynamic gravity flow storage systems are evolving toward four distinct paradigms.
Sub-Zero Cold Chain Integration
Thermal contraction and ice condensation in -30°C freezer facilities cause unhardened rollers and bearings to freeze. Procurement contracts now demand low-temperature synthetic lubricants, hermetically sealed stainless roller bearings, and pre-galvanized track assemblies that operate without lubricant seizure.
Total Cost of Ownership (TCO)
Global supply chain managers are shifting from lowest-bid purchase orders to 10-year lifecycle TCO models. Heavy-duty cast steel track end protectors, reinforced entry guides, and dual-flanged brake rollers substantially decrease warehouse maintenance stoppages and forklift collision downtime.
Digital Twin & 3D CAD Validation
Enterprises require certified structural simulation before steel stamping begins. At HEDA Shelves, finite element analysis (FEA) validates upright stress deflection curves under maximum simulated seismic load conditions, floor slab pressure ratings, and sprinkler flue clearances.
ESG-Compliant Steel Sourcing
Traceability of low-carbon green steel and compliance with RoHS paint finishing standards are becoming mandatory in European and North American logistics tenders. Factory-direct audits ensure our electro-deposition and powder recovery systems deliver 98% material utilization.
Technological Development Trends in Dynamic Gravity Racking
The intersection of automated mobile robotics (AMRs), digital warehouse execution systems, and sensor technology is redefining how gravity flow systems operate in modern omnichannel distribution centers.
Hybrid AMR & AGV Pick-Face Interfacing
Modern gravity flow lanes are no longer limited to manual counterbalanced forklift interfaces. High-precision laser-guided AGVs and autonomous reach trucks require millimeter-accurate pallet presentation at discharge ends. Advanced optical sensors, precision centering guide rails, and dampened mechanical stops are integrated into lane discharge faces to allow automated robotic end-effectors to pick pallets smoothly without positional misalignments.
Smart IoT Velocity Dampening & Sensors
Emerging gravity roller systems feature self-powered kinetic micro-generators embedded inside speed controller rollers. These rollers harvest energy from passing pallet motion to power wireless IoT nodes that report roller RPM, ambient temperature, bearing wear, and line blockages back to the warehouse management system (WMS), enabling true predictive maintenance before jams occur.
High-Density Carton Flow Pick-to-Light
For split-case fulfillment and piece-picking operations, carton flow systems are transitioning into fully digital picking shelves. Clip-on LED light bars, weight-sensing track dividers, and e-ink lane labels guide order pickers in real time, increasing picking rates from 120 lines per hour to over 450 lines per hour while maintaining 99.98% inventory accuracy.
Frequently Asked Questions: B2B Wholesale Gravity Flow Racking
Everything procurement executives, logistics architects, and facility directors need to know about engineering specs, testing protocols, shipping parameters, and installation support.
What engineering variables are required to calculate the correct gravity flow slope and roller configuration?
How does HEDA Shelves ensure quality control and international structural safety compliance?
Can gravity flow pallet racking handle non-standard wooden pallets or plastic skids?
What is the difference in operational cost between Gravity Flow Racks and Radio Shuttle Systems?
What packaging and container stuffing methods are used to prevent transit damage during ocean freight?
Do you provide engineering design, CAD floor plans, and installation guidance abroad?
Ten-Stage Precision Manufacturing Workflow
Our 30,000 m² Guangzhou production facility operates under strict process controls to guarantee dimensional accuracy, structural safety, and long-lasting durability.
01. Raw Material Verification
High-tensile hot-rolled steel coils from Tier-1 mills are inspected for chemical composition, yield stress, and dimensional thickness tolerances.
02. Precision Steel Slitting
CNC slitting lines decoil and shear master coils into exact band widths with burr-free edges, preparing stock for continuous roll-forming.
03. Automated CNC Punching
High-speed presses punch teardrop, diamond, or hex upright pitch holes with pitch variance kept strictly within ±0.2 mm.
04. Continuous Cold Roll Forming
24-pass precision roll forming stands progressively shape complex upright profiles and step beams to prevent residual structural stress.
05. Robotic Welded Joints
Beam connectors, baseplates, and track brackets are joined using automated multi-axis robotic MAG welding for deep penetration and clean bead finishes.
06. Roller Track Assembly
Galvanized steel rollers, sealed low-noise bearings, and speed controller cylinders are assembled and bench-tested under load.
07. Acid Pickling & Phosphating
Steel passes through a 7-tank chemical pre-treatment bath to strip scale and deposit an anti-corrosive phosphate conversion coating.
08. Electrostatic Powder Coating
Non-toxic epoxy-polyester thermoset powder is electrostatically applied and cured in 200°C tunnels to form a resilient, scratch-resistant finish.
09. Full Pre-Shipment Inspection
Our QA engineers verify weld integrity, film thickness (60–90µm), hole centerlines, and assembly fit before approving packaging.
10. Export Packing & Loading
Components are strapped into labeled bundles with protective wrap and timber blocking to ensure damage-free multi-modal ocean transit.