Engineered Racking Uprights & Heavy-Duty Storage Systems
From single-bay selective pallet racks to automated ASRS high-bay columns, explore our export-grade cold-formed upright profiles built to EN 15512, RMI, and FEM structural integrity standards.
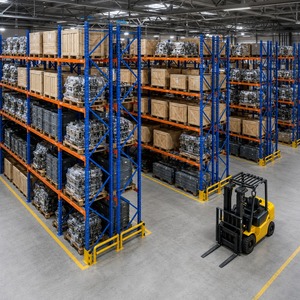
Selective Pallet Racking System Steel Storage Rack Q235B Heavy Duty Warehouse Industrial Racks Powder Coated
Standard 75mm/50mm pitch omega uprights, certified 5,000kg bay load ratings, electrostatic powder finish resistant to industrial wear.
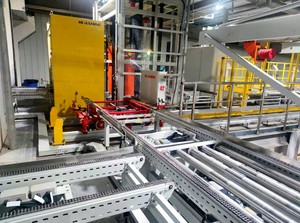
HUASHINE INTELLIGENT Warehouse Automatic Storage Racking ASRS System Chemical Nylon, Carbon Black Industry
Continuous roll-formed high-bay uprights reaching 30m+ with strict deflection limits designed for crane tolerances and heavy pallet turnover.
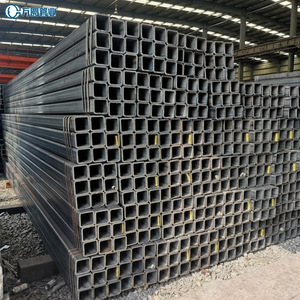
EN 10219 S355J0H Cold Formed Load Bearing Carbon Steel SHS RHS Structural Hollow Section For Warehouse Pallet Racking System
High-tensile European standard hollow structural sections engineered for seismic resistance and demanding heavy cantilever and mezzanine uprights.
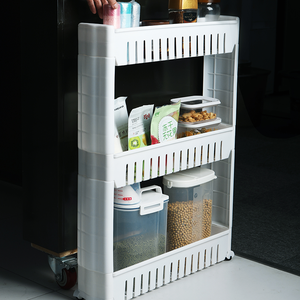
Slim Slide Out Storage Tower Rack Mesh Rolling Organization Serving Cart Shelf for Narrow Spaces Gap Storage Rack
Precision-fabricated micro-gap steel shelving unit utilizing cold-formed tubular uprights for maximum payload efficiency in confined picking bays.
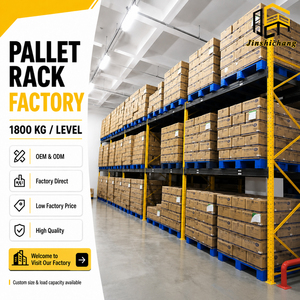
3000KG Heavy Duty Pallet Rack Warehouse Storage Shelves Units Powder Coating Steel Racking System
Heavy profile 90mm/100mm/120mm upright sections engineered to support up to 3000kg uniformly distributed loads per beam level safely.
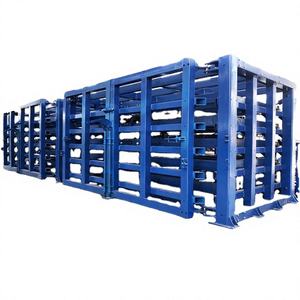
Adjustable Movable Steel Selective Pallet Rack with 2 Layers ESd Protection Electric Mobile Racking System for Industrial Use
Reinforced column base junctions with specialized anti-static grounding and motorized guided rail interfaces for cleanroom electronics logistics.
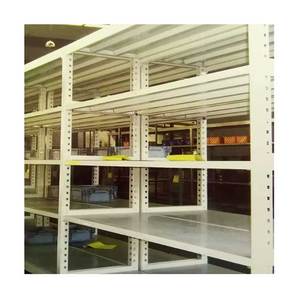
Herschel Warehouse Heavy Duty Industrial Steel Fabric Roll Storage Warehouse Pallet Racking
Heavy punched upright frames fitted with custom cantilever saddles and cylindrical axle cradles for textile, paper, and coil inventory.
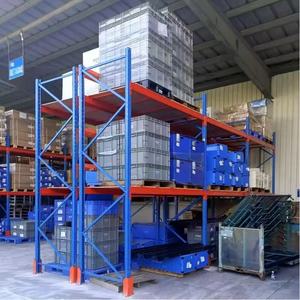
Heavy Duty Metal Pallet 250-1000kg Bulk Stackable Equipment Garage Warehouse Storage Rack Powder Coating
Removable corner post upright design with cupped stacking feet for flexible bulk storage without permanent floor anchoring.
Metallurgical Architecture & Structural Mechanics of Racking Uprights
The warehouse racking upright (column) is the ultimate load-bearing backbone of any storage system. Understanding section modulus, residual cold-forming stress, and punch-hole stress concentration is essential for safe warehouse operations.
1. Steel Grade Selection: Q235B vs. Q355B vs. S355J0H
The yield strength ($R_e$) and ultimate tensile strength ($R_m$) of raw hot-rolled or cold-rolled strip determine the load capacity of the formed column. While commercial shelving relies on basic Q195/Q215 steel, heavy industrial racking demands Certified Q235B (minimum yield 235 MPa) or high-strength Q355B / S355J0H (minimum yield 355 MPa).
Higher yield grades provide superior resistance against localized crushing under extreme axial compression while allowing thinner wall thicknesses that reduce containerized shipping deadweight without sacrificing factor of safety ($SF \ge 1.5$ per FEM 10.2.02).
Our uprights undergo strict tensile elongation tests ($A \ge 22\%$) to guarantee seismic energy dissipation during dynamic earthquake loading.
2. Cold Roll-Forming Bends & Section Modulus
A flat steel coil does not gain strength until engineered bends are induced. Our multi-station continuous roll-forming lines execute between 11 to 13 progressive cold bends to shape our proprietary Omega ($\Omega$) profile. Each bend creates work-hardening at the corners, increasing local yield strength by up to 15%.
This multi-rib geometry maximizes the second moment of area ($I_x$ and $I_y$), drastically reducing effective buckling length ($KL/r$) and preventing torsional-flexural buckling under combined axial and eccentric pallet loads.
Reinforced return flanges prevent open-throat spreading under maximum beam moment reactions.
3. Punching Geometry & Stress Concentration Factor
Uprights require perforations along their length to allow beam height adjustability. Common patterns include teardrop, butterfly, diamond, and hexagonal slots at 50mm, 75mm, or 76.2mm (3-inch) pitch. However, punching creates localized residual stresses.
Our CNC tooling uses precision-ground dies with controlled cutting clearance (8% of sheet thickness) to prevent micro-fissures around the aperture edges. This keeps the fatigue notch factor under rigorous control during cyclic warehouse loading.
Cumulative perforation pitch error is strictly constrained within $\pm 0.15\text{ mm}$ over a continuous 12-meter upright length.
| Profile Model | Section Depth × Flange (mm) | Material Thickness | Steel Grade Spec | Max Frame Capacity (kg) | Standard Pitch Type | Optimal Application |
|---|---|---|---|---|---|---|
| HD-UP80 | 80 × 60 × 2.0 | 1.8 – 2.0 mm | Q235B / Cold-Rolled | 8,500 kg | 50 mm European / 75 mm | Standard Selective / E-Com |
| HD-UP90 | 90 × 70 × 2.0 | 2.0 – 2.3 mm | Q235B / Q355B | 14,000 kg | 75 mm / 76.2 mm Teardrop | Heavy Industrial Logistics |
| HD-UP100 | 100 × 70 × 2.5 | 2.0 – 2.5 mm | Q355B High-Tensile | 19,500 kg | 50 mm / 75 mm | Drive-In & Radio Shuttle |
| HD-UP120 | 120 × 95 × 2.5 | 2.3 – 3.0 mm | Q355B / S355J0H | 26,000 kg | 75 mm Heavy Pitch | ASRS Automated High-Bay |
| HD-UP140 | 140 × 95 × 3.0 | 2.5 – 3.2 mm | S355J0H Structural | 34,000 kg | Custom Pitch (ASRS) | Seismic High-Rack Silos |
4. Chemical Pretreatment & Anti-Corrosion Surface Engineering
Unprotected mild steel corrodes quickly in harsh industrial environments such as coastal logistics hubs, high-humidity food distribution plants, and chemical manufacturing yards. At HEDA Shelves, uprights do not simply get sprayed; they pass through an automated 10-stage immersion and spray pretreatment line consisting of alkaline degreasing, twin-stage water cascade rinsing, pickling for mill-scale removal, and micro-crystalline zinc phosphating.
The phosphate conversion layer bonds at the molecular level, creating a 1.5–2.5 g/m² conversion coating that anchors the subsequently applied thermosetting epoxy-polyester powder (80–120 microns DFT). This finishing system achieves over 500 hours of continuous neutral salt spray resistance (ASTM B117) with cross-hatch adhesion meeting Grade 0 (ISO 2409). For cold stores operating at down to -30°C or outdoor storage yards, hot-dip galvanized (HDG) columns according to ISO 1461 are provided.
Future Procurement & Technological Trends in Warehouse Uprights
Global warehouse development is undergoing structural transformation driven by warehouse automation, carbon compliance, and high freight costs. Buyers must consider several key engineering trends when sourcing upright profiles.
ASRS Integration & Tighter Tolerances
As automated storage and retrieval systems (ASRS) replace manual reach trucks, upright column deflection criteria are tightening from standard manual warehouse limits ($L/200$) to strict robotic crane standards ($L/400$ to $L/600$). Splice connections must maintain plumbness within 1:1000 across vertical heights exceeding 24 meters.
Decarbonization & Green Steel (CBAM Readiness)
International procurement teams in Europe and North America increasingly require Environmental Product Declarations (EPD). Upright manufacturing is moving toward electric arc furnace (EAF) scrap-based steel coils and low-VOC powder curing ovens, lowering embodied carbon metrics to comply with the EU Carbon Border Adjustment Mechanism.
Modular Nesting for Container Space Optimization
Rising maritime container shipping rates demand smarter volumetric nesting. Next-generation upright cross-sections feature tapered rear flanges and optimized frame bracing geometries. This allows upright frames to be shipped knocked-down (KD) and nested compactly, boosting 40HQ container payload efficiency by up to 28%.
Seismic Performance & Baseplate Dissipation
Global seismic codes (such as Eurocode 8 and ASCE 7) now mandate energy-dissipating ductile baseplate assemblies. Modern upright engineering integrates high-ductility anchor slots, cold-formed reinforcing boots, and sacrificial crumple zones that absorb forklift impact kinetic energy without initiating column progressive collapse.
IoT-Enabled Structural Health Monitoring (SHM)
High-bay logistics centers are beginning to incorporate fiber-optic strain gauges and RFID load-deformation sensors into critical upright slots. These smart columns stream real-time stress data to Warehouse Management Systems (WMS), warning operations managers about uneven bay overloading or impact damage.
High-Yield Thin-Walled Cold-Formed Steel Sections
Advancements in roll-forming software enable 14+ bend profiles using ultra-high-yield steels (up to 420–550 MPa). This achieves identical moment resistance to traditional hot-rolled structural steel sections while reducing steel weight per pallet position by 15–20%.
Our 10-Step In-House Racking Manufacturing Ecosystem
From raw coil verification to export-secure bundling, every manufacturing stage is monitored inside our 30,000 m² factory in Guangzhou, China.

Raw Steel Verification
Chemical composition analysis & ultrasonic flaw detection on certified Q235B/Q355B coil batches.

Precision Slitting & Cut
Automated uncoiling, leveling, and high-speed rotary shearing with laser-guided edge tracking.

CNC Column Punching
Continuous mechanical power presses stamp 50mm/75mm/76.2mm perforation matrices at ±0.1mm tolerance.

Cold Bending Forming
Specialized hydraulic brake bending for heavy-duty baseplates, column protectors, and frame brackets.

Omega Roll Forming
11–13 progressive forming stands shape the high-inertia omega profile with zero micro-cracking.

Automated De-burring
Rotary wire brush and abrasive polishing remove laser slag and sharp perforation edges for safe manual assembly.

Robotic MIG Welding
Panasonic robotic stations ensure deep penetration welds on baseplate anchors and beam connector claws.

Pickling & Phosphating
Automated chemical immersion tanks eliminate scale, oil, and rust, establishing an anti-corrosion barrier.

Electrostatic Coating
Swiss Gema powder application guns deposit 80–120μm polymer film cured in a 200°C tunnel oven.

QC & Seaworthy Packing
CMM dimensional audit, bundle strapping, corrugated edge protection, and container stowage tracking.
Built to Global Building & Storage Codes
In international tender projects, safety compliance and valid certificates are critical requirements. HEDA Shelves holds traceable certifications verified by third-party testing organizations:
-
CE Certification (EN 1090-1 / EN 15512)
Certificate No. 2435-CPR-8605159 confirms factory production control for structural steel components.
-
ISO 9001:2015 Quality Management System
Registration No. 18624Q00169R0M (valid through 2027-06), auditing raw material traceability and manufacturing quality.
-
RoHS & Heavy-Metal Surface Non-Toxicity
Powder coating films are verified free of lead, cadmium, and hexavalent chromium, making them safe for food and pharmaceutical warehouses.
Frequently Asked Questions on Racking Uprights Sourcing
Clear engineering and commercial answers to help procurement managers, EPC contractors, and rack distributors import directly from China.
What steel grades are used for HEDA Shelves upright columns, and can you supply test certificates?
How do you calculate safe upright frame capacity and buckling resistance?
Are your upright perforation patterns compatible with existing European or American teardrop racks?
- North American Teardrop: 2-inch punch spacing with 1-inch adjustability, compatible with major US brands.
- European 50mm Pitch: Compatible with Dexion, Stow, and Jungheinrich beam connector brackets.
- Standard 75mm / 76.2mm Pitch: The international benchmark for high-load industrial selective racking.
What anti-corrosion protection do you recommend for cold storage or coastal logistics hubs?
How are upright frames packed for export containers to prevent transit deformation?
What information is needed to receive an engineering layout and quotation?
Upgrade Your Warehouse Infrastructure with Certified Upright Columns
Consult with our structural engineering team today to review your load requirements, optimize steel tonnage, and request our complete engineering catalog and sample packs.