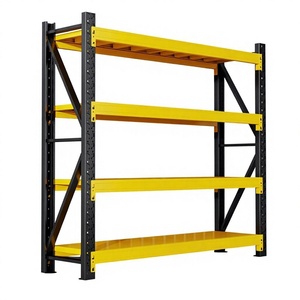
Engineered Warehouse Racking & Dynamic Storage Systems
Certified industrial structural racks, high-density live pallet flow lanes, and radio automated platforms manufactured to strict European FEM and American RMI mechanical standards.
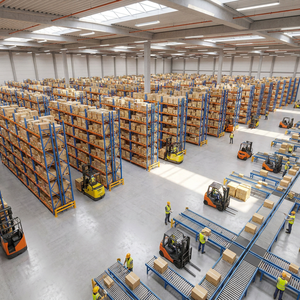
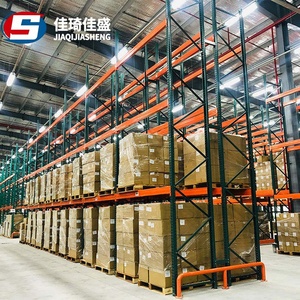
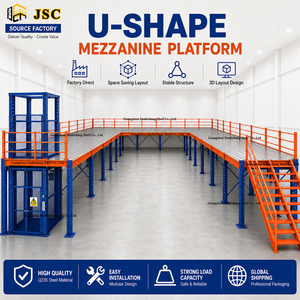
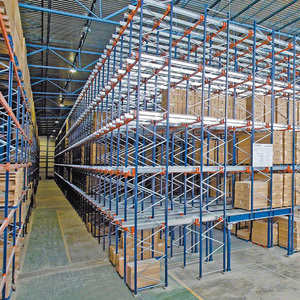
Engineering Excellence in Case Flow & Dynamic Live Storage
In modern high-velocity fulfillment facilities, material handling efficiency is dictated by the physics of the picking face. Case flow rack systems (also referred to as carton flow racks) utilize inclined roller tracks or dynamic skate-wheel beds to transport cartons, totes, and split cases from the rear loading aisle to the front picking face via natural gravitational acceleration. This design creates an absolute physical separation between replenishment traffic and order-picking personnel, effectively eliminating operational bottlenecks and cutting overall picker transit time by up to 75% compared to static selective shelving.
As a premier OEM & ODM manufacturer operating over 30,000 square meters of precision fabrication infrastructure since 2001, our facility engineers bespoke case flow racking frameworks tailored to fluctuating package dimensions, fragile payloads, and extreme operating ambients. Utilizing premium Q235B cold-rolled structural steel, robotic continuous gas-shielded seam welding, and computerized ten-stage surface pretreatment lines, our rack assemblies are calculated to resist high dynamic impact while maintaining sub-millimeter track straightness over decades of continuous cycle loading.
Strict FIFO Rotation Assurance
By leveraging dedicated rear charge lanes and frontal retrieval planes, our case flow modules guarantee flawless First-In, First-Out (FIFO) inventory cycling—an essential engineering mandate for pharmaceutical, food and beverage, and perishable cosmetic logistics.
Drop-In OEM Track Modularity
Designed with adaptable clip brackets compatible with standard teardrop, structural channel, and European hook-profile uprights. Roller tracks feature self-lubricating nylon or high-durability steel axles rated for up to 150 kg/m dynamic rolling mass.
Environmental Surface Integrity
High-adhesion thermo-setting electrostatic polyester powder coating cured at 200°C over zinc-phosphated substrates guarantees peak corrosion prevention, passing 500-hour salt spray testing for humid or sub-zero refrigeration conditions.
Technological Paradigms & Future Procurement Trends (2025–2030)
The warehousing landscape is shifting rapidly from static storage density metrics to micro-fulfillment agility and dynamic throughput velocity. Procurement directors and supply chain integrators must anticipate technological shifts when deploying case flow capital investments:
1. Pick-to-Light (PTL) and Autonomous Mobile Robot (AMR) Convergence: Traditional standalone case flow racks are transitioning into integrated pick faces. Modern OEM specifications demand integrated extruded aluminum mounting channels for light indicators, sensor arrays, and pick-to-voice interfaces. Forward-thinking layouts now feature custom low-profile front stops optimized for robotic gripper arms and mobile piece-picking robots operating alongside human selectors.
2. Hybrid High-Density Dynamic Mezzanine Systems: Real estate constraints across major urban logistics gateways (such as Dubai JAFZA, Riyadh Logistics Zone, and North American distribution hubs) have driven demand for multi-tier case flow mezzanines. By suspending carton flow lanes within structural steel catwalk mezzanines, facilities achieve 300% storage expansion without requiring horizontal real estate development.
3. Ultra-Low Friction Universal Skatebeds: Rather than fixed-width dual plastic tracks, universal full-width aluminum skatebeds are quickly becoming the industry standard. They allow instant reconfiguration for variable SKU packaging—from polybags and flimsy corrugated boxes to rigid plastic crates—without the mechanical re-spacing of lane dividers.
Factory Infrastructure: Custom OEM/ODM Capabilities
Backed by over two decades of heavy steel fabrication expertise, our manufacturing campus operates multiple continuous roll-forming lines, automated punching matrices, and robotic welding stations. We eliminate trading intermediaries, offering global buyers direct engineering oversight, certified material traceability, and mill-direct price structures.
Traceable Metallurgy
Exclusively cold-formed high-tensile Q235B and Q355B structural coil sourced from certified mills, accompanied by full chemical analysis and mechanical tensile test reports.
Global Certifications
Fully compliant with international safety and quality standards: CE Certificate (No. 2435-CPR-8605159), ISO 9001:2015 Quality Management, and RoHS-certified non-toxic finishes.
Free Engineering & 3D
Complimentary 2D CAD structural layouts, picking zone workflow calculations, and photometric 3D rendering delivered within 24 hours of receiving site blueprints.
Export Container Pack
Automated strapping, moisture-barrier wrapping, heavy-gauge steel dunnage, and part-level numbered bundles to streamline customs clearance and local assembly.
Procurement & Technical Engineering FAQ
What is the standard incline gradient for case flow lanes?
Standard case flow beds are installed with a pitch between 2.5% and 5% (approximately 15 to 30 mm of drop per linear meter). The precise angle is calibrated based on carton base material, tote friction coefficients, payload mass, and whether pneumatic speed controllers or impact separators are integrated.
Can OEM case flow beds retrofit existing pallet racks?
Yes. Our universal mounting clips and load beam adaptors allow our gravity flow beds to bolt directly into pre-existing selective pallet racking, industrial shelving, or drive-in frames from nearly any international racking manufacturer without structural drilling.
What are the minimum order quantities (MOQ) and production lead times?
As a direct mill fabricator, standard configurations feature flexible trial MOQs starting at single-bay test units, while full container project quantities typically dispatch within 15 to 22 business days following design approval.
How do you guarantee rack safety and Civil Defense approval?
All structural drawings feature verified static calculations, aisle clearance envelopes, and flue-space layouts compliant with local municipal civil defense codes, seismic criteria, and NFPA/EN sprinkler clear space guidelines.