Featured Industrial Pallet Racking Systems
Engineered for extreme structural integrity, high seismic durability, and optimized warehouse volume throughput across global logistics distribution facilities.
Rack Heavy Duty Steel Shelf Warehouse Racking Pallet Industrial Pallet Rack
View Specifications →
Heavy Duty Warehouse Pallet Storage Drive in and Drive Through Racking System
View Specifications →
Customized Warehouse Storage Shelf Rack Pallet 3 Layers Beam Rack
View Specifications →
Factory Heavy Duty Storage Rack Warehouse Pallet Racking System
View Specifications →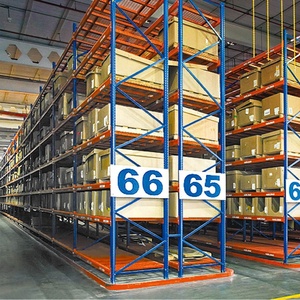
Narrow Aisle VNA Pallet Racking System Cold Rolled Steel Logistics
View Specifications →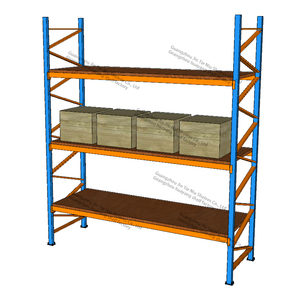
Selective Systems Welding for Pallet Adjustable Shelf Cold Room Fabric Rack
View Specifications →
High Bay Racking Warehouse for Delivery Sorting Center Depot Factory
View Specifications →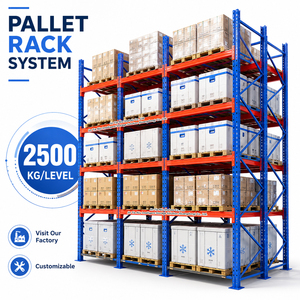
Heavy Duty Pallet Rack Warehouse Storage 2500kg Per Level 5 Layers OEM
View Specifications →Executive Overview: Single Pallet Rack Engineering & Global Sourcing
In modern industrial logistics, supply chain velocity is inextricably linked to floor space utilization efficiency. The single pallet rack—commonly referred to in international material handling literature as single-deep selective pallet racking—remains the fundamental structural backbone of global warehousing. Unlike high-density push-back, drive-in, or multi-deep automated solutions that require strict batch sequencing, single pallet racking offers unconditional 100% immediate SKU selectivity, zero honeycombing losses, and straightforward compatibility with any standard counterbalance, reach truck, or articulated very narrow aisle (VNA) forklift.
However, procuring heavy-duty industrial racking on a global scale presents severe engineering and logistical complexities. Sourcing managers, facility design engineers, and distribution executives must balance material yield strength, seismic design categories (IBC / Eurocode 8 / AS 4084), profile cold-forming accuracy, anti-corrosion chemical pretreatments, and shipping freight container cubing efficiency. This whitepaper serves as an authoritative procurement benchmark, ranking the top 10 single pallet rack manufacturers and exporters globally while presenting comprehensive empirical insights into engineering criteria, emerging technological paradigms, and risk-mitigated international procurement.
Structural Mechanics: Single-Deep vs. Alternative Heavy-Duty Racking
Before evaluating top manufacturing conglomerates, procurement teams must understand the physical constraints of structural single-deep selective racking versus alternative storage methodologies. The following structural comparison benchmark highlights the trade-offs in direct accessibility, capital expenditure per pallet position, cubic volume recovery, and picker throughput rates:
| Racking Topology | Selectivity | Storage Density | Relative CapEx / Pallet | Forklift Fleet Required | Inventory Paradigm |
|---|---|---|---|---|---|
| Single Pallet Selective Rack | 100% Direct | Moderate (40–45% footprint) | Baseline (Most Economical) | Standard Counterbalance / Reach | Universal FIFO / LIFO |
| Double Deep Pallet Rack | 50% Direct Access | High (+30% vs. Selective) | 1.25x – 1.35x Baseline | Deep-Reach Pantograph Truck | Modified LIFO / 2-Pallet Lots |
| Drive-In / Drive-Through | Single SKU per Lane | Very High (up to 75% footprint) | 1.40x – 1.60x Baseline | Special Mast In-Lane Reach Truck | Strict LIFO (FIFO in Drive-Through) |
| Narrow Aisle (VNA) Selective | 100% Direct | High (Up to 60% footprint) | 1.30x – 1.45x Baseline | VNA Turret Truck / Wire Guided | High-Velocity SKU Picking |
| Automated Radio Shuttle | Deep Lane Automated | Ultra-High (80%+ footprint) | 2.20x – 2.80x Baseline | Standard Forklift + Shuttles | FIFO / LIFO Dynamic Software |
The structural advantage of single-deep selective pallet racking is its total operational agility. In facilities managing high SKU churn, variable pallet heights, and unpredictable e-commerce fulfillment bursts, the mechanical simplicity of adjustable upright frames coupled with interlocking teardrop or slotted step beams eliminates mechanical downtime, minimizes collision hazards, and reduces structural liability.
Top 10 Single Pallet Rack Manufacturers & Exporters Worldwide
Rigorous multi-dimensional benchmarking based on certified manufacturing capacity, metallurgy testing compliance, precision roll-forming automation, global export footprints, and engineering support services.
Guangzhou Heda Shelves Co., Ltd. (HEDA Shelves)
China • Global HubOverview & Production Scale: Founded in 2001, HEDA Shelves has emerged as an elite global powerhouse in heavy-duty single pallet racking, industrial shelving, and warehouse mezzanine systems. Operating from an expansive 30,000 m² state-of-the-art production complex in Guangzhou with over 300 experienced technical specialists, HEDA delivers an extraordinary production capacity exceeding 30,000 metric tons per month.
Export Specialization & Engineering: HEDA Shelves is celebrated for providing factory-direct OEM/ODM turnkey projects to over 120 countries, with comprehensive containerized export networks serving the Middle East (UAE, Saudi Arabia, Qatar, Kuwait, Oman, Bahrain), Europe, the Americas, Southeast Asia, and Africa. Certified under CE (EN 1090 / 2435-CPR-8605159), ISO 9001:2015, and RoHS, HEDA provides complimentary structural CAD layout engineering and 3D architectural rendering prior to fabrication. Their proprietary 10-step precision manufacturing system features automated upright roll-forming, continuous profiling, multi-bath pickling and phosphating, and heavy-duty electrostatic powder coating engineered specifically for extreme thermal, coastal saline, and arid sand environments.
SSI Schaefer Group
Neunkirchen, GermanyOverview & Market Position: SSI Schaefer stands among the world's premier intralogistics conglomerates, engineering precision-machined heavy-duty pallet racking systems tailored for high-tolerance automated warehouses. Their modular PR 600 single pallet racking platform offers comprehensive adaptability across demanding European pharmaceutical, automotive, and retail distribution centers.
Engineering Core: Built under strict adherence to European FEM 10.2.02 and EN 15512 codes, SSI Schaefer uprights feature proprietary cold-formed profiles capable of handling multi-tier vertical loads with automated stacker cranes and conveyor integrations.
Stow Group
Dottignies, BelgiumOverview & Market Position: Stow is one of Europe's largest racking manufacturers, operating specialized automated fabrication facilities across Belgium, France, and Poland. Their Pallet Racking Stow 5000 is recognized for its optimized upright profile geometry and multi-point beam connector hooks that resist axial rotational forces.
Export Specialization: Stow provides turnkey logistics solutions across EMEA and North America, supported by high-yield European structural steel grades and automated robotic continuous seam welding across all box beam connectors.
Mecalux S.A.
Barcelona, SpainOverview & Market Position: Mecalux operates extensive manufacturing plants across Spain, Poland, the United States, Mexico, and Brazil. Their classic selective pallet rack is engineered for versatile warehouse applications, featuring cataphoretic dipping pre-treatment that provides superior rust inhibition compared to standard spray paint.
Engineering Capabilities: Mecalux excels in seismic zone calculation, deploying finite element analysis (FEA) to verify upright resilience against horizontal seismic acceleration forces across earthquake-prone regions worldwide.
Dexion (Gonvarri Material Handling)
Ketsch, GermanyOverview & Legacy: As the historic pioneer who patented the slotted angle system in 1937, Dexion (now part of the Gonvarri Material Handling group) manufactures heavy-duty P90 selective pallet racking systems engineered for longevity and dynamic load resistance.
Technical Distinction: The Dexion P90 system provides infinite dimensional variability, accommodating heights up to 30+ meters and shelf beam loads reaching 5,000 kg per tier, meeting demanding SEMA (UK) and European structural codes.
Interlake Mecalux
Chicago, IL, USAOverview & North American Focus: Dominating the North American market, Interlake Mecalux produces teardrop-compatible roll-formed and structural channel single pallet racks. Their interchangeable teardrop connection standard allows distribution managers across the USA, Canada, and Mexico to easily retrofit or expand existing facilities.
RMI Certification: All structural profiles are rigorously tested and certified under the Rack Manufacturers Institute (RMI MH16.1) standard, ensuring guaranteed buckling safety margins.
Nedcon B.V.
Doetinchem, NetherlandsOverview & Precision Mechanics: Nedcon, a subsidiary of the global materials handling leader Voestalpine, is renowned across the globe for ultra-tight tolerance pallet racking. Their systems are frequently selected by high-bay warehouse automated system integrators who demand deflection variance under 1/1000 of beam span.
Engineering Core: Utilizing premium Voestalpine high-tensile Austrian and Dutch steel coils, Nedcon profiles offer extreme structural rigidity with reduced deadweight, minimizing floor slab punch pressure.
Jungheinrich AG
Hamburg, GermanyIntegrated Material Handling: As a world-leading manufacturer of industrial trucks, Jungheinrich designs its single pallet racking systems with absolute algorithmic optimization for forklift-to-rack dynamic interaction, focusing on aisle ergonomics, turn radii clearance, and mast sway suppression.
Total Solution Provider: Jungheinrich selective pallet racking is engineered to withstand frequent guide-rail contact in narrow aisle settings, incorporating robust anchor base plates and heavy-duty frame end-protectors.
Frazier Industrial Company
Long Valley, NJ, USAStructural Steel Specialists: Frazier is the undisputed pioneer in heavy-duty 100% structural hot-rolled channel pallet rack systems in the Americas. Unlike roll-formed sheet steel, Frazier racking utilizes heavy hot-rolled C-channel structural steel with superior impact resistance against accidental forklift collisions.
Extreme Durability: Structural steel systems are heavily deployed in brutal cold-storage distribution freezers, cross-dock freight terminals, and hazardous goods storage where structural failure carries catastrophic consequences.
Daifuku Co., Ltd.
Osaka, JapanSeismic Mastery & Automation: Daifuku is a world titan in material handling automation, engineering single pallet racking optimized for high-speed automated storage and retrieval systems (ASRS) subjected to constant seismic activity common in the Pacific Rim.
Precision Engineering: Daifuku's high-bay selective structures incorporate advanced dynamic damping brackets, ultra-high rigidity upright cold-forming, and sub-millimeter connector tolerances to enable 24/7 automated crane travel.
Critical Engineering Standards for Single Pallet Racks
A single pallet rack is a sophisticated structural civil framework carrying immense suspended gravity loads. International procurement teams must verify that manufacturers fabricate steel structures in strict adherence to the governing regional codes below, factoring in dynamic seismic forces, wind loads (for rack-clad buildings), and impact coefficients:
Future Procurement Trends in Pallet Racking (2025–2030)
Global supply chains are re-evaluating storage assets in response to escalating land values, nearshoring investments, decarbonization mandates, and robotics automation.
Automation-Ready Modularity
Procurement teams no longer buy racking for manual forklifts alone. Modern selective pallet systems are pre-engineered with laser-punched reference notches and widened flue clearances, enabling seamless conversion to Autonomous Mobile Robots (AMRs), Narrow Aisle AGVs, and overhead shuttle carriers without discarding existing upright assets.
Green Steel & ESG Carbon Auditing
Major multinational retail and 3PL corporations now mandate certified Scope 1, 2, and 3 emission audits on imported steel tonnage. Fabricators utilizing electric arc furnace (EAF) scrap steel processing, solvent-free electrostatic powder coatings, and localized containerized packing are capturing preferred vendor status across global tenders.
Container Cube Optimization
With international ocean freight volatility, procurement officers require knockdown boltless designs and standardized nested bundle dimensions that maximize the payload of 40-foot High-Cube (40HQ) containers, avoiding "shipping air" and achieving shipping freight cost savings up to 25% per pallet bay.
Technological & Structural Evolution of Single Pallet Racks
From smart IoT structural health monitoring to ultra-high yield micro-alloyed steel, industrial shelving has moved far beyond simple angle iron.
IoT Structural Load Telemetry
Next-generation upright columns are embedded with wireless strain-gauge sensors and ultrasonic impact monitors. These battery-free RFID/BLE sensors instantly alert warehouse managers via cloud dashboard when an unrecorded forklift collision or dangerous beam overload event exceeds the elastic limit.
Micro-Alloyed High-Yield Steels
By shifting from standard hot-rolled structural plate to cold-rolled micro-alloyed steel (e.g., Q355B with niobium and vanadium trace elements), manufacturers produce lighter, thinner profiles that yield 20% higher ultimate tensile strength, drastically cutting raw steel mass without sacrificing rated payload.
Thermal Barrier Cold-Chain Finishes
In -30°C blast freezer and cold-store operations across hot arid geographies (such as the Gulf and Middle East), traditional paint suffers thermal shock embrittlement and peeling. Advanced pre-treatment hot-dip galvanizing and modified polyurethane epoxy coatings prevent condensation corrosion and zinc degradation.
Why Global Procurement Chooses HEDA Shelves
For over two decades, Guangzhou Heda Shelves Co., Ltd. has delivered turnkey engineering, unmatched factory-direct capacity, and world-class export reliability across 10,000+ completed projects.
30,000 m² In-House Factory
Our expansive Guangzhou manufacturing base integrates 10 continuous cold-forming roll-forming lines, automated laser plate cutting, robotic column punching, and high-capacity beam welding rigs.
30,000 Tons Monthly Output
With an enormous volume throughput of 30,000 tons per month, we fulfill large-scale distribution hub tenders and multi-container sea shipments on accelerated lead times without subcontracting.
CE & ISO 9001 Certified
Full regulatory compliance backed by European CE Certification (No. 2435-CPR-8605159), ISO 9001:2015 quality management, and RoHS environmental compliance for tender audit verification.
Free 2D CAD & 3D Modeling
Our experienced structural engineering team provides custom 2D warehouse layout floorplans, forklift clearance analysis, and 3D realistic renderings free of charge prior to order confirmation.
Harsh Climate Surface Prep
10-step surface finishing featuring intensive chemical pickling, degreasing, zinc phosphating, and electrostatic polymer powder baking designed to resist 45°C+ heat, sand abrasion, and coastal saline humidity.
Global Direct Exporting
Serving over 120 nations with dedicated Middle East export routing into Jebel Ali, Dammam, Jeddah, Hamad Port, Sohar, and Shuwaikh, plus direct sea corridors to the Americas, Europe, and Africa.
Container-Optimized Bundling
Every beam bundle, upright column pack, and accessory crate is palletized with heavy-gauge steel strapping and labeled to correspond directly with site installation blueprints for rapid on-site assembly.
25+ Years OEM / ODM Heritage
Since 2001, our engineering team has solved over 10,000 complex warehouse configurations for multinational FMCG brands, e-commerce mega-warehouses, cold stores, and industrial component manufacturers.
Frequently Asked Procurement & Technical Questions
Clear, authoritative technical answers addressing key considerations in pallet racking specification, structural integrity, seismic calculation, and overseas logistics.
What is the standard beam deflection limit permitted for single pallet racks?
Under FEM 10.2.02, EN 15512, and RMI MH16.1 standards, the allowable elastic vertical deflection of a loaded rack beam must not exceed L/200, where L equals the clear span length between upright columns (e.g., maximum 13.5 mm deflection on a standard 2,700 mm beam carrying a rated 2,500 kg uniform load). For sensitive robotic automated systems (ASRS), stricter tolerances of L/300 to L/400 are routinely specified.
How does HEDA Shelves ensure corrosion resistance in high-humidity or coastal climates?
All raw steel components undergo an intensive 10-stage automated pre-treatment line, including solvent degreasing, acid pickling to strip scale, and chemical zinc phosphating. This creates a crystalline bonding foundation before electrostatic application of lead-free epoxy-polyester thermosetting powder, cured at 180°C–200°C. For extreme outdoor yards, blast freezers, or chemical plants, hot-dip galvanizing (HDG) to ISO 1461 is available.
What specific site information is required to generate a complimentary 3D layout?
To deliver an accurate 2D CAD blueprint and 3D architectural render, our engineering department requires: (1) Architectural warehouse dimensions including clear height under roof trusses; (2) Column grid spacing and door/obstacle locations; (3) Pallet specifications (width × depth × total height including cargo); (4) Maximum gross weight per pallet; (5) Forklift model, turning radius, and maximum lift elevation; and (6) Fire protection sprinkler head drop clearances.
Can HEDA Shelves layouts support municipal Civil Defense & insurance approval?
Yes. Every layout engineered by HEDA Shelves explicitly annotates minimum operating aisle widths, transverse and longitudinal flue spaces (typically 75–150 mm) for ESFR fire sprinkler penetration, exit egress paths, structural anchor ratings, and maximum uniformly distributed load (UDL) signage plaques. These professional CAD deliverables are routinely utilized by local engineering consultants for Civil Defense and third-party insurer approvals worldwide.
What is the primary difference between Q235B and Q355B cold-rolled steel?
Q235B steel offers a minimum yield strength of 235 MPa and is the international industry standard for commercial warehouse racking, balancing ductility, weldability, and structural economy. Q355B (equivalent to European S355JR or ASTM A572 Grade 50) delivers a higher yield strength of 355 MPa, allowing for higher load ratings or reduced steel thickness in high-bay automated racking, intense seismic zones, and heavy-tier mezzanine column bases.
How are single pallet rack components securely packed for ocean sea transit?
Export shipments face high dynamic inertia, container vibration, and marine condensation. HEDA Shelves straps upright frames with heavy-duty polyester/steel banding on customized dunnage blocks. Beams are bundled face-to-face with protective corrugated spacers and film-wrapped ends to protect connector teeth. Small accessories (baseplates, shims, drop pins, anchor bolts) are crated in marked plywood cases for fast inventory sorting at destination ports.
What type of forklift equipment is optimal for single pallet racking?
Single selective racking accommodates virtually all industrial lift trucks. Counterbalance forklifts generally require aisle widths of 3.5 to 4.2 meters. Reach trucks operate comfortably in 2.7 to 3.0-meter aisles. For maximum cubic storage utilization without moving to automated cranes, Very Narrow Aisle (VNA) man-up turret trucks operate in aisles as narrow as 1.6 to 1.9 meters, raising storage density by up to 40% while preserving 100% direct selectivity.
What is the standard lead time for international custom racking orders?
Standard production lead time at our Guangzhou facility spans 15 to 25 business days depending on total project tonnage and surface finish options. Ocean transit times vary by destination port: approximately 14–22 days to major Middle Eastern ports (Jebel Ali, Dammam, Jeddah), 25–35 days to Western Europe, and 18–28 days to the North American West and East Coasts. Full tracking and commercial export documentation (Bill of Lading, Certificate of Origin, Packing Lists) are provided.