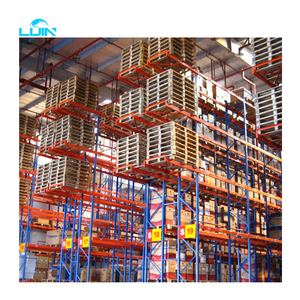
LIJIN Heavy Duty Commercial Industrial Long Span Shelving
Adjustable multi-tier medium-to-heavy shelving featuring modular step beams and galvanized or steel shelf panels. Ideal for manual pick faces and automotive spare parts.
Direct from our 30,000 m² Guangzhou production facility: cold-rolled Q235B/Q355 structural profiles engineered to withstand seismic shear, intensive forklift impacts, and extreme ambient humidity.
Adjustable multi-tier medium-to-heavy shelving featuring modular step beams and galvanized or steel shelf panels. Ideal for manual pick faces and automotive spare parts.
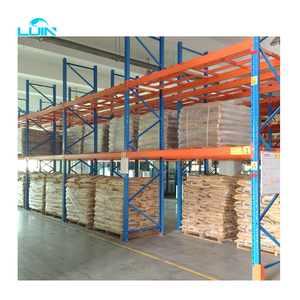
Interlocking beam-to-column connectors with safety lock pins prevent accidental dislodgement from reach trucks and forklifts in high-throughput distribution hubs.
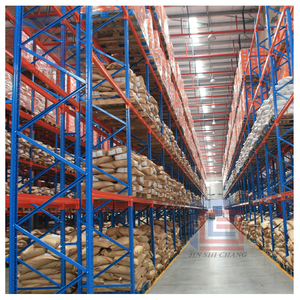
The gold standard for total inventory accessibility. Ensures immediate 100% SKU selection without honeycomb losses, compliant with FEM 10.2.02 international guidelines.
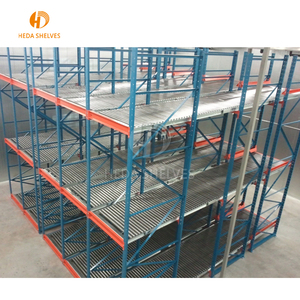
Integrated aluminum or plastic skate-wheel roller tracks operate via gravity feed. Minimizes picker travel distances by 40% along lean manufacturing lines and assembly areas.
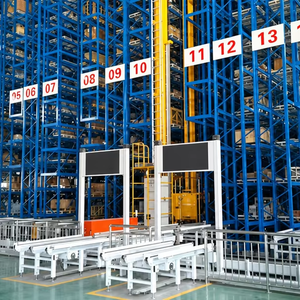
Engineered for autonomous stacker cranes and AMR integration with structural height capabilities exceeding 30 meters. Millimeter-accurate deflection tolerance guaranteed.
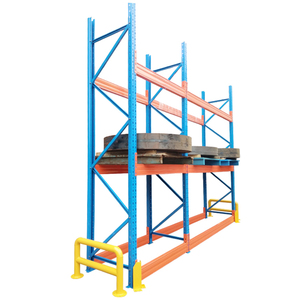
Box-beam and step-beam variants reinforced with cold-rolled upright columns. Fully customizable frame depths and clear span profiles built around specific slab psi loads.
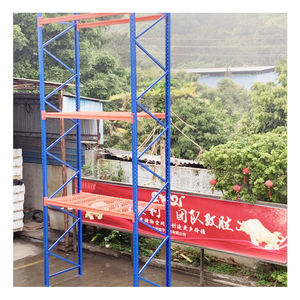
Optimized for third-party logistics (3PL) operations requiring frequent beam level adjustments. Treated with multi-stage zinc phosphate pre-treatment to arrest corrosion.
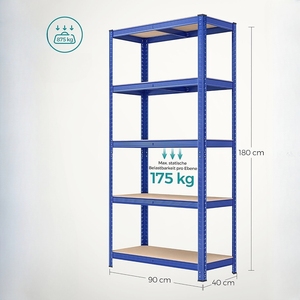
Multiplies usable warehouse vertical footprint by 200%-300%. Integrates structural walkways, safety handrails, pallet gates, and staircase modules without structural expansion.
With over 25 years of specialized mechanical racking calculation, our factory combines advanced in-house robotics, strict metallurgical controls, and Civil Defense approval readiness.
We source only certified prime structural steel coils (Q235B / Q355). Our cold-roll-forming profiles undergo finite element method (FEM) analysis and adhere strictly to CE Certification (No. 2435-CPR-8605159) and ISO 9001:2015 quality regimens, guaranteeing consistent yield strength under static and seismic loads.
To resolve extreme microclimates—including ambient heat exceeding 45°C and severe coastal humidity across Middle Eastern ports (Jebel Ali, Dammam, Jeddah)—our 10-stage processing incorporates chemical pickling, phosphating, and 60-80μm electrostatic powder coatings that exceed salt-spray durability tests.
By cutting out intermediary trading companies, enterprise buyers gain a direct engineering channel for custom hole punching, bespoke frame heights, container-optimized packing schedules, and direct sea transport documentation matching regional Civil Defense approval standards.
An authoritative operational guide analyzing total cost of ownership (TCO), ESG compliance, and the structural convergence of manual racking with robotics.
Procurement directors are rapidly pivoting from low-density floor-stacking to high-bay vertical racking engineered with tight deflection criteria (L/200, L/300) that can accommodate autonomous mobile robots (AMRs) and radio shuttle carts without retrofitting.
Sourcing is shifting from raw tonnage pricing to lifetime damage mitigation. Buyers prioritize high-tensile column shapes with reinforced lower-flange profiles, column base protectors, and factory-certified drop-in beam locks over lower-gauge raw steel.
Supply chain shocks make lead times paramount. Logistics operators seek integrated manufacturers running simultaneous roll-forming, automatic punching, and powder-coating lines capable of outputting 30,000 tons monthly with modular container nesting.
| Storage Architecture Type | Space Utilization | SKU Selectivity | Material Handling Equipment | Optimal Industry Application |
|---|---|---|---|---|
| Selective Pallet Racking | 40% – 50% (Aisle Intensive) | 100% (Instant Direct Access) | Standard Counterbalance / Reach Truck | FMCG, 3PL Warehouses, General Retail |
| Drive-In Racking | 70% – 85% (High Density) | Low (Last-In, First-Out) | Drive-in Forklift with Narrow Mast | Cold Storage, Beverage, Seasonal Stock |
| Gravity Carton / Pallet Flow | 75% – 85% (Dynamic Dense) | High per lane (Strict FIFO) | Forklift Load / Hand or Tugger Pick | Pharmaceuticals, Perishable Foods, Assembly |
| Radio Shuttle Automation | 80% – 90% (Deep Lane Density) | Medium (Automated FIFO/LIFO) | Standard Forklift + Radio Shuttle Cart | Meat Cold Storage, High-Volume Manufacturing |
| Multi-Tier Mezzanine | 200% – 300% (Vertical Multiplier) | 100% Manual Bin Selectivity | Conveyors, Vertical Lifts, Hand Trucks | E-commerce Fulfillment, Auto Parts Distribution |
How engineering evolutions in high-tensile metallurgy, parametric BIM modeling, and automated surface treatments are redefining storage equipment lifespan.
Modern manufacturing now relies on 3D parametric calculation engines. Each project generates exact deflection curves, joint rigidity matrices, and seismic response spectra, enabling architects to seamlessly import IFC/Revit models into civil defense dossiers.
Advancements in multi-station continuous roll-forming lines allow complex cross-sections with 10 to 14 multi-bend stiffening ribs. This maximizes second moment of area (Ix, Iy) while reducing overall steel consumption and freight weight without compromising load ratings.
Eliminating hazardous chemical waste, state-of-the-art silane or zirconium oxide nanotech conversion coatings are superseding traditional heavy phosphating. These nano-layers achieve superior resin cross-linking with powder coats, multiplying weather and chemical resistance.
Technical solutions to the most critical structural, regulatory, and logistics questions asked by project consultants, general contractors, and procurement heads.
To deliver verified 2D CAD engineering plans and 3D FEA stress models, our design team requires: (1) Architectural CAD floor plans indicating clear internal height beneath the roof trusses and column grids; (2) Pallet specifications (width, depth, overall loaded height, maximum gross weight including pallet); (3) Forklift turning radius (AST) and maximum lift mast height; (4) Concrete floor slab thickness and reinforcement specification (psi/MPa capacity); and (5) Local seismic zone coefficients.
Our surface finishing line follows a strict 10-step protocol: chemical degreasing, twin water washings, pickling to remove scale, zinc phosphating (or zirconium nanotech passivation), and automated electrostatic application of high-durability polyester powder coating cured at 180°C–200°C. For unconditioned port facilities or outdoor staging yards, components can be specified in hot-dip galvanized finishes conforming to ISO 1461 standards.
Yes. Every project drawing set details clear flue spaces (longitudinal and transverse) for in-rack fire sprinkler penetration according to NFPA 13 rules, precise aisle clearances for emergency egress, maximum permissible uniform distributed loads (UDL) per pair of beams, and load-plate sign locations. Our engineering documentation provides structural data that consultants submit to local authorities (such as GCC Civil Defense departments).
Our export logistics protocol categorizes components into color-coded and numbered steel-strapped bundles that mirror site erection phases. Uprights are bundled with protective wood dunnage and heavy-duty corner boards to prevent fork chafing. Beams, bracing struts, and footplates are palletized in wooden crates with desiccant packs to prevent marine sweating during long-haul container ocean transport through humid maritime routes.
From mill raw coil certification to export stuffing, our Guangzhou facility maintains complete digital traceability for every steel batch.
Mill test certificate verification, continuous ultrasonic thickness monitoring, laser precision slitting, and computerized high-speed column punching with precision 50mm/75mm tooling dies.
Continuous roll-forming profiles followed by multi-axis robotic welding for beam connectors and baseplates, preventing cold laps and guaranteeing penetration depth along connector joints.
Complete chemical pickling, phosphating, electrostatic spray booth application, high-temperature convection curing, and stringent cross-hatch adhesion and load-deflection QC sign-off.
Connect directly with our senior application engineers. Receive a complete 2D layout proposal, 3D structural rendering, and comprehensive containerized freight quote within 24 business hours.