Featured Industrial Warehouse & Movable Racking Systems
Explore our proven heavy-duty industrial configurations fabricated from premium Q235B and Q355B cold-rolled structural steel, fully customized for maximum volumetric utilization, seismic safety, and rapid global deployment.
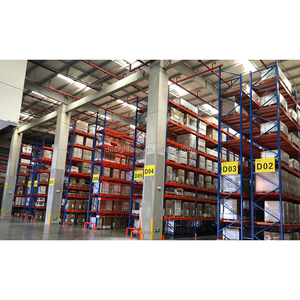
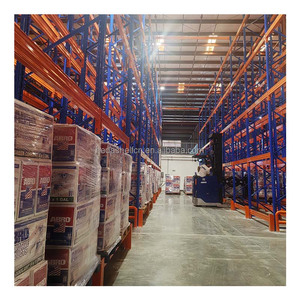 Global Benchmark
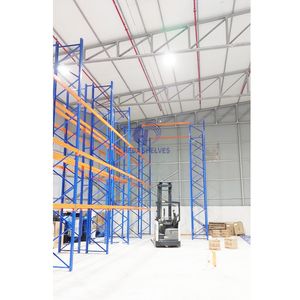
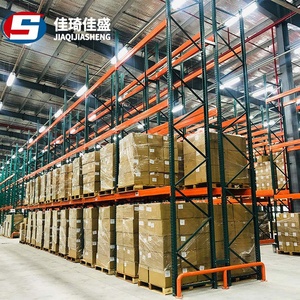 Hybrid Multi-Tier
 Corrosion Defense
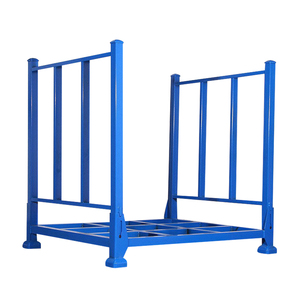 Movable Post Pallet
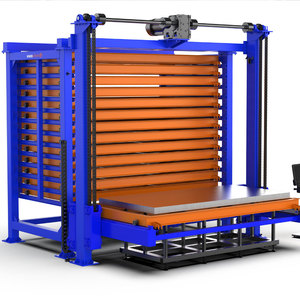
Engineering Movable Racking: Dynamic Footprint Optimization
Traditional static pallet racking systems sacrifice between 50% and 65% of floor surface area exclusively to access aisles. Industrial movable racking systems revolutionize this spatial equation by mounting heavy-duty upright frames onto electromechanical motorized chassis or precision-guided low-friction floor rails.
The Mechanics of Movable Dynamic Bases
A true industrial-grade movable racking system requires structural calculations that balance static dead weight with dynamic kinetic acceleration and sudden deceleration forces. Utilizing dual-flanged steel wheels driven by synchronized helical gear motors, movable bases slide smoothly along recessed floor guide rails embedded directly into the structural concrete slab.
By opening a single aisle on demand via PLC interface, radio remote, or integrated warehouse execution software (WES), an operator unlocks up to 85% to 90% floor space utilization. This eliminates the operational costs of climate-controlling unused cubic volume, making it the premier strategy for cold chains, dry bulk chemicals, and ultra-high-density distribution centers.
- Fail-Safe Optical Safety Curtains: Continuous photo-electric beams across the movable aisles halt base translation instantly upon detection of obstacles or personnel.
- Torque-Balanced Drive Axles: Electronically synchronized wheel drives prevent racking skewing or base binding during heavy asymmetric pallet loading.
- Precision Rail Ground Tolerances: Leveling tolerances calibrated to DIN 18202 Class 3 ensure minimum roll resistance and negligible structural flex over 100,000+ motion cycles.
| Storage Architecture | Floor Space Efficiency | Pallet Selectivity | Seismic & Structural Dynamic Load | Optimal Industry Applications |
|---|---|---|---|---|
| Movable Electric Pallet Racking | 85% – 90% (Ultra High) | 100% On-Demand Aisle Access | Dynamic braking distribution; rigid floor-anchored guidance rails | Cold Storage (-30°C), High-Value Parts, Chemicals, Pharma |
| Standard Selective Pallet Racks | 35% – 45% (Standard) | 100% Instant Immediate Access | Pure static loading; individual bay anchor bolting | High-throughput retail distribution, FMCG, fast-turnover 3PL |
| Radio Shuttle High-Density Racks | 80% – 88% (High Density) | Channel-Dependent (FIFO/LIFO) | High static bay mass; heavy concentrated rail guide load | Beverage warehousing, seasonal produce, raw material buffers |
| Drive-In / Drive-Through Systems | 60% – 70% (Dense) | Restricted LIFO Sequence | High forklift impact risk; cantilever bracket stress | Uniform SKUs, deep cold rooms, slow-rotation staging |
Future Procurement Trends Shaping Global Racking Logistics
Strategic global supply chain procurement is moving beyond simple unit pricing. Modern capital equipment directors evaluate lifecycle durability, environmental compliance, smart warehouse integration, and geopolitical supply chain resilience.
Total Cost of Ownership (TCO) vs. Initial CapEx
Global procurement teams prioritize structural longevity and low maintenance over initial purchasing discounts. Choosing high-yield Q355B steel with automated pre-treatment and electrostatic polymer powder coating reduces corrosion degradation, upright replacement frequencies, and forklift collision downtime by up to 40% over a 15-year facility horizon.
Supply Chain Diversification & Direct-Factory Exporting
Disruptions in regional warehousing hubs have accelerated direct-from-manufacturer sourcing models. Tier-1 buyers bypass intermediary trading agencies to engage certified factories capable of providing in-house structural engineering, custom 3D CAD modeling, and factory-direct shipping container optimization that fits 40HQ container cube limits without structural damage.
Mandatory Regulatory & Seismic Pre-Qualification
Civil defense authorities and commercial property underwriters enforce strict compliance with EN 15512, RMI ANSI MH16.1, and local seismic building codes. Racking tenders now mandate certified finite element analysis (FEA), load distribution schematics, and stamped weld inspection records before container dispatch is authorized.
Technological Innovations in Movable & Automated Racking
Next-generation intralogistics demands hardware and software integration. Discover how mechanical engineering convergence is redefining warehouse throughput, safety telemetry, and energy efficiency.
Autonomous Robotic & AMR Compatibility
Movable and shuttle racking systems are increasingly configured with standardized laser-reflective guidance targets, ultra-flat docking channels, and wireless handshake protocols. This enables direct, human-free pallet handoffs to Autonomous Mobile Robots (AMRs) and automated counterbalanced AGVs.
Eco-Drive Regenerative Braking Architecture
Large-scale motorized movable rack runs incorporate variable frequency drives (VFD) equipped with regenerative deceleration modules. Kinetic energy recovered during deceleration cycles is returned to the facility grid, trimming continuous electrical draw by up to 22% across cold chain logistics facilities.
IoT Load-Sensing & Deflection Telemetry
Advanced upright channels integrate strain-gauge micro-transducers and optical deflection sensors. Real-time telemetry notifies warehouse supervisors of asymmetrical overloading, seismic displacement, or forklift impact stress exceeding structural elasticity thresholds ($L/250$).
Why Global Buyers Trust HEDA Shelves as Their Primary Exporter
Headquartered in Guangzhou, China, Guangzhou Heda Shelves Co., Ltd. has stood at the forefront of heavy-duty industrial racking and modular warehouse fabrication since 2001. We combine massive production scale with precision European engineering standards.
30,000 m² Mega Plant
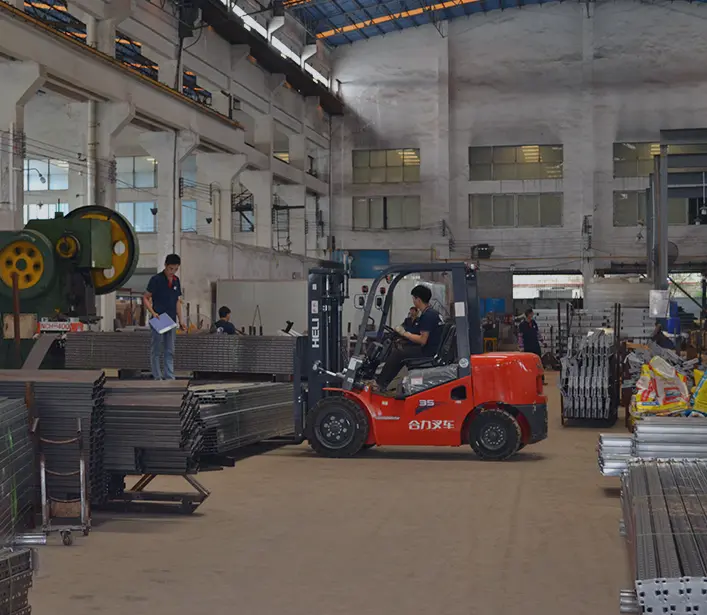
Our centralized manufacturing base houses advanced high-speed continuous roll-forming lines, automated laser-guided punching machines, and robotized gas metal arc welding cells.
Verified Traceable Quality
Certified under CE (Certificate No. 2435-CPR-8605159), ISO 9001:2015 (Certificate No. 18624Q00169R0M), and full RoHS compliance. All raw coil batches undergo mill-test mechanical yield verification.
Free 2D CAD & 3D Modeling
Our technical team of 300+ specialists delivers complete AutoCAD spatial plans, beam deflection calculations, and photorealistic 3D layout renderings prior to project sign-off.
Global Export Packaging
Components are systematically bundled, rust-proof wrapped, and coded to match assembly blueprints directly. Exported cleanly across Jebel Ali, Dammam, Jeddah, Rotterdam, and Los Angeles.
In-House 10-Stage Metallurgical Manufacturing Process
Raw Material QC
Certified high-tensile steel coils tested for tensile strength and yield composition.
Precision Slitting
CNC slitting lines trim coils to sub-millimeter edge tolerances for roll forming.
Auto Punching
Continuous hydraulic stamping of pitch holes (50mm/75mm) along the upright web.
Cold Bending
Multi-roller forming stations fold structural steel into rigid Omega profiles.
Profile Forming
Beam and bracing profile channels calibrated to exact structural depths and lengths.
Polishing & Deburr
Automated shot-blasting removes burrs, scale, and micro-imperfections.
Robotic Welding
CO2 gas shielded robotic arms weld beam connectors and baseplates with zero spatter.
Pickle & Phosphate
Acid pickling and zinc phosphate wash passivate steel against sub-surface oxidation.
Powder Coating
Automated electrostatic epoxy powder line baked at 200°C for superior impact resilience.
Final QC & Pack
Ultrasonic thickness gauge testing, piece-count audit, and container strapping.
Frequently Asked Questions for Warehouse Racking Procurement
Critical engineering, logistics, and compliance considerations clarified by HEDA Shelves' senior structural engineering division.
Ready to Optimize Your Warehouse Cubic Storage Density?
Collaborate directly with HEDA Shelves' technical structural team. Submit your architectural floor plan or storage requirements today to receive a comprehensive CAD layout, 3D rendering, and factory-direct quotation within 24 to 48 hours.