Engineered Heavy-Duty Warehouse Racking Solutions
Precision-manufactured utilizing Q235B and Q355B structural carbon steel. Designed for universal forklift compatibility, maximum volumetric efficiency, and structural safety compliant with RMI and European EN 15512 standards.
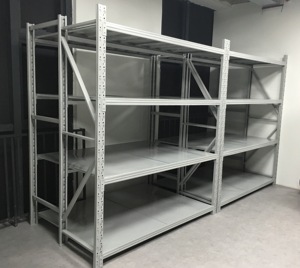
Space Saving Light Duty Steel Selective Pallet Rack 5 Adjustable Multi Tier Large Load Capacity Corrosion Protection Storage
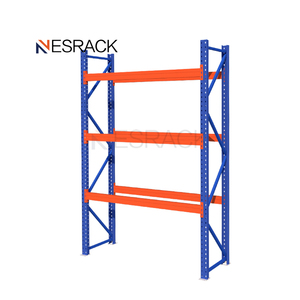
Heavy Duty Pallet Rack Shelving Pallet Racking Dimensions Warehouse Storage Racks Customized Adjustable Steel Q235B Pallet Rack
Bulk Order Tubular Subframe Metal Frames Fabrication Services Crossmember Carrier Pallet Platform Rack
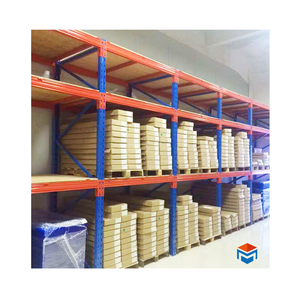
Warehouse Racking System Heavy Duty Warehouse Shelving Solution Metal Adjustable Double Deep Selective Pallet Storage Rack
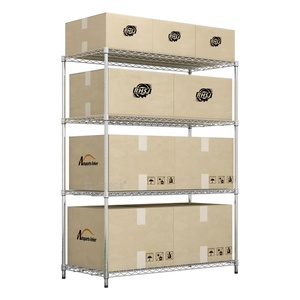
Versatility 4 Tiers NSF Approval Chrome Plated Racking Solid Steel Wire Shelving Storage System for Garage Warehouse
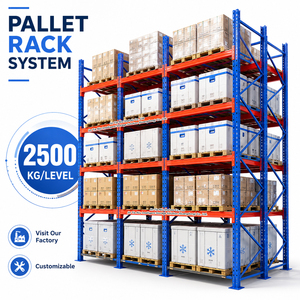
Heavy Duty Pallet Rack Warehouse Storage Racking System 2500kg Per Level 5 Layers OEM Factory
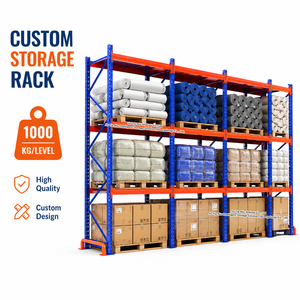
1000KG Warehouse Heavy Duty Pallet Rack Adjustable Storage Racking System Factory Direct
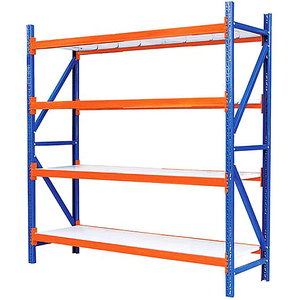
Blue Orange Custom Design Corrosion Protection Medium Duty Storage Racks Boltless Shelving Heavy Duty Shelf
Future Pallet Rack Procurement Trends (2025–2030)
Global supply chain disruptions, urban land scarcity, and rapid automated material handling adoption are forcing warehouse operators to abandon standard commodity racking in favor of precision-engineered structural assets.
Total Cost of Ownership (TCO) vs. CapEx Procurement
Enterprise buyers are transitioning from initial purchase price metrics to lifecycle TCO calculations. Racks fabricated with certified micro-alloyed steel (such as Q355B or ASTM Grade 50) maintain yield strengths under cyclical dynamic impacts, reducing beam sag, joint loosening, and catastrophic collapse hazards over 15 to 20 operational years.
- Lower deflection ratios (exceeding L/200 & L/240)
- Cold-formed upright geometries mitigating forklift torsion
- Extended factory warranties backed by verifiable mill certs
Automation-Ready Tolerances (ASRS & AMR Integration)
Manual forklift operations accept dimensional deviations of ±5mm; automated shuttle systems, Autonomous Mobile Robots (AMRs), and high-bay Automated Storage and Retrieval Systems (ASRS) require strict structural fabrication tolerances within ±1.0mm. Forward-looking procurement demands CNC-punched column profiles compatible with automated laser guidance and shuttle rails.
- Radio-shuttle lane retrofittability
- Continuous roll-formed guide rail integration
- Sub-millimeter floor baseplate anchoring tolerances
Climatic & Corrosive Resilience Engineering
Warehouses across high-humidity coastal trading ports (e.g., Jebel Ali, Dammam, Rotterdam, Singapore) and sub-zero cold-chain hubs face accelerated coating degradation and structural embrittlement. Modern tenders strictly specify multi-stage chemical pretreatment, zinc-iron phosphating, and electrostatic polymer cross-linking exceeding 500-hour ASTM B117 salt spray benchmarks.
- Zero-VOC thermosetting polyester powder coatings
- Hot-dip galvanized (HDG) outdoor subframe integration
- Cryogenic steel formulations eliminating ductile-to-brittle shifts
Technical Evaluation: Traditional Commodity Racking vs. HEDA Engineered Standards
| Engineering Attribute | Standard Commodity Market Racking | HEDA High-Precision Industrial Racks | Operational Impact on Facility |
|---|---|---|---|
| Raw Steel Grade & Yield Strength | Uncertified Q195 / Scrap Mix (Yield ≤ 205 MPa) | Mill-Certified Q235B / Q355B (Yield ≥ 355 MPa) | Prevents catastrophic beam failure under dynamic surge loads |
| Beam Deflection Specification | L / 150 to L / 180 under full static capacity | Strict L / 200 to L / 240 design threshold | Guarantees automated shuttle and pallet jack clearance without sticking |
| Pretreatment & Finishing | Single degreasing wash + air dry painting | Automatic 8-stage pickling, phosphating & powder cure | Eliminates under-film flaking; withstands 95% coastal humidity |
| Punching Precision & Pitch | Manual punch press (±3.0mm pitch variance) | Automated continuous CNC roll-punch (±0.5mm variance) | Perfect beam locking integrity; zero wobble during fast seismic loading |
| Regulatory Code Adherence | Self-declared capacity without stamped proof | CE (2435-CPR-8605159), ISO 9001:2015, EN 15512 | Smooth Civil Defense approvals and commercial property underwriting |
Technological Advancements in Pallet Storage Engineering
Structural engineering has shifted from static empirical rulebooks to dynamic non-linear computational modeling. Discover how advanced computational mechanics and intelligent material sciences are reshaping modern logistics infrastructure.
Finite Element Analysis (FEA) & Dynamic Seismic Verification
Modern high-bay racking systems operate as integrated structural frames. Utilizing advanced ANSYS finite element modeling, HEDA structural engineers simulate localized stress concentrations at the beam-to-column connector teeth under horizontal seismic accelerations (compliant with EN 16681 and RMI standards).
- Dynamic response spectrum modal analysis
- Second-order P-Delta geometric sway calculations
- Multi-claw beam locking clips eliminating unseating risk
Automated Closed-Loop Cold Roll-Forming Lines
Traditional fabricated channels suffer residual stresses and micro-fractures along bend radii. Modern cold roll-forming lines deploy progressive multi-station roll tooling (up to 24 continuous forming stations). This ensures cold work hardening along column profile corners, increasing the effective moment of inertia without adding dead steel tonnage.
- Omega-shaped upright cross-sections with 8 to 12 load-bearing bends
- Optimized slenderness ratios minimizing buckling susceptibility
- Consistent mechanical properties from coil head to tail
Structural Health Monitoring & RFID Asset Tracking
The rise of smart warehousing has introduced sensor-instrumented racking. Micro-strain sensors placed on high-stress baseplates monitor real-time beam overloading and dynamic forklift impact events. RFID tags embedded in upright protectors record inspection cycles, providing facility managers with automated predictive maintenance logs.
- Real-time overload alert telemetry via warehouse WMS
- Collision detection sensors on vulnerable aisle corners
- Automated periodic safety inspection auditing compliance
Why Global Logistics Leaders Partner with HEDA Shelves
Established in 2001, Guangzhou Heda Shelves Co., Ltd. operates as a dedicated one-stop industrial racking designer and manufacturer. With a 30,000 square meter factory, 300+ engineering technicians, and 30,000 tons of monthly capacity, we deliver direct mill advantages worldwide.
Global Regulatory Approvals
Full compliance with CE Certification (No. 2435-CPR-8605159), ISO 9001:2015 Quality Management System (No. 18624Q00169R0M), and RoHS environmental standards for global tender acceptance.
Complimentary 2D/3D Engineering
Our engineering department delivers comprehensive 2D AutoCAD floor plans, 3D structural layouts, forklift turning radius simulations, and Civil Defense fire flue clearance calculations within 24–48 hours.
GCC & Global Port Logistics
Direct factory export packing tailored for overseas maritime logistics. Frequent scheduled container runs to major regional ports including Jebel Ali, Khalifa Port, Dammam, Jeddah Islamic, Hamad, Sohar, and Shuwaikh.
Complete OEM & ODM Customization
Custom beam sections, custom upright hole pitches (50mm / 75mm / 76.2mm), tailored epoxy powder shades (RAL standards), and bespoke heavy mezzanine integration built to your structural slab load limitations.
Certified 10-Stage Precision Manufacturing Workflow
From raw hot-rolled steel coil to containerized export dispatch, every phase is governed by strict ISO-level QA/QC inspection gates.










Frequently Asked Questions by Industrial Racking Buyers
Direct, engineering-backed answers addressing structural design codes, environmental protection, Civil Defense permits, and overseas delivery logistics.
Accelerate Your Warehouse Capacity with Certified Structural Racking
Whether you are commissioning a new regional logistics hub or retrofitting an existing distribution facility, our engineering team is ready to analyze your floor plan and supply custom CAD designs, finite element calculations, and direct factory pricing.