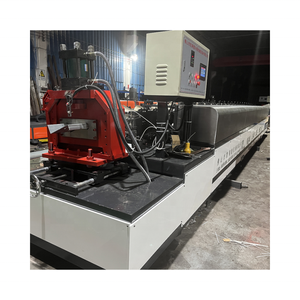
High Quality Shuttle Racking Production Line Bearing Drive-In Storage Motor
Integrated drive-in pallet shuttle line featuring industrial heavy-torque motors, robust guide tracks, and dynamic load-bearing engineering.
View Specifications →Precision-engineered high-density storage platforms configured for heavy payload capacities, severe cold chain environments, and fully automated intralogistics ecosystems.
Integrated drive-in pallet shuttle line featuring industrial heavy-torque motors, robust guide tracks, and dynamic load-bearing engineering.
View Specifications →
Deep-lane radio shuttle configuration optimizing volume utilization up to 85% with high-speed remote channel navigation.
View Specifications →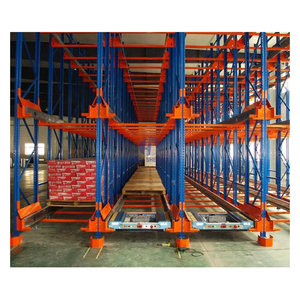
Certified high-tensile structural steel racking tailored for high-throughput automated warehouses with integrated sensor protection.
View Specifications →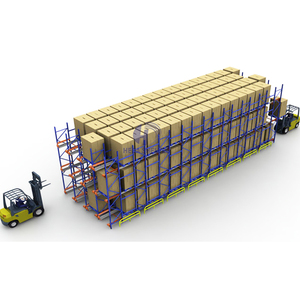
Next-generation multi-directional 4-way shuttle robot allowing lateral and longitudinal lane shifting without forklift intervention.
View Specifications →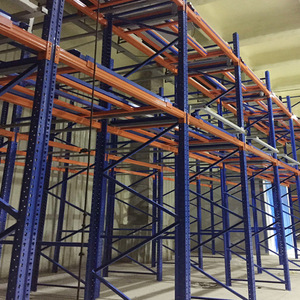
Reinforced cold-formed steel profiles with zinc-plated guide rails and automated obstacle detection for multi-shift continuous operations.
View Specifications →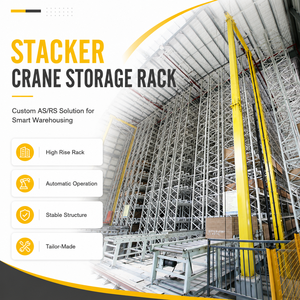
Turnkey high-bay warehouse integration combining stacker cranes, mother-daughter shuttles, and WCS software interfaces.
View Specifications →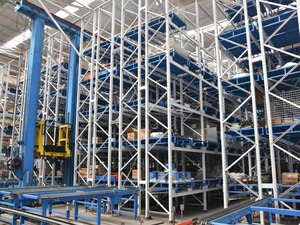
Specialized anti-corrosion and low-temperature steel construction designed specifically for cold chain and food processing facilities.
View Specifications →
Heavy-duty perimeter storage accessory enhancing SKU modularity, container safety, and loose item retention in high-bay setups.
View Specifications →In contemporary warehousing infrastructure, the pressure to maximize volumetric utilization while cutting labor-intensive forklift maneuvers has transformed high-density storage from an optional upgrade into an operational necessity. Shuttle pallet racking represents the technological bridge between static structural storage (such as drive-in or push-back systems) and fully automated high-bay ASRS (Automated Storage and Retrieval Systems).
Unlike traditional drive-in racking where forklifts must enter storage channels—resulting in frequent upright impacts, reduced throughput, and structural fatigue—a semi-automated radio shuttle racking system relies on self-propelled carts running on precision-formed horizontal rails. Pallet loads are positioned at the entry face by standard reach trucks or counterbalance forklifts; the wireless shuttle carrier lifts the unit load and transits autonomously down the lane to the nearest available storage buffer.
Structural Insight: The core failure point in sub-tier shuttle racking installations is not the mechanical shuttle cart, but cumulative dimensional rail deflection caused by substandard steel forming. High-performance factories employ continuous CNC roll-forming lines that hold profile straightness tolerances within ±0.5 mm over a 6-meter span.
| System Architecture | Volumetric Storage Density | Pallet Handling Mode | Forklift Damage Vulnerability | Capital Cost / Pallet Position | Typical Applications |
|---|---|---|---|---|---|
| Radio Shuttle Racking | 80% – 88% | FIFO or LIFO Automated | Ultra-Low (External bay only) | Moderate ($85 – $145) | FMCG, Cold Storage, High-Volume SKUs |
| Four-Way Shuttle (ASRS) | 88% – 94% | Dynamic Matrix 3D Routing | Zero (Unmanned operation) | High ($220 – $380) | E-commerce Fulfilment, High-bay 24/7 Hubs |
| Drive-In Racking | 65% – 75% | LIFO Strict | Extremely High (Frequent collision) | Low ($45 – $75) | Low-velocity seasonal bulk items |
| Selective Pallet Racking | 35% – 45% | 100% Direct Selective Access | Moderate (Aisle collisions) | Economy ($35 – $55) | High SKU fragmentation, retail distribution |
Fabricated exclusively from high-yield cold-rolled steel coils (Q235B and Q355B structural grades). Upright frames and omega profile beams provide high elasticity thresholds under dynamic cyclic loading.
Patented asymmetric guide tracks with zinc-electroplated or hot-dip galvanized finishes. Engineered to eliminate carriage slippage, guide shuttle tracking wheels, and support pallet bottom-board deflections.
Equipped with thermal-regulated Lithium Iron Phosphate battery modules capable of 8 to 10 hours continuous duty cycle per charge, maintaining discharge stability in sub-zero freezer chambers (-25°C).
How supply chain directors, industrial EPC contractors, and warehouse engineers are future-proofing intralogistics procurement over the coming decade.
Procurement paradigms have shifted dramatically from evaluating price-per-ton of steel to calculating Total Cost of Ownership (TCO), kilowatt-hour consumption per pallet cycle, and multi-tier system scalability. As global warehousing real estate costs rise—especially across logistics corridors in North America, Western Europe, and the Middle East GCC region—procurement teams face three clear strategic directions:
While traditional 2-way radio shuttles excel in single-deep and deep-lane mass SKU storage, procurement is pivoting rapidly toward 4-Way Shuttle Robotics. Four-way systems traverse both storage channels and cross-aisles, transitioning seamlessly between rack tiers via vertical reciprocating conveyors (lifts). This creates a software-orchestrated multi-agent swarm system that eliminates forklift reliance across the storage zone.
Industrial developers in coastal, arid, and high-temperature logistics parks (e.g., Dubai JAFZA, Jeddah Industrial, Texas Gulf Coast) now reject standard direct-to-metal spray coatings. Specification sheets require multi-stage chemical pretreatment—including immersion pickling and phosphating—followed by electrostatic thermosetting epoxy-polyester powder coating tested beyond 500 hours of continuous salt-spray exposure.
Proprietary shuttle controllers with closed protocols are becoming obsolete. Modern tier-1 procurement mandates shuttles equipped with Wi-Fi 6 / 5G industrial mesh connectivity, RESTful API hooks, and standardized Modbus/TCP interfaces that enable warehouse managers to coordinate shuttles, AGVs/AMRs, and overhead conveyors under unified ERP architectures.
Direct factory manufacturing since 2001. ISO 9001:2015 and CE Certified heavy structural fabrication with verified international distribution channels.
Founded in 2001, Guangzhou Heda Shelves Co., Ltd. has grown into a world-class manufacturing authority in high-density pallet racking, automated shuttle racking platforms, and industrial mezzanine floors. Spanning a modern 30,000 square meter factory base with over 300 technical production specialists, Heda provides complete in-house control over roll-forming, laser profiling, robotic welding, surface passivation, and export packing.
High-volume continuous roll-forming lines guarantee stable, on-schedule production schedules even for mega-warehouse contracts exceeding 15,000 pallet positions.
Fully compliant with European Standard EN 15512 and FEM intralogistics standards. CE Certificate No. 2435-CPR-8605159 and ISO 9001:2015 registration provide audit-proof reliability.
Our senior logistics civil engineers generate bespoke 2D CAD layouts and 3D operational simulations, including slab load-bearing and seismic risk assessments, before contract finalization.
Components undergo comprehensive chemical pickling, phosphating, pure-water rinse, and automated electrostatic powder coating to ensure anti-rust resilience across extreme environments.
Heavy upright frames and beams are bundle-strapped with protective corner guards and labeled sequentially according to installation sequence, minimizing site staging time.
Proven track record of regular port deliveries to Jebel Ali, Dammam, Jeddah, Hamad, Sohar, and major international hubs across 120+ destination countries worldwide.
Authoritative engineering answers addressing load calculations, cold store operations, civil approvals, and maintenance protocols.
Because radio shuttles travel along horizontal steel guide rails supported by upright frames, floor flatness is critical. According to DIN 18202 (Table 3, Group 4) and FEM 9.831 / EN 15620 guidelines, the floor levelness under racking posts should not exceed 3 mm deviation over a 2-meter straight edge. For high-bay installations exceeding 10 meters in upright height, superflat slab standards (FM2 or higher) are strongly recommended to prevent structural tilt and dynamic eccentric loading.
Shuttle systems are an ideal choice for cold chain operations because they maximize thermal density and eliminate the need for forklifts to enter refrigerated bays, reducing energy losses. HEDA cold-room shuttles are built with specialized low-temperature components, including cold-resistant hydraulic fluids, low-temp lubricant seals, IP65 electronic enclosure sealing, internal thermal heating resistors, and low-temperature Lithium Iron Phosphate (LiFePO4) battery packs rated for continuous performance down to -25°C.
Yes. A primary operational advantage of shuttle racking is dual-mode capability. In a LIFO (Last-In, First-Out) setup, loading and unloading occur from the same front face, minimizing aisle space. In a FIFO (First-In, First-Out) setup, pallets enter from the charging face and are retrieved from the discharging face. This versatility suits date-sensitive FMCG, pharmaceutical, and perishables distribution centers.
HEDA delivers a comprehensive engineering calculation pack for local authorities, Civil Defense departments, and structural compliance inspections. This includes structural frame stability calculations, dead load/live load analysis, deflection verification under EN 15512 / RMI standards, baseplate anchor pull-out ratings, and site-specific seismic coefficient evaluations.
HEDA industrial shuttles utilize quick-swap LiFePO4 battery modules. A full charge requires approximately 2.5 to 3.5 hours, providing 8 to 10 hours of continuous pallet movements. With dual battery packs per shuttle, warehouses can sustain 24/7 round-the-clock operations. The battery cells deliver an operational design life exceeding 2,500 full charge-discharge cycles before dropping below 80% original capacity.
Rail alignment is maintained via cold-rolled galvanized guide rails bolted directly to heavy-duty horizontal support arms with serrated locking hardware. Support arms hook securely into teardrop or diamond upright frame perforations and are locked with high-shear safety pins. Dynamic braking forces from the shuttle are dissipated across the entire longitudinal frame run via horizontal and vertical back bracings.
Connect directly with senior structural storage engineers at Guangzhou Heda Shelves Co., Ltd. Request our comprehensive industrial product technical whitepaper, load-bearing capability charts, and complete CAD layout specifications for your upcoming high-density storage facility.