Hazmat Safe Chemical Drum Pallet Racking
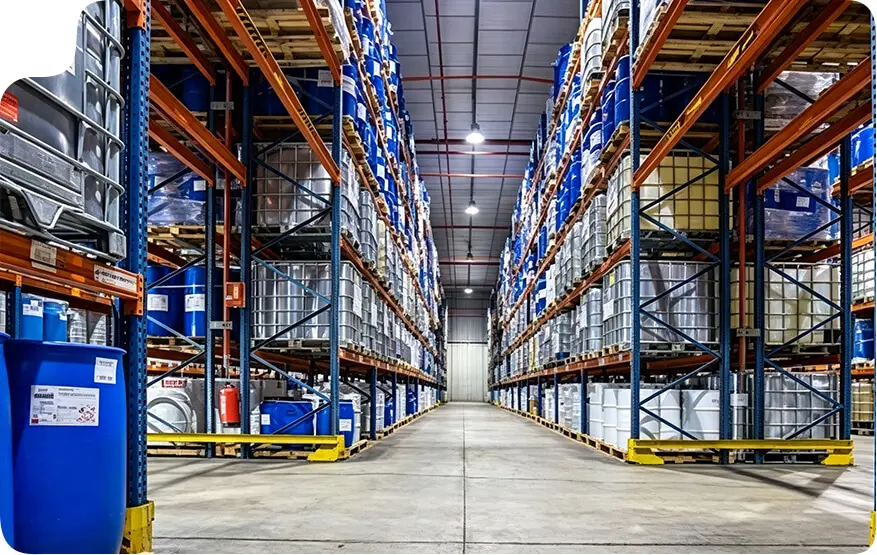
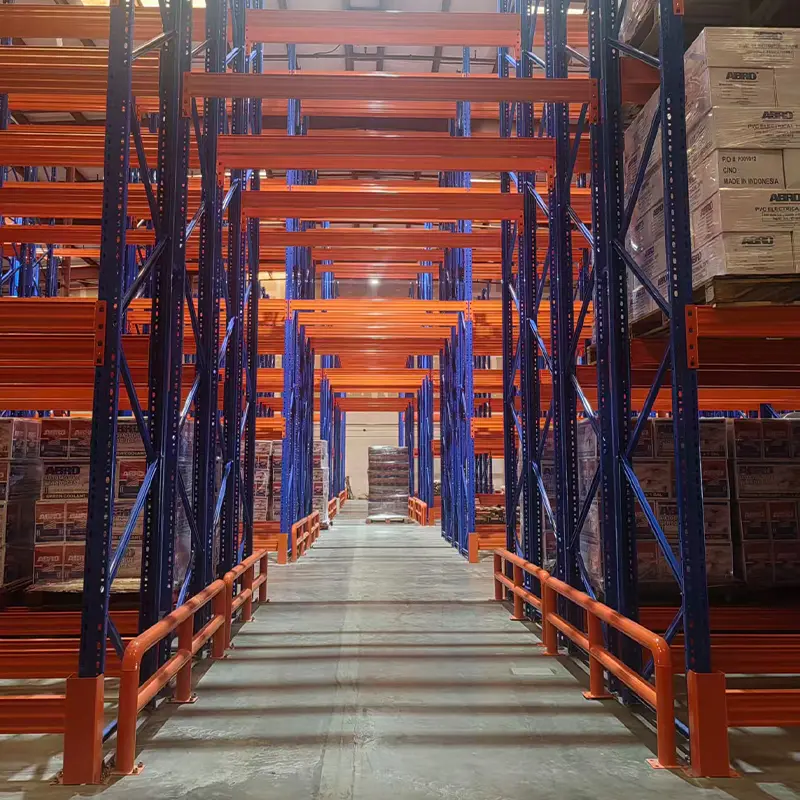
Heavy-duty selective racking outfitted with custom drum cradles, barrel positioning chocks, and bottom spill trays. Provides 100% direct selectivity for vertical or horizontal drum storage.
Storing hazardous industrial chemicals, combustible solvents, volatile petrochemicals, and agricultural fertilizers demands far more than basic structural steel. Warehouse operators must satisfy stringent health, safety, and environmental (HSE) regulations, prevent environmental spill contamination, and guarantee rack integrity under extreme thermal and seismic stresses.
Unlike standard fast-moving consumer goods (FMCG) storage, chemical warehouse storage deals with concentrated heavy dynamic loads (such as 1,000-liter intermediate bulk containers / IBC totes weighing over 1,200 kg each, or clustered 55-gallon oil and solvent steel drums). A minor deflection in cross beams or accidental forklift impact can cause hazardous leaks, toxic vapor releases, or catastrophic cascade failures.
At Guangzhou Heda Shelves Co., Ltd., every chemical storage racking system is engineered using finite element analysis (FEA) based on European EN 15512 codes, ANSI MH16.1 guidelines, and regional civil defense fire codes. Our cold-rolled structural steel profiles (Q235B and high-yield Q355B) feature cold-bent multi-flange upright columns capable of supporting massive continuous vertical loads without structural fatigue.
Furthermore, our designs integrate mandatory longitudinal and transverse open flue spaces directly aligned with early suppression fast response (ESFR) ceiling and in-rack sprinkler heads, ensuring fire protection systems can instantly penetrate deep rack levels in compliance with NFPA 30 Flammable and Combustible Liquids Codes.
Our 10-stage pretreatment acid pickling and phosphating process bonds electrostatic epoxy-polyester coatings permanently to the substrate, preventing acid, alkaline, and solvent degradation.
Certified steel and chemical-grade polymer containment bunds positioned under each pallet bay catch unexpected drips and barrel ruptures, shielding floor slabs and groundwater.
Comprehensive CAD layout submission packages featuring certified load ratings, flue widths, safety barrier clearances, and egress route compliance for smooth municipal permitting.
Reinforced column base wrap guards, wrap-around post buffers, and end-of-row tubular bollards absorb repetitive forklift collisions common during heavy liquid barrel transport.
Choosing the right chemical storage racking system depends on packaging type (IBC tanks, steel drums, plastic canisters, or bulk powder totes), SKU rotation frequency, and hazardous classification.
Hazmat Safe Heavy-duty selective racking outfitted with custom drum cradles, barrel positioning chocks, and bottom spill trays. Provides 100% direct selectivity for vertical or horizontal drum storage.
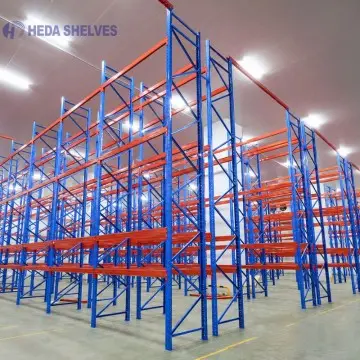
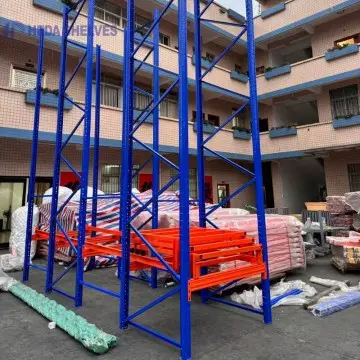
Reinforced double-C beam profiles specifically calculated for heavy 1,000L to 1,500L IBC container concentrated loads up to 4,000 kg per beam pair, with welded pallet stop beams.
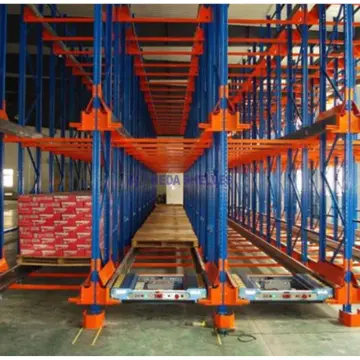
Automated shuttle carrier eliminates forklift entry into deep chemical lanes. Minimizes structural impact risk and reduces operator exposure to toxic solvent and gas storage atmospheres.
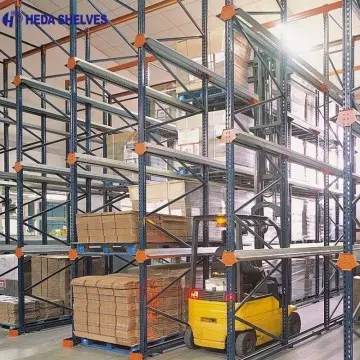
Ideal for stable, non-flammable raw chemicals, fertilizers, and polymer granules stored in bulk batch pallets. Maximizes floor utilization by up to 80% through continuous lane density.
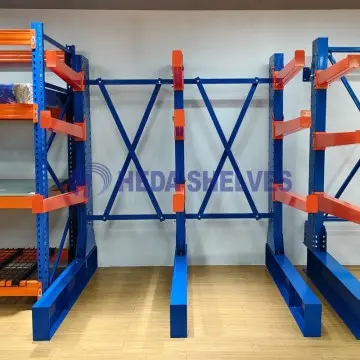
Designed for chemical processing piping, long raw materials, bar stock, and pressurized gas cylinder bundles. Arm capacities up to 3,000 kg with retaining end-pins for zero slippage.
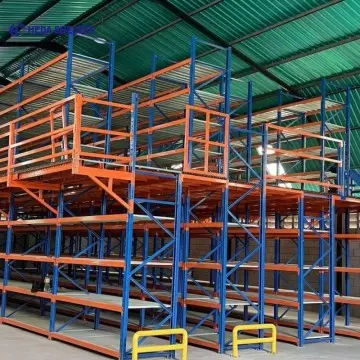
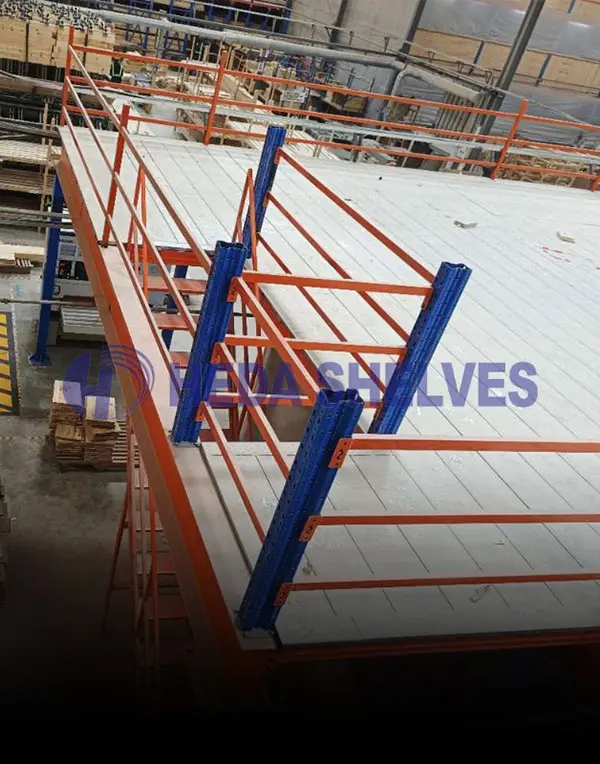
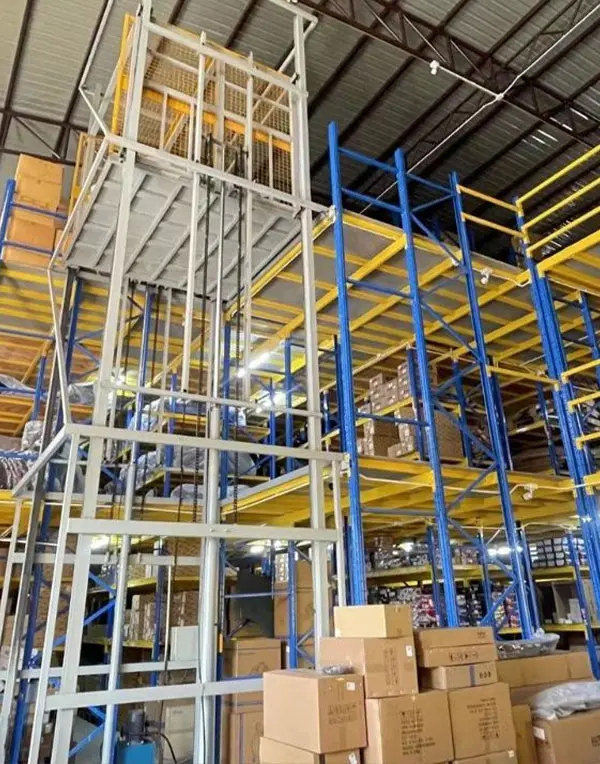
Multi-tier structural or rack-supported mezzanine floors built for laboratory sample archives, chemical dispensing benches, and container repacking lines with chemical-resistant steel grating.
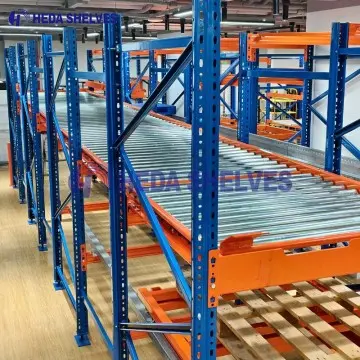
Inclined roller beds with heavy-duty speed controllers enable strict first-in, first-out stock rotation for perishable adhesives, sealants, catalysts, and temperature-sensitive chemicals.
Nested rolling carts accommodate 2 to 6 pallets deep per lane. Balances high pallet density with rapid forklift accessibility for intermediate chemical batch manufacturing facilities.
As safety audits become digitized and global chemical supply chains tighten regulatory enforcement, procurement executives must anticipate four macro shifts reshaping chemical storage installations worldwide.
01 Procurement teams are moving away from aftermarket plastic drip pans toward factory-integrated, certified galvanized steel bund sumps built directly into the racking tiers. This structural integration ensures compliance with local environmental protection agencies while maximizing vertical cubic space.
02 Traditional indoor paint degrades rapidly under vaporous hydrochloric, sulfuric, or volatile hydrocarbon environments. Future-proof chemical logistics facilities now specify high-thickness epoxy-phenolic powders, zinc-rich thermal primers, or total hot-dip galvanization to achieve 25+ years of operational structural service life.
03 To reduce human exposure to toxic vapors and explosive dusts, automated storage and retrieval systems (AS/RS) and explosion-proof radio shuttles are rapidly replacing manual counterbalance forklifts in toxic chemical, agrochemical, and battery precursor distribution hubs.
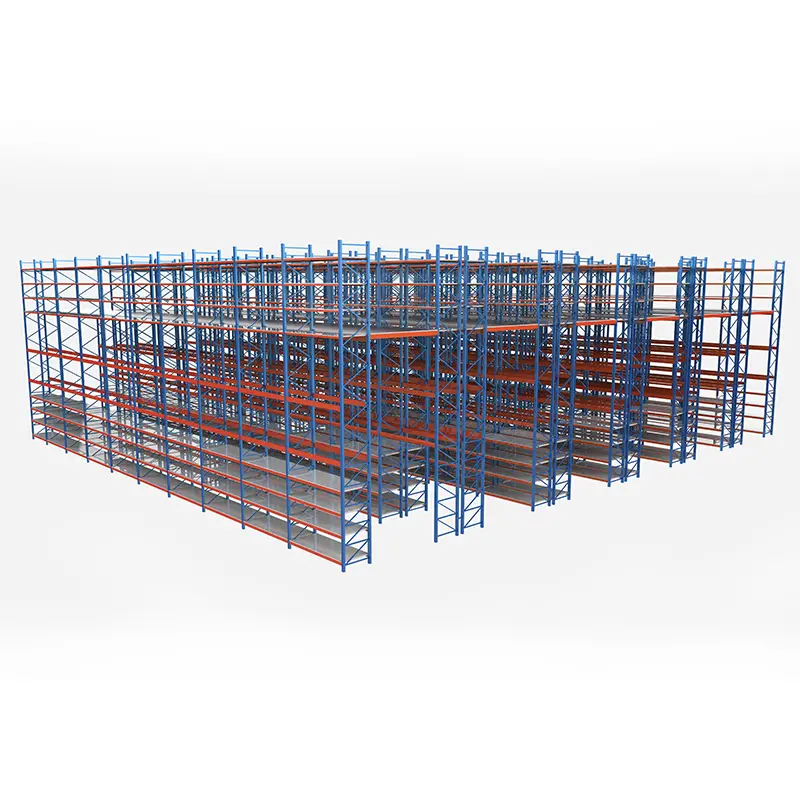
04 Global insurers now demand 3D digital simulations that prove water spray pattern penetration across all racking tiers before project signing. Guangzhou Heda Shelves Co., Ltd. leads this transition by supplying parametric BIM and 3D CAD models calibrated for precise sprinkler and ventilation alignment.
Since 2001, Guangzhou Heda Shelves Co., Ltd. has grown to become an international powerhouse in heavy-duty warehouse racking and specialized industrial storage engineering. With an advanced 30,000 m² smart manufacturing plant and over 300 experienced technical experts, we deliver factory-direct engineering, fabrication, and worldwide delivery without third-party markups.
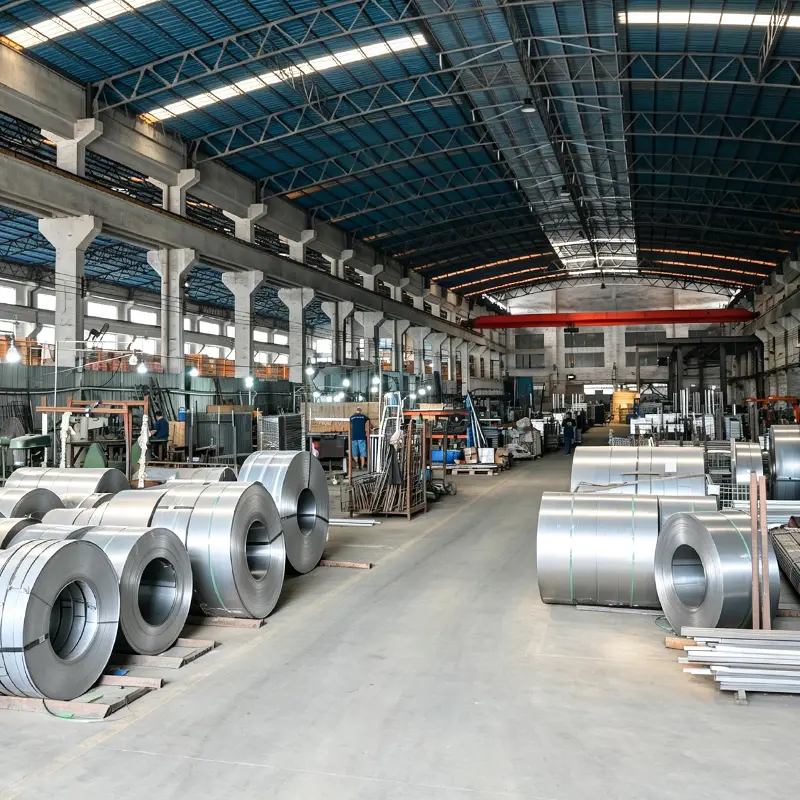
Chemical warehousing demands unyielding material integrity. We source prime Q235B and Q355B certified steel coils directly from premier domestic steel mills. Every upright column, load beam, bracing member, and spill containment sump is roll-formed, laser-cut, robot-welded, and surface-treated entirely in-house under stringent ISO 9001:2015 quality management procedures.
Chemical storage safety begins at raw material molecular inspection and ends with secure container transport packing. Here is how Guangzhou Heda Shelves Co., Ltd. guarantees zero structural failure.
Step 01
Step 02
Step 03
Step 04
Step 05
Step 06
Step 07
Step 08
Step 09
Step 10Explore how international chemical manufacturers, oil blending plants, and logistics parks rely on our custom-engineered racking installations.
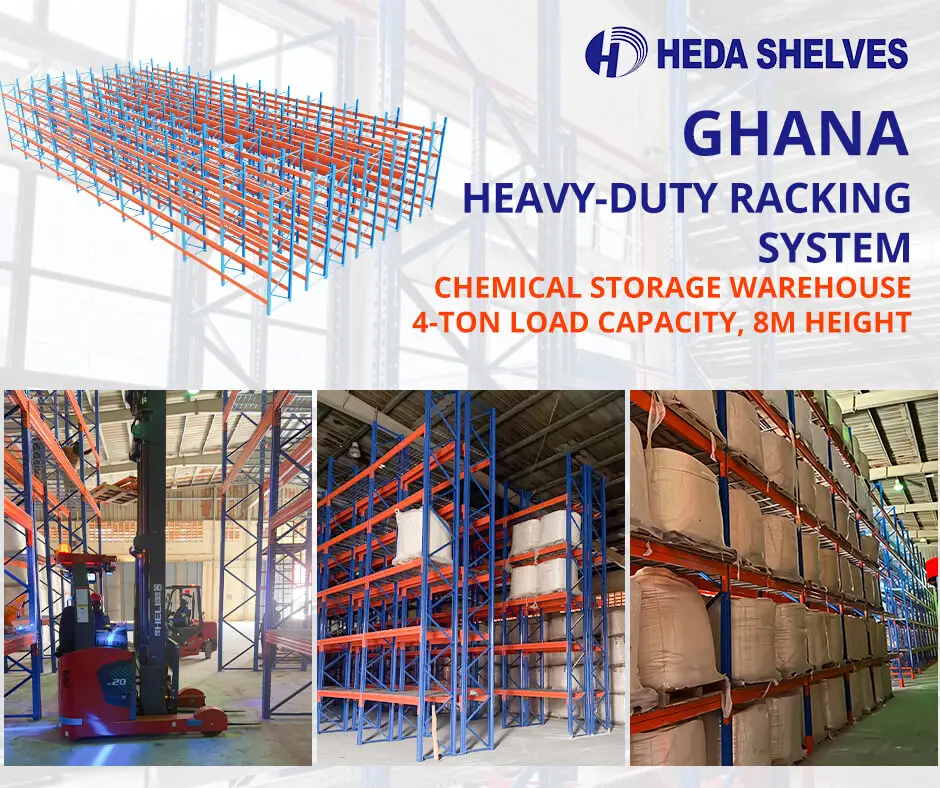
Ghana · 2,400 Pallet Positions with Spill Trays
Kenya · Acid-Resistant Grating Decking
Thailand · High Load Capacity Uprights
Procurement authorities, environmental agencies, and civil defense bodies require official, verifiable compliance documents. Guangzhou Heda Shelves Co., Ltd. provides certified proof for all vendor approval audits.
Trusted by Global Chemical Brands & Industrial Logistics Leaders
Answers to key technical, regulatory, and engineering questions frequently asked by chemical warehouse managers, safety engineers, and procurement specialists.
Send an InquiryThe optimal surface finish depends on the chemical vapor concentration. For warehouses storing mild solvents, lubricants, and solid chemicals, our multi-stage electrostatic epoxy-polyester powder coating (applied after automated acid pickling and phosphating) provides excellent protection. For highly corrosive acid, chlorine, alkali, or open-air coastal storage yards, Guangzhou Heda Shelves Co., Ltd. provides hot-dip galvanizing (HDG) in accordance with ISO 1461, ensuring complete cathodic corrosion immunity for 25+ years.
Our chemical racking systems can be fitted with custom-engineered containment sump trays located beneath pallet support beams. These trays are fabricated from heavy-gauge galvanized steel or acid-resistant polymer, engineered with minimum 110% containment capacity for single IBC containers or 25% of total stored volume to satisfy OSHA 1910.106 and EPA 40 CFR 264.175 spill containment regulations.
Yes. Our engineering department develops warehouse CAD floor layouts and 3D schematics adhering directly to NFPA 30 guidelines and local Civil Defense regulations. We calculate required transverse and longitudinal flue spaces (typically 75 mm to 150 mm) so that in-rack ESFR sprinkler lines and smoke detection sensors operate without obstruction during emergency inspections.
Liquid stored in IBC totes and drums creates dynamic sloshing momentum during seismic motion or sudden forklift impacts. Our structural calculations use reinforced box-welded upright frames, oversized baseplates anchored with heavy-duty chemical wedge expansion bolts, and reinforced diagonal cross-bracing that dampen lateral vibrational forces.
Standard custom chemical racking systems are manufactured within 15 to 25 business days at our 30,000 m² factory. All components are packed in container-optimized, protective steel bundles with itemized identification tags cross-referenced to CAD assembly blueprints. We arrange factory-direct shipping to all GCC and worldwide ports (such as Jebel Ali, Dammam, Jeddah, Hamad, and Sohar) with customs clearance support.
Simply provide your warehouse architectural drawing (or length × width × clear ceiling height), floor slab load tolerance (kN/m²), unit load dimensions and gross weight (drum pallet or IBC tote), forklift operational aisle width, and the hazard classification (MSDS/SDS). Our engineering team will supply a complete 2D CAD layout, 3D render, and structural quote within 24 hours.
Prevent costly compliance fines, containment failures, and structural warehouse risks. Connect with senior structural engineers at Guangzhou Heda Shelves Co., Ltd. for factory-direct chemical warehouse racking systems engineered to international safety standards.
Technical Inquiries: [email protected]