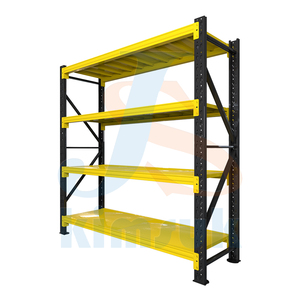
Customized Warehouse Multi-level Mezzanine Rack System
Maximizes vertical cubic capacity with high-tensile multi-tier flooring, integrated catwalks, and heavy-duty load capacities up to 1,000 kg/m².
HEDA Shelves manufactures and exports heavy-duty industrial gravity flow pallet racking systems, multi-tier mezzanine floors, teardrop pallet racking, and specialized materials-handling structures. Designed to minimize internal handling costs, maximize footprint efficiency, and streamline strict First-In, First-Out (FIFO) stock turnover across cold storage, agro-industrial, and FMCG sectors.
Maximizes vertical cubic capacity with high-tensile multi-tier flooring, integrated catwalks, and heavy-duty load capacities up to 1,000 kg/m².
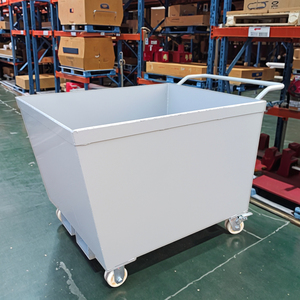
4-high stackable self-cleaning galvanized cages tailored for high-volume parts organization, agricultural harvesting, and reverse logistics.
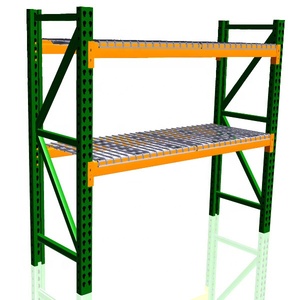
Universal interchangeable connection pattern providing rapid tool-less beam adjustment, high torsional stiffness, and full RMI-compliant structural integrity.
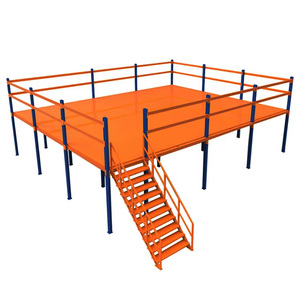
Combines bottom pallet storage with secondary-floor picking space. Engineered with modular cold-rolled steel channels for rapid site erection.
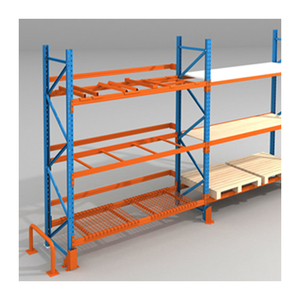
Treated with multi-stage phosphating and anti-static powder coatings to resist ambient humidity in coastal zones like Buenaventura and Cartagena.
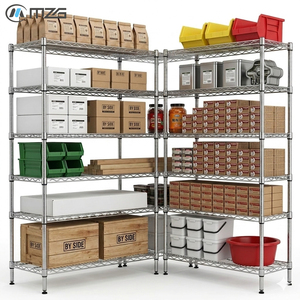
Sanitary, open-wire design promoting unobstructed air circulation, light penetration, and clean cold-chain airflow for food processing plants.
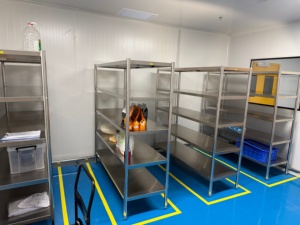
Ultra-clean, corrosion-free mobile shelving engineered for pharmaceutical cleanrooms, medical labs, and cold storage operations requiring frequent washdowns.
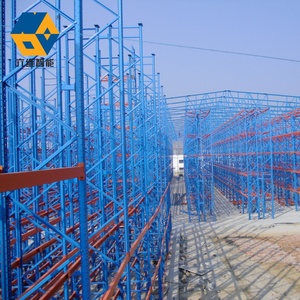
Self-supporting structural racking engineered to eliminate standard civil building columns, functioning as both product racking and building superstructure.
Gravity flow racking (Pallet Live Storage) functions as an autonomous, self-powered internal transport system. By utilizing inclined roller tracks configured between 2.5% to 4% declination, loads glide under regulated gravitational kinetic force from the entry charging aisle to the retrieval discharge face.
To safeguard structural frames and goods against uncontrolled acceleration, our systems incorporate centrifugal magnetic and mechanical brake rollers at exact intervals. These regulate pallet travel speed to a consistent, safe velocity under 0.3 meters per second regardless of pallet weight variations from 300 kg to 1,500 kg.
When retrieving pallets at the picking face, hydrostatic and mechanical pallet separators absorb the line pressure exerted by trailing inventory. This relieves back-pressure, ensuring forklift operators can execute smooth, frictionless extraction without jamming or load-snagging risks.
Roll-formed heavy-gauge galvanized steel wheel beds prevent track deflection over long shelf spans. Entry guidance funnels align pallets automatically upon insertion, correcting operational offsets before the pallet engages the roller lane.
Colombia’s distinctive macroeconomic topology—defined by high-altitude plateaus, tropical coastal shipping hubs, and aggressive metropolitan warehouse land valuation—demands hyper-dense material handling systems tailored to specific sector requirements.
Concentrated on the Sabana de Bogotá and Rionegro (Antioquia), fresh flower exporters manage time-critical cold rooms near El Dorado (BOG) and José María Córdova (MDE) airports. Pallet flow systems provide non-negotiable FIFO turnover, cutting cold-room cubic refrigeration energy loss by up to 45% through high-density aisle consolidation.
Within the Eje Cafetero, Valle del Cauca, and central distribution hubs in Funza and Cota, food and beverage enterprises store high-velocity fast-moving consumer goods. Live pallet flow lanes separate loading personnel from retrieval trucks, eliminating fork truck traffic conflicts and maximizing dispatches per hour.
Modern life science clusters around Bogotá and Cali adhere to stringent INVIMA regulatory validation. Dynamic gravity racking guarantees zero-defect batch tracking and strict expiration-date rotation, preventing dead-stock write-offs while maintaining immaculate sanitary audit trails.
Strategic shifts in modern industrial real estate demand structural performance, high seismic compliance, and rapid return on capital across Colombian trade corridors.
Industrial development parks (Parques Industriales) along the Calle 80 and Autopista Medellín corridors in Cundinamarca face premium square-meter lease valuations. Operations can no longer expand horizontally. Gravity flow systems deliver 60% higher storage density over conventional selective racking by condensing 10 to 15 pallet positions in depth per lane while eliminating intermediate service aisles.
Colombia lies along active tectonic fault lines (Pacific Ring of Fire), designating Bogotá, Bucaramanga, and western regions as intermediate-to-high seismic risk zones. Warehouse engineering must strictly satisfy Colombia’s NSR-10 (Norma Sismo Resistente) building regulations. HEDA Shelves engineers structural upright profiles, heavy baseplates, and bracing trusses capable of handling seismic shear loads under full dynamic live-weight capacity.
Export-oriented companies leveraging Colombia's strategic maritime positioning through the Ports of Buenaventura, Cartagena, and Barranquilla are establishing automated hub centers within Zonas Francas. High-density gravity live racks optimize custom bonded warehouses where bonded inventory staging requires rapid container de-stuffing and high-velocity dispatch.
Unlike fully automated crane AS/RS installations that require high electrical power draw and specialized software maintenance, gravity flow systems function purely via natural gravitational force. They reduce forklift driving cycles and operating hours, directly lowering warehouse diesel/electric consumption while accelerating throughput.
From prime Q235B/Q355B cold-rolled coil steel to ocean-freight container packing, every component is manufactured in-house under strict ISO 9001:2015 controls.
Structural load calculation based on seismic acceleration (Aa/Av), floor slab concrete psi rating, and specific pallet dimensional tolerances.
Continuous roll-forming lines with multi-station automated punch tooling guarantee pitch uniformity and rigid load beam integration.
Automated 9-stage acid pickling, zinc phosphating, and thermosetting epoxy-polyester electrostatic powder coating cured at 200°C.
Bundled with protective corrugated wrapping, steel strapping, and labeled match-marking to streamline customs clearance at Colombian seaports.
We eliminate intermediaries, supplying direct factory engineering to Colombian logistics directors, distributors, and general contractors.
Compliant with CE standards (No. 2435-CPR-8605159), ISO 9001:2015 Quality Management (No. 18624Q00169R0M), and international RMI specifications, facilitating quick insurance underwriting and local municipal sign-offs.
Our 30,000 m² modern manufacturing infrastructure with over 300 technical personnel executes high-volume turn-key projects with reliable 15 to 25 day factory lead times.
Before final quotes, our structural engineers deliver complete warehouse layout CAD floor plans, structural node details, and realistic 3D renderings mapped to your forklift aisle clearances.
Detailed technical, logistical, and import guidance for operations and supply chain managers ordering storage racks into Colombia.
Connect with our structural engineering team today. Send us your architectural floor plan, storage dimensions, and throughput targets for a complimentary 2D CAD layout and formal factory-direct proposal.