High-Density Pallet Shuttle Engineering & Factory Execution
Modern supply chains face unprecedented volatility in land acquisition costs, warehouse leasing rates, and operational labor overhead. Conventional selective racking architectures dedicate more than 60% of total warehouse floor footprint to forklift access aisles, capping volumetric storage efficiency under 40%. The CE Certified Radio Shuttle Racking System manufactured by Guangzhou Heda Shelves Co., Ltd. represents an advanced paradigm in high-density semi-automated material handling. By deploying intelligent, bi-directional carrier shuttles along precision cold-formed steel guide rails within deep pallet channels, warehouse operators maximize cubic footprint utilization up to 85% while drastically mitigating structural forklift impact damage, inventory shrinkage, and picking cycle latencies.
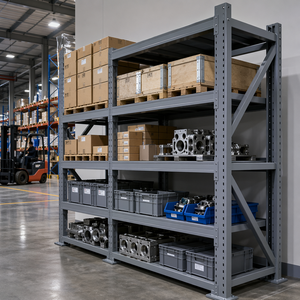 Anti-Corrosion
ISO9001 Certified Custom OEM Stainless Steel Shelving Frame
- 304/316 Steel
- Acid Pickled
- Cleanroom Ready
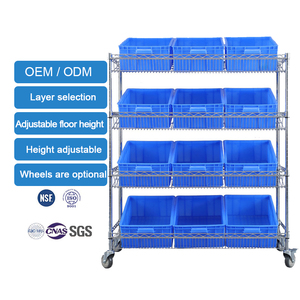 Order Picking
Light Duty Adjustable 4-5 Tier Warehouse Picking Cart
- Heavy-Duty Casters
- Modular Wire Mesh
- E-Commerce Hub
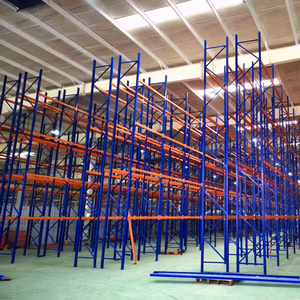 Automated Hub
2-5 Tier Wide Aisle Heavy Load Automated Pallet Racking
- Up to 4,500kg/Beam
- High Clearance
- Fulfillment Ready
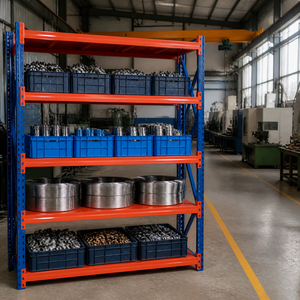
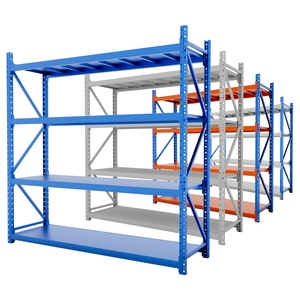 Factory Direct
 4-Tier 500-2000kg Heavy Duty Industrial Rack
- Q235B Cold Steel
- Long-Span Beam
- Powder Coated
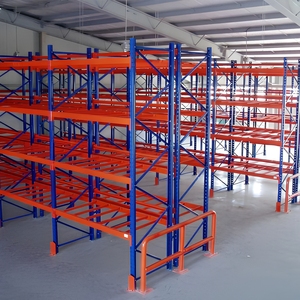
 High Bay VNA
Custom Adjustable Anti-Rust Very Narrow Aisle (VNA) Racking
- Floor Guide Rails
- Max Height 16m
- Zero Aisle Waste
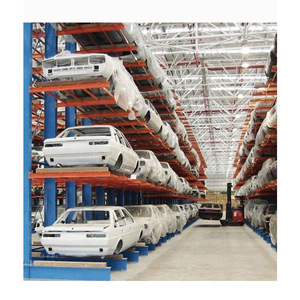
 100% Selective
Industrial Adjustable Heavy Duty Conventional Pallet Racking
- 75mm Pitch Slot
- Multi-SKU Access
- ISO9001 Tested
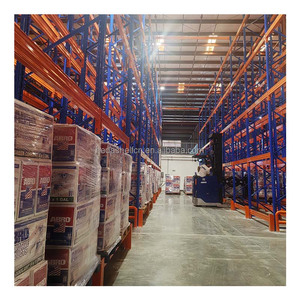
 Structural Steel
CE Certified Heavy-Duty Cantilever Racking for Auto & Pipe
- 3,000kg Per Arm
- H-Beam Column
- No Front Upright
 OEM Standard
Factory Heavy Duty Storage Pallet Racking System Supplier
- Direct Mill Supply
- Custom RAL Tones
- Seismic Compliant
Radio Shuttle vs. Traditional High-Density Storage Topologies
Selecting the appropriate storage infrastructure requires assessing structural capacity, throughput rate (pallets per hour per aisle), equipment lifecycle fatigue, and operational safety. Traditional drive-in racking creates hazardous operational friction because forklifts must navigate deep, narrow channels, causing repeated collision damage to uprights. Gravity flow racking eliminates forklift intrusion but relies on mechanical rollers that suffer from dust abrasion, friction degradation, and pallet jamming.
| Evaluation Metric | Radio Shuttle Racking | Drive-In Racking | Push-Back Cart Racking | Automated Crane AS/RS |
|---|---|---|---|---|
| Volumetric Utilization (%) | 80% – 88% | 65% – 75% | 60% – 70% | 90% – 95% |
| Throughput Velocity (Pallets/Hr) | 35 – 50 cycles/hr/shuttle | 12 – 18 cycles/hr/mast | 18 – 25 cycles/hr | 40 – 65 cycles/hr/crane |
| Forklift Mast Channel Travel | Zero Intrusion (Perimeter Only) | Full Channel Intrusion | Face Load Only | Fully Automated Stacker |
| Stock Rotation Logic | Dual Flex: FIFO and LIFO | Strictly LIFO | Strictly LIFO | Full Dynamic WMS Routing |
| Channel Depth Capability | Up to 40 Pallets Deep | Max 7–10 Pallets (Safety Limit) | Max 4–6 Pallets | Double or Multi-Deep |
| Structural Collision Risk Index | Extremely Low (<5% Baseline) | Very High (>75% Damage Rate) | Moderate (Front Beam Impacts) | Negligible (Sensor Monitored) |
| CapEx Amortization Period | 14 – 22 Months | 12 – 18 Months | 18 – 26 Months | 48 – 72 Months |
LiFePO4 Intelligent Power Architecture
Shuttle carts incorporate automotive-grade Lithium Iron Phosphate (LiFePO4) battery packs operating at 24V or 48V with continuous 8-to-10 hour operational endurance. Integrated fast-charging docks restore 80% charge within 60 minutes, while cold-chain thermal insulated battery management systems (BMS) guarantee cold-start reliability down to -30°C without amp-hour capacity collapse.
Optoelectronic Laser & RFID Positioning
Sub-millimeter lane guidance is achieved through optical quadrature encoders and dual Sick or Omron laser distance sensors. The carrier senses end-of-channel proximity, pallet clearance gaps, and rail deformation in real-time, executing deceleration profiles that eliminate load tipping when carrying fragile FMCG, pharmaceutical, or beverage containers up to 1,500kg.
EN 15512 Structural Compliance
Every upright profile is engineered using Q355B high-tensile cold-rolled steel coils, fabricated with continuous automated roll-forming lines. Structural calculations conform strictly to European Standard EN 15512:2020 and RMI standards, delivering certified beam deflection ratios well below L/200 under static and dynamic shuttle braking loads.
Future Procurement & Technological Development Trends (2026–2030)
Procurement engineers and supply chain executives must plan material handling investments against rapid shifts in warehouse automation, energy efficiency regulations, and real-time ERP integration. The radio shuttle market is shifting from isolated semi-automated shuttles into coordinated, smart multi-tier ecosystems.
Convergence with 4D Multi-Directional Shuttles
While 2D shuttles move along single linear lanes, enterprise facilities are rapidly procuring 4D autonomous shuttles capable of traversing both longitudinal storage channels and perpendicular transfer aisles via internal lifting wheels. Paired with vertical reciprocating lifts (VRCs), 4D shuttles navigate 3D warehouse matrices without requiring forklift repositioning, bridging the gap between semi-automation and lights-out AS/RS at 40% lower initial capital expenditure.
WCS/WMS Microservices & Fleet Management
Procurement requirements now demand bi-directional API handshakes between shuttle PLC control boards and tier-1 Warehouse Management Systems (SAP, Manhattan, Infor). Utilizing secure industrial 5G and mesh Wi-Fi protocols (MQTT and OPC UA), central dispatch software dynamically balances task distribution across shuttle swarms, performing predictive slotting optimization, automated SKU consolidation, and real-time cycle counting.
Cold Chain Optimization & ESG Standards
Global frozen food trade and pharmaceutical cold chain standards are accelerating procurement of high-density shuttle racking rated for -30°C environments. Reducing refrigerated warehouse volume by 45% per pallet position directly lowers compressor electrical consumption by up to 35%. Modern procurement contracts evaluate Embodied Carbon footprints, favoring steel factories that utilize clean hydropower-sourced electric arc furnaces (EAF) and non-VOC powder coating lines.
HEDA Shelves: 25+ Years of Certified Racking Engineering Excellence
Founded in 2001, Guangzhou Heda Shelves Co., Ltd. operates an advanced 30,000 square meter intelligent manufacturing base in Guangzhou, China. Generating a monthly structural steel production capacity exceeding 30,000 tons, our factory serves system integrators, general contractors, and logistics operators across 120+ countries, including extensive project deployments across the Middle East (UAE, Saudi Arabia, Qatar, Oman, Kuwait, Bahrain), Europe, Southeast Asia, and the Americas.
Our Traceable 10-Step Precision Fabrication Pipeline
Unlike regional intermediaries or trading houses, HEDA Shelves controls every metallurgical, forming, and chemical finishing phase within our proprietary facility. Every heat number of steel coil is lab-tested, and every finished upright frame is tracked through our comprehensive ERP to ensure reliable structural execution on the warehouse slab.
 Step 01
Raw Coil Metallurgy & Tensile Verification
 Step 02
CNC Automated Laser & Slitting Line
 Step 03
High-Speed Continuous Punching
 Step 04
Precision Cold-Bending Mechanics
 Step 05
Multi-Station Profile Roll-Forming
 Step 06
Mechanical Edge Polishing & Deburring
 Step 07
Robotic Shielded Arc Welding (GMAW)
 Step 08
Chemical Acid Pickling & Phosphating
 Step 09
Thermoset Electrostatic Powder Coating
 Step 10
CMM Quality Control & Export Bundling
Audited Certifications for Rigorous Civil Defense & Tendering Compliance
HEDA Shelves products hold factory-audited European CE Certification (Certificate No. 2435-CPR-8605159 conforming to EN 1090-1 and Construction Products Regulation), ISO 9001:2015 Quality Management Accreditation (Certificate No. 18624Q00169R0M, verified valid through June 2027), and international RoHS compliance for heavy-metal-free thermosetting resin coatings.


How does the Radio Shuttle system handle bottom-deflection on non-standard or damaged wooden pallets?
What floor slab flatness tolerances are required for high-bay radio shuttle installations exceeding 12 meters?
Can the same shuttle carrier operate reliably across both ambient and sub-zero cold storage zones?
How are fire sprinkler systems and transverse flue spaces integrated according to NFPA 13 regulations?
What is the expected Total Cost of Ownership (TCO) and return on investment period compared to standard Drive-In racking?
What export freight packaging and on-site erection support does HEDA Shelves provide for overseas buyers?
Accelerate Your High-Density Warehouse Transformation
Collaborate directly with our senior racking structural engineers. Send us your architectural floor plans, clear ceiling heights, and pallet payload parameters to receive a complimentary 2D CAD layout, 3D structural rendering, and comprehensive factory-direct quotation within 24 hours.