Factory-Engineered Intralogistics Storage Systems
Direct supply from Guangzhou manufacturing base: Certified cold-formed structural steel storage systems for bulk warehousing, FMCG cold chain, distribution hubs, and high-density industrial facilities.
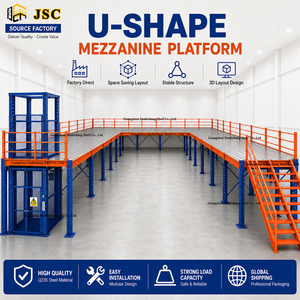 Space Optimization
Industrial Warehouse Mezzanine Floor System Steel Structure Platform For Space Saving Storage Solution
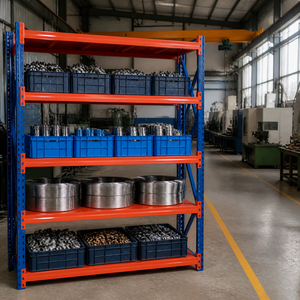 VNA High Bay
Custom Adjustable Anti-Rust Storage Metal Stacking Racks Pallet Racking System Steel Shelving VNA Racking Narrow Aisle Rack
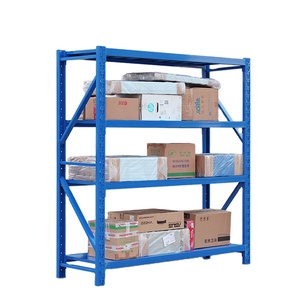 Manual Picking
JIAMEI Storage Shelving Warehouse Storage Rack Long Span Shelf Rack
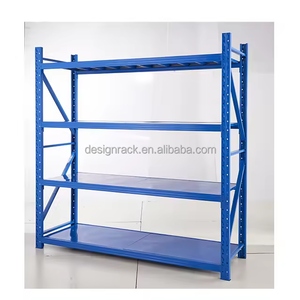 Wholesale
Wide Span Shelving Units Wholesales Price Warehouse Rack Storage Pallet Racks Shelf Blue & Orange Pallet Racking
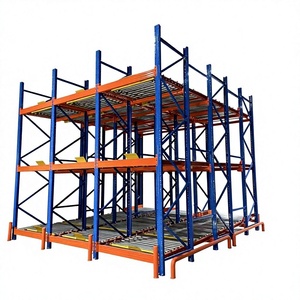 FIFO Flow
Pallet Flow Racking Gravity Roller Flow Through Rack FIFO High Density Warehouse Pallet Storage System Metal Steel Anti-Rust
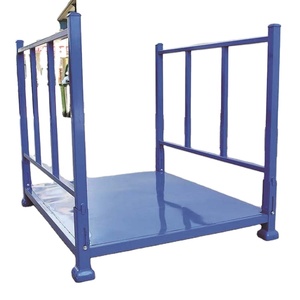 Dynamic Stacking
Stacking Heavy Duty Pallet Rack Gravity Racking Folding Logistics Freight Storage Equipment Powder Coating Assembled Steel Blue
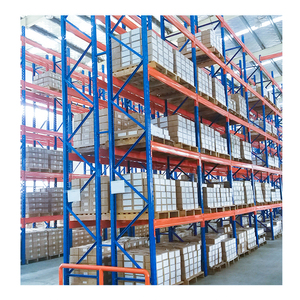 High Utilization
Multi Level Shelf Rack Cost Effective Steel Factory Warehouse Heavy Duty Industrial Pallet Racking
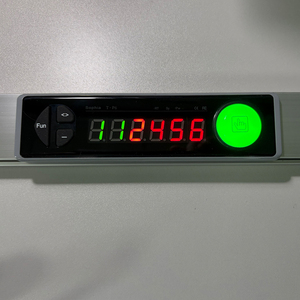 Smart Warehouse
Sophia 6 Digit Display Pick to Light Picking Tag Electronic TagT- P6 for Warehouse Rack
Factory Direct Precision: Guangzhou HEDA Shelves Co., Ltd.
Serving EPC logistics contractors, 3PL distributors, and supply chain operators across 120+ countries since 2001 with verified static and dynamic engineering calculations.
As an institutional-grade pallet rack manufacturer, HEDA Shelves operates a fully integrated, vertically controlled production line in Haizhu District, Guangzhou. Our production facility transforms structural hot-rolled sheet coil into ultra-rigid upright columns, box step beams, and structural decking. Holding certified verification including CE (Certificate No. 2435-CPR-8605159), ISO 9001:2015 Quality Management (No. 18624Q00169R0M), and complete RoHS Compliance, every rack profile strictly adheres to European standard EN 15512 (Steel Static Storage Systems) and Australian Standard AS 4084-2012.
Civil Defense Approval
Architectural 2D CAD layouts and 3D FEA stress models detailing flue spaces, sprinkler penetrations, and egress aisles tailored for local regulatory audits.
10-Stage Surface Treatment
Acid pickling, phosphating, and electrostatic epoxy-polyester thermo-curing engineered specifically for high-humidity coastal zones and chilled chambers (-30°C).
Traceable Q235B / Q355B Steel
Mill test certificates (MTC) supplied with every batch. Optimized yield strengths guarantee load deflection rates well within European limits (L/200).
Global Container Logistics
Direct export through Jebel Ali, Khalifa, Dammam, Jeddah, Shuwaikh, Sohar, and Hamad ports with tagged structural bundling matching erection guides.
High-Density Storage Architecture Matrix & Specification Data
Selecting the optimal pallet storage typology requires aligning structural safety margins, cubic space utilization, SKU differentiation, and handling cycle times.
| Racking Topology | Floor Space Utilization | Pallet Accessibility | Standard Load Envelope | Handling Equipment Required | Recommended Velocity Tier |
|---|---|---|---|---|---|
| Selective Pallet Racking | 40% – 50% | 100% Direct Access (Fastest) | 1,000 – 4,500 kg per beam level | Standard Counterbalance, Reach Truck | High SKU Variance / Rapid Turnover |
| Drive-In / Drive-Through | 65% – 75% | LIFO / FIFO (Batch Gated) | Up to 1,500 kg per pallet lane | Counterbalance, High-Mast Reach | Low SKU Variance / Cold Rooms |
| Radio Shuttle Automation | 75% – 85% | Flexible FIFO & LIFO | Up to 2,000 kg per shuttle cart | Standard Forklift + Automated Carrier | High Volume Distribution & Cold Storage |
| Gravity Flow Racking | 70% – 80% | Strict FIFO (Gravity Incline) | 800 – 1,500 kg per roller line | Dedicated Infeed & Retrieval Forklifts | Perishable Food, Dairy, Fast FMCG |
| Rack-Supported Mezzanine | 90% – 100% (Vertical) | Mixed (Pallet Base + Manual Pick) | 300 – 1,000 kg/m² upper deck | Order Pickers, Vertical Cargo Lifts | E-commerce, Auto Parts, Spare Units |
Structural Roll-Forming Precision
All vertical upright columns are cold-rolled continuously through a 24-station automated rolling line. CNC multi-hole hydraulic perforations allow beam adjustments at 75mm or 50mm increments while retaining maximum section modulus under extreme axial compression.
Dynamic Thermal Accommodation
For installations spanning ambient (45°C ambient warehouse environments) to blast-freezer temperatures (-30°C), HEDA utilizes micro-alloyed high-ductility steels preventing cold-embrittlement while maintaining structural elasticity and dynamic impact resistance.
Seismic & Slab Anchoring Rigor
Structural calculations accommodate concrete slab thickness variations (150mm to 250mm). High-tensile chemical anchors or mechanical expansion bolts are engineered to dissipate lateral forklift impact loads without compromising slab integrity.
Future Procurement Trends in Industrial Storage Engineering
How supply chain executives, warehouse developers, and procurement heads are modernizing physical infrastructure to meet next-generation supply demands.
Total Cost of Ownership (TCO) vs Capital Outlay
Procurement teams are shifting away from lowest-initial-bid acquisitions toward total asset lifecycle evaluation. Investing in superior epoxy coatings, heavy-gauge baseplate protectors, and reinforced wrap-around column guards substantially cuts operational rack remediation costs and downtime caused by inevitable forklift impact.
Modular Automation & Shuttle Readiness
Rather than committing massive capital to rigid, fully automated AS/RS facilities, logistics operators are prioritizing modular, shuttle-ready channel racking. These semi-automated configurations allow phased integration of automated guided vehicles (AGVs) and radio shuttles without structural teardowns.
Digital Twins & Pick-to-Light Integration
Modern procurement contracts mandate integration points between racking structures and warehouse management systems (WMS). Electronic shelf labeling, Sophia Pick-to-Light hardware, and IoT deflection-monitoring sensors are transforming static steel structures into interconnected, paperless fulfillment arrays.
The Evolution of Structural Warehouse Racking: 2026 and Beyond
The transition from passive steel frameworks to high-performance structural systems designed for carbon optimization, robotic interfacing, and extreme resilience.
Green Cold-Formed Steels
Adoption of low-carbon, scrap-recycled green steel profiles meeting corporate ESG and LEED warehouse building criteria without compromising yield strength or safety factors.
High-Bay Clad Buildings
Elimination of separate structural building skeletons: Racking frames themselves serve as the primary roof and wall support structures, slashing construction lead times by 35%.
Micro-Deflection Tolerances
Tighter fabrication tolerances (EN 15620 Class 100/200) specifically built for high-speed automated storage and retrieval system (ASRS) cranes operating up to 40 meters.
Intelligent Impact Sensors
Integrated structural telemetry tags that automatically ping maintenance engineers over BLE or LoRaWAN whenever a forklift collision exceeds allowable dynamic thresholds.
Warehouse Storage Rack Procurement: Frequently Asked Questions
Essential guidance for procurement managers, structural consultants, and logistics directors evaluating turnkey racking tenders.
What specific parameters are mandatory to initiate a structural 3D CAD design?
To produce an engineered 2D CAD layout and 3D FEA rendering, our structural engineering department requires: (1) Architectural building layout (.DWG format) with clear heights under eaves, lighting, and HVAC obstructions; (2) Concrete slab specification (thickness, compressive strength, rebar density); (3) Pallet dimensions (Width × Depth × Height including cargo overhang) and maximum gross weight; (4) Forklift truck operational specification (turning radius, maximum mast elevation, collapsed mast height); and (5) Inventory classification and SKU rotation philosophy (FIFO vs LIFO).
How does CE certification (EN 15512) safeguard commercial procurement?
CE Certification (such as HEDA’s Certificate No. 2435-CPR-8605159) under Construction Products Regulation (CPR) verifies that structural calculations, cold-forming processes, weldments, and mechanical properties meet strict European unified safety standards. In contrast to uncertified racking that frequently suffers catastrophic weld failure or localized upright buckling under peak loads, certified racking undergoes exhaustive physical destructive testing, ensuring verified safety margins (typically a minimum factor of 1.5 to 2.0 against yield).
How do finishing treatments prevent coating degradation in coastal or cold-store zones?
Standard paint finishes rapidly delaminate and rust when exposed to extreme coastal humidity (such as UAE, Saudi Arabian, or Southeast Asian ports) or chilled condensation (-25°C). HEDA executes an intensive 10-step surface pretreatment involving acid pickling (clearing all scale/oil) and chemical zinc phosphating. This is sealed with high-adhesion electrostatic polyester powder coating cured at 200°C. For open-air lumber/pipe yards or extreme corrosive chemical facilities, hot-dip galvanization to ISO 1461 is available.
Can your warehouse layouts directly support Civil Defense & FM Global approvals?
Yes. Our engineering drawings provide detailed longitudinal and transverse flue space dimensions (typically 150mm minimum), accurate rack-to-wall separations, designated emergency egress pathways, and fire sprinkler drop clearances conforming directly to NFPA 13 (Standard for the Installation of Sprinkler Systems) and Civil Defense fire safety codes. This documentation streamlines structural third-party reviews and insurance policy validation.
What packaging techniques are applied to mitigate damage during ocean shipping?
Exporting structural steel requires rigorous transport packaging to withstand container motion and humidity shifts. HEDA bundles structural uprights and step beams with protective wooden runners, corrugated cardboard buffering, and heavy-duty polyester strapping. Individual packages are labeled with distinct alpha-numeric tags cross-referenced to the master installation blueprint, enabling fast customs deconsolidation and systematic on-site staging.
What installation and structural supervisory assistance is available?
Every shipment is accompanied by comprehensive mechanical assembly drawings, torque-setting tables, beam safety pin verifications, and component bill-of-materials. For local mechanical contractors, we provide real-time remote video engineering support. For large-scale multi-tier mezzanines, automated shuttle tracks, and complex VNA systems, senior HEDA field supervisors can be deployed on-site to oversee positioning, leveling, plumbing, and anchoring validation.
Ready to Engineer Your High-Density Storage Facility?
Submit your facility floor plans or storage specifications today. Receive a free engineering assessment, customized 2D CAD layout, 3D visual rendering, and factory-direct quotation within 24 hours.
Send an Inquiry