Engineered Industrial Racking & Shelving Systems
From versatile retail gravity merchandising to high-density heavy-duty pallet systems rated up to 4,000 kg per level, our cold-formed certified steel storage solutions deliver optimal volumetric efficiency and total load safety across global logistics hubs.
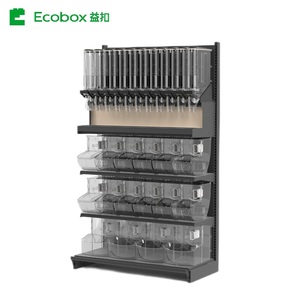
Ecobox Matching Iron Display Rack with Bulk Food Bins Gravity Bins for Supermarket Stand Display
Integrated iron merchandising fixture optimized for dry goods, grains, and zero-waste supermarket aisles. Built with certified food-grade contact brackets, heavy-duty powder coating, and precision gravity-feed dispensing slots.
- Material: Q235 Cold Rolled Iron + Acrylic
- Application: Supermarket Bulk Displays
- Capacity: 150–300 kg / tiered level
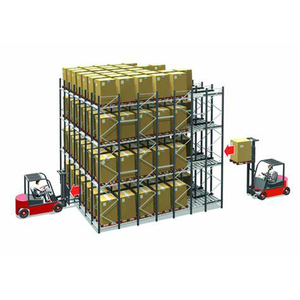
Warehouse High Density Gravity Roller Pallet Flow Racking
Dynamic gravity-fed roller lane system designed for strict First-In, First-Out inventory control. Features integrated centrifugal speed controllers, impact brake rollers, and entry guides ideal for food, beverage, and pharmaceutical cold stores.
- Operation: Automatic Gravity Flow (FIFO)
- Lane Depth: 2 to 20 Pallets Deep
- Braking: Self-Energizing Centrifugal Rollers
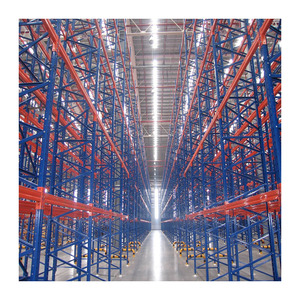
Mracking Heavy Duty Industrial Palletized Racking with a Capacity of 1000-4000kg Industrial Storage Racking
Engineered for extreme loading demands with box-beam profiles and slotted omega uprights. Certified for 1,000 kg to 4,000 kg per beam level with safety clip interlocks, seismic-grade baseplates, and abrasion-resistant polyester finish.
- Load Range: 1,000–4,000 kg / Beam Tier
- Steel Grade: Q235B / Q355B Certified
- Pitch Step: 50 mm / 75 mm Adjustable
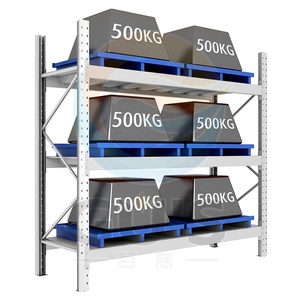
Factory Outlet Adjustable Warehouse Pallet Racking Heavy Pallet Rack Heavy Storage Rack Warehouse Storage Selective Pallet Rack
Direct 100% selectivity rack configuration facilitating immediate accessibility to every single pallet position. High-strength interlocking connectors ensure zero frame distortion under sustained dynamic forklift loading.
- Accessibility: 100% Individual Pallet Access
- Configuration: Single or Back-to-Back Row
- Forklift Class: Counterbalance, Reach, VNA
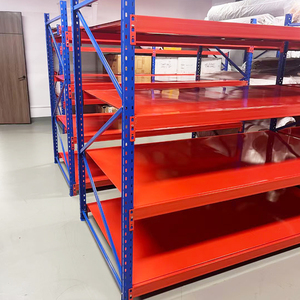
High Effective 5 Metal L2500*W1100*H2550mm 1000kg-4000kg Heavy Duty Corrosion Protection Warehouse Storage Racking Push Back
Telescoping nested cart system riding on inclined structural steel channel rails. Eliminates dedicated drive-in entry aisles while boosting storage density by up to 75% under a dependable Last-In, First-Out (LIFO) inventory cycle.
- Dimensions: L2500 x W1100 x H2550mm (Custom)
- Pallet Density: 2 to 6 Pallets Deep
- Coating: Salt-Spray Anti-Corrosion Treated
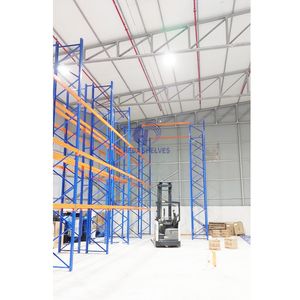
Warehouse Heavy Duty Beam Pallet Racking System for Large Scale Warehouses and Industrial Storage
Engineered for large-scale logistics fulfillment centers and raw manufacturing hubs. Incorporates double-C roll-formed welded step beams, reinforced column footplates, and optional wire mesh decking or steel pallet support bars.
- Frame Profile: Up to 120 x 95 mm Uprights
- Beam Section: 80–160 mm Box / Step Beam
- Compliance: EN 15512, RMI, AS4084 Certified
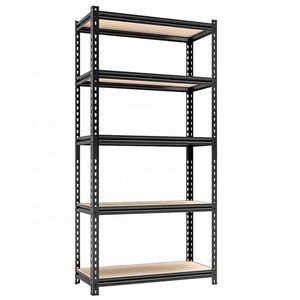
60" H X28 W X12 D 5-Shelf Rack Industrial Steel Adjustable Heavy-Duty Tall Shelving Units Black Boltless Racking Warehouse Use
Rapid snap-together boltless steel shelving engineered for manual parts picking, distribution bin replenishment, and archive storage. Features heavy-gauge steel uprights and adjustable shelves without hardware or loose fasteners.
- Dimensions: 60" H x 28" W x 12" D (Standard)
- Assembly: 100% Boltless Keyhole System
- Shelving Deck: Solid Steel Panel / Wire Mesh
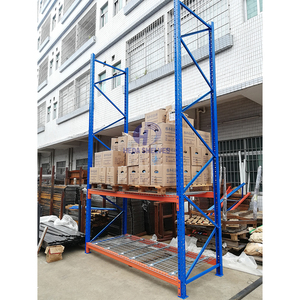
High Bay Heavy Duty Selective Pallet Racking System for Tall Warehouses and Industrial Storage
Ultra-tall narrow-aisle (VNA) system engineered for ceiling heights reaching up to 16+ meters. Maximizes vertical cube volume while integrating laser-aligned bottom floor guide rails or inductive wire guidance for automated reach trucks.
- Vertical Height: Up to 18 meters single-frame
- Aisle Width: 1.6m – 1.9m Narrow Aisle
- Volumetric Gain: +45% cubic warehouse gain
Guangzhou Heda Shelves Co., Ltd.: Engineering Authority Since 2001
Headquartered in Guangzhou with a dedicated 30,000 square meter fabrication infrastructure and 300+ technical personnel, HEDA Shelves provides true tier-1 OEM and ODM manufacturing capabilities for high-performance industrial shelving, selective racking, and integrated mezzanine flooring.
Certified Global Compliance
Every structural profile is strictly calculated and third-party certified under CE (No. 2435-CPR-8605159), ISO 9001:2015 Quality Management (No. 18624Q00169R0M), RoHS compliance, and conforms with European EN 15512, FEM 10.2.02, and American RMI MH16.1 codes.
Free 2D CAD & 3D Modeling
Our senior structural team provides complete 2D layout drafting, aisle-clearance optimization, Civil Defense approval documentation, and photorealistic 3D warehouse renderings at zero cost prior to contract finalization, preventing costly site installation clashes.
Extreme Climate Resilience
Equipped with specialized 8-stage pickling, phosphating pretreatment, and electrostatic thermosetting powder coat lines. Engineered specifically to eliminate paint peeling, rust creeping, and joint oxidation in severe coastal humidity, extreme heat, and ambient salt air environments.
Container-Optimized Logistics
Direct export logistics out of Guangzhou port serving Jebel Ali, Dammam, Jeddah, Hamad, Sohar, Long Beach, and Rotterdam. Shipments feature bundle barcoding matching layout blueprints, minimizing sorting delays and lowering structural erection costs.
Our Proprietary 10-Step Precision Manufacturing Process
True structural reliability requires unified in-house execution. We control every metallurgical, mechanical, and surface chemistry stage under a single roof to guarantee uniform tensile properties and load deflection tolerances under 1/200th of clear span.

Raw Materials
Certified high-tensile Q235B and Q355B steel strip coils tested for yield strength and ductility.

Precision Cutting
CNC slitting lines cut raw sheet steel with micron-level edge accuracy to eliminate stress burrs.

Column Punching
Automated punch presses stamp 50mm and 75mm pitch diamond and teardrop slots with zero deviation.

Cold Bending
Heavy hydraulic CNC presses bend support angles, baseplates, and bracket reinforcements.

Roll Forming
Continuous multi-station cold-rolling lines shape complex upright omega and box-beam sections.

Surface Polishing
Automated deburring and mechanical polishing smooth joints to ensure 100% uniform powder adhesion.

Robotic Welding
Gas metal arc robotic stations weld beam connectors and baseplates with deep penetration.

Acid Pretreatment
Full dip chemical tanks pickle, degrease, and phosphate steel, neutralizing rust inhibitors.

Powder Coating
Automated electrostatic spray booths apply 60–100 μm heavy epoxy-polyester coatings cured at 200°C.

QC & Export Packing
Final load deflection tests, thickness checks, barcode labeling, and protective sea-worthy bundling.
Industrial Racking System Comparison: Density, Access & Capex
Selecting the correct storage geometry depends on your inventory velocity, SKU profile counts, forklift mast capabilities, and structural floor slab capacity. Evaluate key performance trade-offs below:
| Racking Architecture | Direct Selectivity | Floor Space Use | Rotation Principle | Typical Capacity / Bay | Forklift Compatibility | Capex Index |
|---|---|---|---|---|---|---|
| Standard Selective | 100% (Instant) | 40% – 50% | FIFO or LIFO | 1,000 – 4,500 kg | Standard Counterbalance / Reach | Baseline (Low) |
| Gravity Pallet Flow | Limited (Face SKU) | 75% – 85% | Strict FIFO | 1,000 – 3,000 kg | Standard Counterbalance | High / Automated |
| Push-Back Carts | Moderate (Lane Face) | 70% – 80% | Strict LIFO | 1,000 – 3,500 kg | Reach Truck / Heavy Forklift | Medium-High |
| High Bay VNA | 100% (Instant) | 65% – 75% | FIFO or LIFO | 2,000 – 4,000 kg | Turret Truck / Articulated VNA | Medium |
| Radio Shuttle Cart | High by Level | 85% – 90% | Flexible FIFO / LIFO | 1,500 – 2,500 kg | Standard Reach + Semi-Auto Shuttle | High Performance |
| Multi-Tier Mezzanine | 100% (Piece Pick) | Up to 250% (Cubic) | Omni-Channel Picking | 300 – 1,000 kg/m² | Manual Cart / Vertical Lift (VRC) | Medium-High |
Future Procurement Trends Transforming Industrial Warehousing
Warehouse managers and global supply chain directors are moving away from commodity rack purchasing toward total lifecycle value, modular scalability, and carbon-aware supply chain compliance. Stay ahead of these industry transformations:
Real Estate Densification & VNA High-Bay Scaling
With industrial square meter leasing costs hitting historic highs across North America, Europe, and GCC dry ports, greenfield and brownfield facilities are universally prioritizing vertical clear height. The demand for narrow-aisle selective frames exceeding 12 to 16 meters has expanded by over 38% since 2023, shifting procurement priority toward high-tensile upright stiffness and sub-millimeter floor anchoring accuracy.
Cold Chain Decarbonization & Shuttle Density
Refrigerated and blast-freezer cubic meters consume up to 6 times more electrical power than ambient storage. Procurement teams are rapidly replacing low-density selective configurations in cold storage with deep-lane semi-automated Radio Shuttle and Gravity Flow designs. Compressing 3,000 pallet positions into 40% less chilled volume yields massive recurring power savings and supports corporate ESG targets.
Automation-Ready & AMR-Interfacing Tolerances
Traditional manual forklifts accept minor beam deflection and floor variances; however, Autonomous Mobile Robots (AMRs), automated pallet shuttles, and Automated Storage and Retrieval Systems (ASRS) demand beam deflection limits strictly engineered to $L/300$ or better. Procurement contracts increasingly mandate laser-surveyed frame straightness, certified floor shimming, and integrated target reflective markers.
Supply Chain Traceability & Circular Steel Specs
Tier-1 multinational general contractors and logistics REITs now enforce full metallurgical traceability. Procurement managers require mill test certificates (MTCs) verifying chemical compositions (Carbon, Manganese, Silicon) and yield ratings ($\ge 235\text{ MPa}$ to $355\text{ MPa}$). Closed-loop zero-effluent chemical pretreatment and heavy, low-VOC TGIC-free powder finishes are becoming mandatory procurement prerequisites.
Engineering & Technological Advancements in Modern Racking
HEDA Shelves invests continuous R&D capital into metallurgical optimization, nonlinear Finite Element Analysis (FEA), and dynamic impact absorption systems. Our cutting-edge advancements safeguard warehouse lives and high-value customer stock:
Nonlinear FEA Stress Modeling
Utilizing high-performance 3D structural simulation software conforming to European FEM 10.2.02 and US RMI standards. Every custom OEM column section undergoes simulated axial compression, lateral wind shear, and seismic ground acceleration tests to identify torsional micro-buckling points prior to tooling manufacture.
Kinetic Forklift Impact Deflection
Upright damage accounts for 85% of warehouse structural failures. We have engineered polymer-core heavy steel corner column protectors and wraparound floor-bolted bullnose shields capable of dissipating accidental 400 J dynamic vehicle impacts without translating kinetic shear stress directly into the frame vertical axis.
Multi-Rib Cold Form Profile Geometries
By transitioning from traditional simple channels to proprietary 12-bend continuous roll-formed upright profiles, our engineers have increased section moment of inertia by 22% while conserving raw steel weight. This achieves higher load ratings with lower freight shipping weights for our global project buyers.
Integrated IoT Structural Telemetry
Pioneering the integration of low-power wireless strain-gauge sensors and load cells directly inside critical beam connection nodes. Enables real-time deflection reporting to the warehouse facility management dashboard, identifying localized overloading and accidental frame collisions instantly.
Frequently Asked Technical & Procurement Questions
Procurement managers, warehouse directors, and engineering EPC contractors ask us these critical questions when specifying custom OEM warehouse racking:
What essential warehouse technical parameters are required to generate a free 3D & CAD layout design? +
How does HEDA Shelves guarantee steel quality and verify beam deflection load limits? +
How do your racking systems withstand corrosive environments like coastal regions and cold stores? +
Can your engineering designs satisfy local Civil Defense, NFPA fire sprinkler, and seismic building codes? +
Can you manufacture non-standard sizes, custom OEM punching patterns, and corporate color branding? +
What are the typical manufacturing lead times, export packing protocols, and container load efficiencies? +
What on-site installation guidance, supervision, and project support do you supply? +
What structural warranties and post-installation service lifecycles do you offer? +
Planning a Warehouse Racking Upgrade or New Distribution Center?
Connect directly with our senior racking engineering department. Provide your facility parameters or hand sketch, and we will deliver an optimized structural 2D CAD layout, comprehensive load calculation report, and factory-direct OEM price quotation within 24 hours.
- Free 2D CAD & 3D Photorealistic Layout
- Direct Guangzhou Factory Pricing (No Broker)
- CE, ISO 9001 & RoHS Certified Safety
- Full Ocean Freight Logistics Support
Engineering Consultation
Speak live with our structural applications team to verify your pallet weights, beam profiles, and building clearances.
Contact Us