Industrial Pallet Racking & High-Density Storage Solutions
Explore our factory-direct, heavy-duty warehouse storage systems. Designed with finite element analysis (FEA) and fabricated from certified high-tensile structural cold-rolled steel coils.
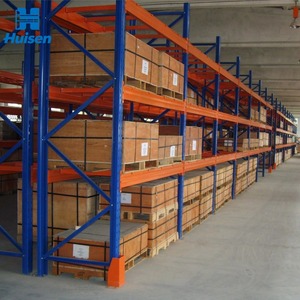 3,000 kg / Tier
Custom Heavy Duty Shelving 3000 Kg Layer Garage Customized Tier Warehouse Storage Metal Stacking Shelf
- Load Capacity: Up to 3,000 kg/level
- Material: Q235B High-Yield Steel
- Beam Section: Dual C-Profile Welded Box
- Finish: Thermoset Epoxy Powder
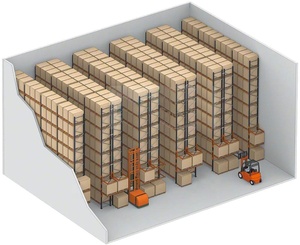 VNA High-Bay
URGO Very Narrow Aisle Pallet Rack / VNA High-Density Racking System
- Aisle Width: 1,500 mm – 1,800 mm
- Max Height: Up to 15,000 mm (15m)
- Access Efficiency: 100% Direct Selectivity
- Floor Guidance: Mechanical Rail or Wire
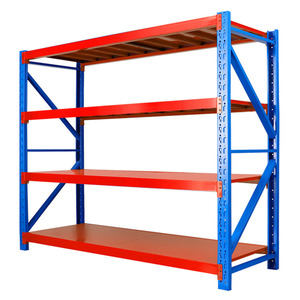 Modular Boltless
China Factory Warehouse Metal Pallet Racking Systems Easy-to-Install Boltless 5 Layer Steel Units
- Assembly: 100% Interlocking Boltless
- Pitch Adjust: 50mm or 75mm increments
- Deck Options: Steel / Mesh / MDF
- Corrosion Proof: Pickling & Phosphating
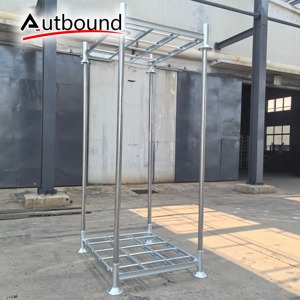 Demountable / Post
Heavy Duty Steel Stackable Pallet Stacking Racks Post Pallet Storage Shelf For Warehouse Storage
- Stacking Height: 4 to 6 units high
- Unit Capacity: 1,000 kg – 2,500 kg
- Post Configuration: Removable / Collapsible
- Base Frame: Robotic Mig-Welded Tube
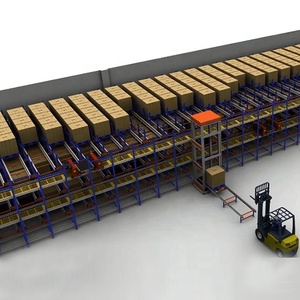 Semi-Automated AS/RS
Automatic Radio Shuttle Rack System Heavy Duty Industrial Warehouse Storage Shelf Racking CE Certified
- Lane Depth: Up to 40 Pallets Deep
- Fulfillment Logic: FIFO / LIFO Switching
- Shuttle Speed: 0.8 – 1.1 m/s (loaded)
- Battery Tech: LiFePO4 Quick-Charge
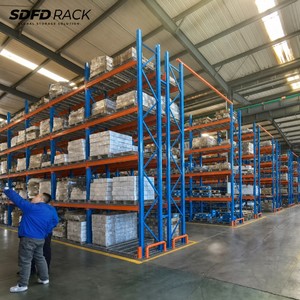 Adjustable Heavy Beam
Adjustable Customized 5 Level Heavy Duty Industrial Pallet Racking with Solid Steel Shelves
- Load Range: 1,500 – 4,500 kg / Tier
- Upright Section: 90mm, 100mm, 120mm
- Shelf Panelling: Ribbed Steel Deck Sheets
- Safety System: Locking Drop-Pins
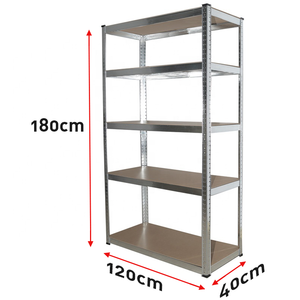 Extra-Tall Shelving
6-Tier Powder Coated Extra Tall Metal Shelving 222x90x40cm 200kg Hand-Loaded Storage Rack
- Dimension: 2220H × 900W × 400D mm
- Per Tier Load: 200 kg Uniform Distributed
- Application: E-Commerce / Spare Parts
- Column Style: Angle-Steel Rolled Profile
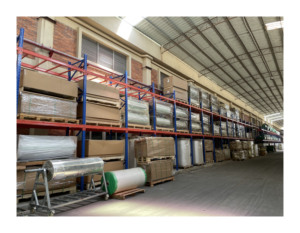 Hot-Dip Galvanized
Galvanized Steel Standard Size Warehouse Heavy Duty Selective Pallet Racking for Cold Storage & Outdoors
- Protection: HDG (ISO 1461 Coating)
- Temperature Range: -35°C Cold Store to +55°C
- Standard Sizes: Customized to Euro/US Pallet
- Impact Guard: Reinforced Base Wraps
Turnkey OEM/ODM Engineering & Factory Infrastructure
Guangzhou Heda Shelves Co., Ltd. operates a premier 30,000 m² production facility in Guangdong, producing more than 30,000 metric tons of certified structural steel storage racking per month for 120+ nations worldwide.
25+ Years Industrial Mastery
Founded in 2001, we provide deep metallurgical knowledge and manufacturing capability for global supply chains, port logistics, cold-chain operations, and distribution complexes.
Complimentary 3D & CAD Design
Our 300+ in-house technical engineers calculate live loads, seismic drift limits, and forklift sweep paths, returning fully coordinated 2D layout schematics and photorealistic 3D models.
CE, ISO & RoHS Certified
Strict quality assurance governed under CE Certificate No. 2435-CPR-8605159 and ISO 9001:2015 (Valid through 2027). Every batch is audited with digital ultrasonic flaw testers and tensile gauges.
Tailored OEM/ODM Flexibility
We tailor hole punching patterns (50mm, 75mm, 76.2mm teardrop), custom RAL electrostatic finishes, cold-formed structural box beams, and specialized baseplates for regional building codes.
Our Integrated 10-Step Manufacturing Process
Total internal production ownership ensures batch-to-batch structural integrity, zero subcontracted roll-forming variance, and absolute corrosion defense.
Raw Material Test
Spectrometric testing of Q235B and Q355B coils from certified tier-1 steel mills.
Precision Slitting
Automated uncoiling, decoiling, and CNC slitting into high-tolerance structural strips.
Continuous Punch
50-ton hydraulic high-speed CNC punching presses for 50mm and 75mm pitches.
Roll-Forming
Multi-stand automated cold-roll forming lines shaping precision Omega uprights.
Profile Sizing
Automated flying hydraulic saws cutting beam channels and columns to exact CAD lengths.
Surface Polishing
Automated shot-blasting and mechanical de-burring to remove slag and mill scale.
Robotic Welding
Dual-station robotic Panasonic CO2 shielded arc welding for beam connectors.
Pickle & Phosphate
9-stage chemical wash, acid rust removal, and zinc-phosphate pre-treatment dip.
Powder Coating
GEMA electrostatic powder guns applying 60-90μm epoxy cured in 200°C baking tunnels.
QC & Sea Packing
Coating thickness check, bundle strapping, and containerization with moisture barriers.
Standard Industrial Racking Structural Parameters
Comparing beam profiles, upright geometries, deflections, and load ratings across selective, drive-in, radio shuttle, and cantilever configurations under EN 15512:2020 and RMI MH16.1 specifications.
| Racking Type | Upright Profile (mm) | Box Beam Profile (mm) | Max Load per Tier | Floor Space Utilization | Operational Selectivity |
|---|---|---|---|---|---|
| Standard Selective Pallet Racking | 90×68×2.0 / 100×68×2.0 | 80×50×1.5 to 160×50×2.0 | 1,000 – 4,500 kg | 40% – 45% (Wide Aisles) | 100% (Instant Individual Access) |
| Very Narrow Aisle (VNA) Racking | 100×68×2.0 / 120×95×2.5 | 100×50×1.5 to 160×50×2.0 | 1,500 – 4,000 kg | 60% – 65% (1.6m Aisle Width) | 100% (High-Reach Turret Truck) |
| Drive-In / Drive-Through Racking | 90×68×2.0 / 100×68×2.5 | Cantilever Support + Guide Rail | 1,000 – 1,800 kg/pallet | 70% – 75% (Eliminates Aisles) | LIFO or FIFO (Batch SKUs) |
| Automated Radio Shuttle Racking | 90×68×2.0 to 120×95×3.0 | Specialized Cold-Formed Shuttle Rail | 1,500 kg per pallet | 80% – 85% (Continuous Deep Lanes) | Automated LIFO / FIFO |
| Heavy Duty Cantilever Racking | 200×100×4.0 to 350×150×6.0 H-Beam | Tapered Arm: 80×60 to 160×80 | 800 – 3,000 kg per arm | Open front for long goods | 100% Access for pipes, timber, steel |
| Multi-Tier Mezzanine Platform | Square Tube / Heavy Box Column 150×150 | Primary/Secondary H-Beam Truss | 300 – 1,000 kg / m² | Multiplies floor area 200%–300% | Integrated picking, conveyor, office |
Structural Deflection and Deflection Limits (L/200 vs L/300)
In structural warehouse engineering, structural compliance is governed by the maximum allowable vertical deflection of the load beam under full design load. According to European standard EN 15512:2020 and American ANSI/RMI MH16.1, the vertical deflection ($\delta$) of any load-bearing pair of beams supporting uniformly distributed pallet loads (UDL) must not exceed $L/200$ of the clear beam span ($L$). For automated systems, including Radio Shuttle and Crane-Served High-Bay AS/RS, our engineering team standardizes on a stricter rigidity limit of $L/300$ or $L/350$.
This prevents optical sensor misalignments, floor guide disengagement, and premature mechanical fatigue on the roll-formed hooks. Each beam end-connector is precision-welded with a minimum 3-claw or 4-claw configuration and fitted with electro-galvanized spring locking safety pins (capable of withstanding an upward shear force exceeding 5,000 N without failure) to eliminate beam dislodgement caused by improper forklift operation.
Emerging Warehouse Racking Procurement Trends
How industrial real estate costs, supply-chain re-shoring, and automated material handling are reshaping B2B purchasing criteria through 2025–2035.
TCO Over Initial Capital Expenditure
Global logistics operators are replacing lowest-bid procurement with Total Cost of Ownership (TCO) assessments. Specifying heavier steel wall gauges (e.g., 2.0mm vs. 1.8mm uprights) and dual-layer thermoset powder finishes drastically mitigates rack deflection incidents, operational downtime, and costly structural repairs caused by industrial reach truck impacts.
Factory-Direct OEM/ODM Disintermediation
Procurement directors increasingly bypass regional intermediaries to partner directly with primary manufacturing factories like Heda Shelves. Direct OEM contracts eliminate distributor markups, allow bespoke punch profiling (matching existing historical warehouse installations), and accelerate engineering revisions for project-specific submittals.
Pre-Approved Fire & Seismic Engineering
Tougher municipal civil defense policies, NFPA 13 sprinkler clearance rules, and Eurocode 8/IBC seismic criteria require verified static structural calculations before warehouse ground-breaking. Procurement contracts now demand certified engineering packages, verified baseplate anchor pull-out ratings, and precise longitudinal/transverse flue space allowances.
Industrial & Technological Trends in Storage Fabrication
Explore how robotic roll-forming lines, automated material handling synergies, and green metallurgical standards are redefining modern warehouse racking systems.
AS/RS & AMR Integration
Traditional static storage is rapidly converging with Autonomous Mobile Robots (AMRs) and Automated Storage and Retrieval Systems (AS/RS). Modern racking layouts feature continuous guide-rails, laser-guided vehicle (AGV) docking tolerances within ±1.5mm, and shuttle runways designed for dynamic cycling loads.
IoT Structural Health Telemetry
Sensors and digital-twin software are entering high-bay logistics. Strain gauges embedded on lower upright sections and vibration-sensing impact collars track reach-truck collisions, overloading, and seismic settlement in real-time, giving plant managers preventative alerts before catastrophic rack collapse occurs.
Sub-Zero Cold Chain Metallurgical Advances
Cold storage facilities (-25°C to -35°C) face steel embrittlement risks. Advanced production uses high-toughness micro-alloyed steels with verified Charpy V-notch impact values at sub-zero temperatures, paired with anti-condensing electrostatic formulations to prevent micro-fissuring and subsurface peeling.
Circular Economy & Low-Carbon Steel
Driven by corporate ESG benchmarks, tier-1 OEMs are shifting toward scrap-based Electric Arc Furnace (EAF) steel coils, low-VOC powder coatings, and modular, demountable bolted connections that facilitate warehouse relocation, repurposing, and total metal recycling at end-of-life.
Frequently Asked Questions for Warehouse Racking Buyers
Answers to critical questions regarding engineering parameters, steel specifications, shipping logistics, and compliance submittals.
What is the structural difference between Q235B and Q355B steel in racking design?
Q235B is a standard low-carbon structural steel with a yield strength of 235 MPa, ideal for ambient selective pallet racking and light-to-medium industrial shelving. Q355B is a high-strength low-alloy structural steel with a minimum yield strength of 355 MPa and higher tensile capacity (470–630 MPa). Q355B allows for reduced wall thicknesses while handling extreme loads, making it the preferred choice for heavy VNA uprights, cantilever columns, automated shuttle rails, and earthquake-prone seismic zones.
How are transverse and longitudinal flue spaces accounted for in CAD layouts?
Per fire protection safety codes (including NFPA 13 regulations), back-to-back pallet racking rows must maintain clear vertical openings (flue spaces) through which heat and sprinkler water can flow. A minimum 75 mm to 150 mm (3 to 6 inches) longitudinal flue space between back-to-back rows is maintained using rigid heavy-gauge steel row spacers. Transverse flue spaces (between individual pallet positions along the beam) are engineered by adding 75–100 mm clearances on each side of the pallet when calculating total clear beam span.
How does the surface pre-treatment prevent corrosion in humid coastal ports or cold stores?
Standard solvent wiping leaves oil residue that degrades coating adhesion. Our factory uses an automated continuous 9-stage immersion system: hot alkaline degreasing, clean water rinse, sulfuric acid pickling (derusting), surface conditioning, zinc phosphating, followed by demineralized rinsing and drying. The micro-crystalline zinc-phosphate conversion layer chemically locks into the steel, passing 500-hour ASTM B117 neutral salt spray tests and protecting cold storage systems against condensation and sub-zero thermal cycling.
Can you manufacture custom upright hole patterns to match existing warehouse systems?
Yes. As a genuine OEM/ODM manufacturing plant, our tool and die division builds custom punch tool sets for high-speed CNC punching presses. We manufacture European standard 50mm pitch, Australian/British 75mm and 76.2mm pitch, American Teardrop configurations, and Japanese diamond-hole profiles. Simply ship an upright sample or submit high-precision engineering drawings for cross-sectional profile matching and load testing.
What engineering data is required to generate an accurate 3D warehouse layout?
To prepare an optimized CAD floor plan and structural proposal, provide: (1) Warehouse architectural drawings showing clear heights under trusses, slab load capacities, and column grids; (2) Pallet specifications (width, depth, overall height including cargo overhang, and maximum pallet gross weight); (3) Material handling equipment (forklift brand, mast model, collapsed height, maximum lift height, and minimum turning radius); and (4) Operational target (total pallet capacity vs. required daily SKU throughput).
How are heavy-duty structural steel components protected during sea transport?
Overseas container transit requires robust strapping to avoid abrasion and maritime corrosion. Upright frames and beams are nested on heavy timber dunage runners, wrapped in air-cushioned polyethylene sheets, cross-banded with high-tensile steel banding, and fitted with heavy-gauge corner edge protectors. Small accessories (safety pins, footplates, shims, anchor bolts) are packed in heavy-duty wooden crates with desiccant pouches, matching the container packing sequence to your site assembly order.
Partner with a Direct OEM/ODM Racking Manufacturer
Looking to equip a new logistics center, replace obsolete industrial shelving, or expand your high-bay warehouse? Engage directly with our senior structural engineering department. We deliver complimentary 2D/3D CAD layout schemes, certified structural calculations, and competitive factory-direct pricing for international export.