Featured Heavy-Duty Pallet Racking Systems
Precision-engineered in our fully certified facility, serving cold-chain distribution, automotive spare parts, FMCG e-commerce fulfilment, and port terminals worldwide.
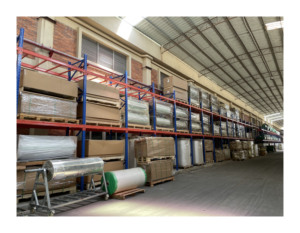 Heavy-Duty
Galvanized Steel Standard Size Warehouse Heavy Duty Selective Pallet Racking
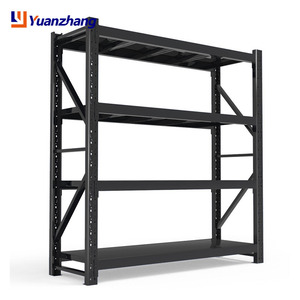 Wide-Span
Warehouse Wide Span Duty Racking Industrial Steel Storage Rack Coated Metal Shelves
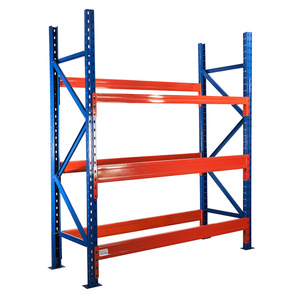 2000kg/Level
Wholesale Factory Heavy Duty Industrial Shelves 2 Tons Warehouse Pallet Storage Rack
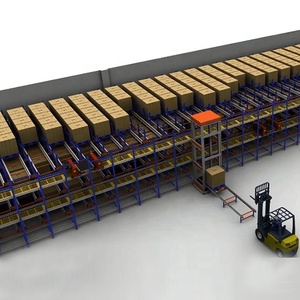 Automated
Automatic Radio Shuttle Rack System Heavy Duty Industrial Storage Shelf CE Certified
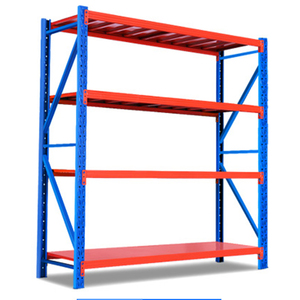 Boltless
HUAWU 200kg Per Layer Boltless Shelving System Steel Q235 Storage Rack HD036
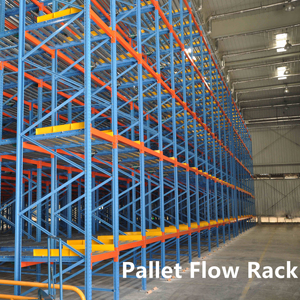 Dynamic Flow
Customized Gravity Flow Pallet Roller Shelf System Heavy Duty Pallet Flow Rack
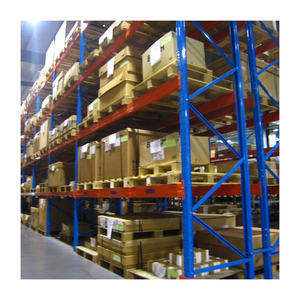 High Structural
Heavy Duty Rack Steel Warehouse Rack Industrial Pallet Storage Shelf System
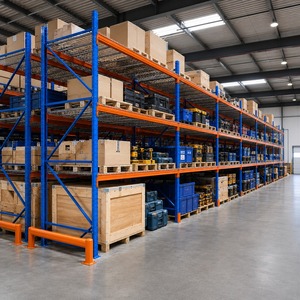 Logistics Hub
Factory Pallet Racks Q235B Steel Schwerlastregal for Logistics Hubs
Comprehensive Strategic Engineering Whitepaper: Industrial Pallet Racking Architecture & Global Procurement
As modern international supply chains encounter fluctuating material costs, hyper-accelerated cross-border e-commerce, and expanding automated fulfillment centers, industrial warehouse pallet storage racks have transitioned from static framing into complex, dynamic civil and logistical systems. Evaluating storage engineering requires scrutinizing structural metallurgical profiles, dynamic payload calculations, safety redundancies, corrosion protection coatings, and seismic response tolerances.
Engineering Core Focus: Selecting warehouse storage racks is fundamentally a structural integrity decision. A compliant facility prevents frame buckling, beam deflection exceeding 1/200th of clear span, and early structural fatigue from dynamic material handling impact.
Structural Metallurgy: The Standard of Cold-Formed Q235B and High-Yield Steel
The foundation of reliable racking fabrication lies in the consistent mechanical properties of structural strip steel. At HEDA Shelves, primary upright columns and structural box beams are roll-formed from cold-rolled steel (predominantly high-grade Q235B or equivalent yield strengths), ensuring yield tensile points exceeding 235 MPa with controlled ductility. Structural columns feature continuous multi-stage cold profile stamping and precision teardrop or omega pitch perforations (typically 50mm, 75mm, or 76.2mm increments) configured to allow rapid mechanical interlock with beam connectors.
Beam fabrication requires specialized twin-C reverse interlocking sections seam-welded to multi-claw end connectors. This connector claw geometry creates a clamping moment connection that tightens under downward pallet weight, minimizing rotational torsional deflection across extended clear spans up to 3900mm or longer for double-pallet configurations handling gross weights exceeding 2,000kg to 4,000kg per shelf tier.
Surface Metallurgy and Climate Adaptability for Harsh International Environments
For warehouse facilities located across aggressive climates—such as the high summer ambient heat exceeding 45°C, high dust loadings, and coastal relative humidity found throughout the Middle East, Southeast Asia, and coastal logistics nodes—conventional surface treatments deteriorate rapidly. Exposed steel oxidizes quickly, undermining load ratings.
Our integrated 10-step production protocol incorporates industrial pickling, phosphating baths, high-temperature de-greasing, ultrasonic water rinsing, and an automated electrostatic epoxy-polyester powder-coating cycle baked at 180°C–200°C. This molecular curing yields an inert polymer coating of 60–90 microns thickness with exceptional salt-spray, scratch, and impact resilience. For external bulk yards, cold storage freezers (-30°C), or harsh chemical distribution hubs, continuous hot-dip galvanization or high-durability zinc coatings provide total cathodic barrier protection against internal tubular corrosion.
Product Architecture Recommendations Across Distinct Industrial Topologies
Selecting an optimal pallet racking architecture depends directly on your SKUs, order volume, handling speed, and floor dimensions:
- Standard Selective Racking: Unrestricted 100% direct access to every SKU pallet. Ideal for third-party logistics (3PL) hubs, distribution facilities, and FMCG retailers balancing wide inventory variations with counterbalanced or reach truck operations.
- High-Density Drive-In / Drive-Through Systems: Maximizes volumetric floor space by cutting working aisles by up to 75%. Perfect for homogenous, bulk-manufactured goods, cold-chain blast freezers, and beverage hubs operating on Last-In-First-Out (LIFO) or First-In-First-Out (FIFO) batch shipping cycles.
- Automated Radio Shuttle Systems: Integrates electric shuttle carts running on dedicated guide rails inside deep storage lanes. Forklift drivers do not enter the rack structure, drastically accelerating pallet retrieval, minimizing frame impact damage, and maximizing cold-room thermal efficiency.
- Gravity Pallet Flow & Push-Back Racking: Gravity-fed flow beds lined with precision steel rollers and speed controllers ensure continuous First-In-First-Out stock turnover, ideal for pharmaceutical, perishables, and time-sensitive FMCG logistics.
- Structural & Rack-Supported Mezzanines: Exploits vertical clearance by stacking two to four levels of accessible walkways and picking platforms over heavy-duty upright frames, multiplying usable picking area without costly civil expansions.
Global Procurement Trends & Future Logistics Trajectories
Global procurement teams are shifting how they source and implement warehouse racking systems:
Automation & ASRS Compatibility
Racking systems are now engineered with tighter millimetre tolerances to accommodate automated guided vehicles (AGVs), laser-guided forklifts, automated pallet conveyors, and high-bay stacker cranes.
Turnkey Factory-Direct Integration
Enterprises are bypassing intermediary trading desks to partner directly with OEM/ODM manufacturers capable of supplying verified structural drawings, 3D BIM models, container packing, and technical installation documentation.
Modular Reconfiguration Capacities
Supply chains require modular racking frames with toolless beam adjustments and bolt-on accessories, allowing fast realignments as inventory profiles change.
Why Global Logistics Leaders Partner with HEDA Shelves
Direct manufacturer capabilities delivering certified quality, structural safety, and end-to-end engineering support.
25+ Years Industrial Heritage
Founded in 2001 in Guangzhou, HEDA Shelves brings over a quarter-century of focused engineering experience across warehouse storage racks, heavy-duty shelving, and structural mezzanine floors.
Free 2D CAD & 3D Layout Design
Our in-house structural engineers evaluate building clearances, column layouts, aisle requirements, slab load capacities, and forklift specs to generate compliant 2D CAD layouts and 3D visual renderings before production.
Verified CE & ISO 9001 Certifications
Quality management and structural performance certified under CE (Certificate No. 2435-CPR-8605159) and ISO 9001:2015 (Certificate No. 18624Q00169R0M), fully meeting municipal fire safety and Civil Defense review standards.
Full OEM/ODM Customization & Export-Ready Container Packing
Our 30,000 m² factory with 300+ technical personnel supports full custom column profiles, specialized steel grades, custom electrostatic RAL powder shades, and tailored component branding. Bundles are systematically labelled and banded to match installation erection drawings, ensuring trouble-free customs clearance and swift on-site assembly at ports worldwide, including Jebel Ali, Dammam, Jeddah, Hamad, Sohar, and Shuwaikh.
Frequently Asked Questions on Pallet Rack Procurement
Key technical, engineering, and logistics considerations for warehouse operators and supply chain managers.