Engineered Warehouse Pallet Racking Systems
Explore heavy-duty storage configurations designed, cold-roll-formed, and structurally engineered for maximum dynamic pallet deflection resistance, ultra-dense SKU handling, and seamless material handling integration.
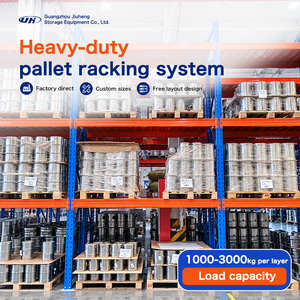
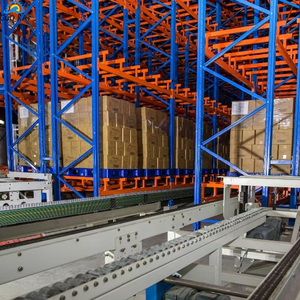
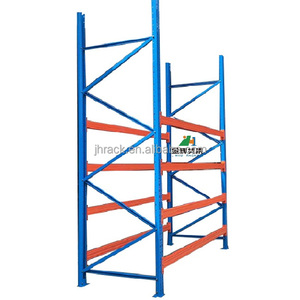
Industrial Heavy Duty Warehouse Racking System Steel Pallet Rack Adjustable Beam Storage System High Load Capacity
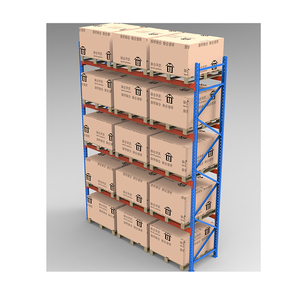
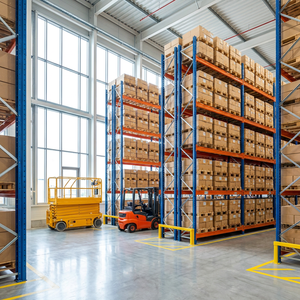
Warehouse Equipment Heavy Duty Pallet Rack Steel Storage Racking System Supplier
Custom Rackmount Storage Server Chassis 12 Bay LFF Hot Swap Drive Sheet Metal Enclosure OEM
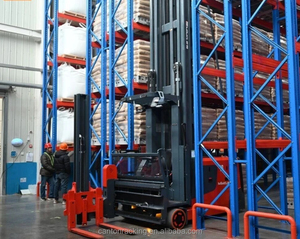
Top 10 Large Pallet Racking Manufacturers Worldwide
A rigorous comparative analysis of the world's premier pallet racking manufacturers, assessing fabrication capacity, seismic structural engineering compliance, automated roll-forming precision, and global supply chain reliability.
HEDA Shelves (Guangzhou HEDA Shelves Co., Ltd.)
Operating since 2001, HEDA Shelves is a recognized global giant with a dedicated 30,000 m² advanced fabrication complex and an exceptional monthly throughput of 30,000 tons. Renowned for its factory-direct engineering model, HEDA produces selective racking, drive-in systems, VNA, heavy-duty cantilever racks, and high-density 4-way radio shuttle AS/RS setups. All structural systems meet CE, ISO 9001:2015, and RoHS requirements, offering unmatched cost-to-performance efficiency for large-scale enterprise expansions worldwide.
SSI SCHAEFER Group
SSI Schaefer stands as one of the world's most comprehensive intralogistics providers. From static pallet racking and modular multi-tier mezzanine tiers to automated high-bay racking systems spanning over 40 meters in height, their structural designs adhere strictly to European FEM and EN 15512 safety protocols. Their strength lies in deep software-hardware integration with proprietary WMS platforms.
Mecalux S.A.
A powerhouse across the European and American intralogistics landscapes, Mecalux maintains numerous automated roll-forming and powder-coating plants. They specialize in high-capacity selective racking, mobile rack systems (Movirack), and automated pallet shuttle assemblies, backed by a proprietary engineering simulation division capable of rapid finite element analysis (FEA).
Nedcon B.V. (voestalpine Group)
As a key subsidiary of global steel group voestalpine, Nedcon combines raw metallurgical expertise with precision mechanical engineering. The brand specializes in high-complexity, tailored racking structures that serve as the backbone for complex, high-speed AS/RS shuttle systems and multi-tier picking towers throughout Europe and North America.
Dexion (Gonvarri Material Handling)
With an industrial heritage dating back to the late 1940s, Dexion pioneered the slotted angle and modern adjustable beam design. Under Gonvarri Material Handling, Dexion provides rugged pallet racking, cantilever systems, and drive-in setups engineered to perform in intense seismic risk zones across Southern Europe, the Middle East, and APAC.
Interlake Mecalux
Forming the North American arm of Mecalux, Interlake Mecalux dominates distribution centers across the USA, Canada, and Mexico. Their engineering adheres strictly to the Rack Manufacturers Institute (RMI) standards, producing high-gauge teardrop selective uprights, bolted structural systems, and push-back rack lanes for FMCG megawarehouses.
Stow Group (stow Robotics)
Stow Group operates dedicated, heavily roboticized production centers across Europe. They have built an outstanding reputation for their stow Atlas shuttle systems and modular beam connectors that feature high shear and torsional resistance. Their dedicated robotics division pairs structural steel arrays with 2D and 3D pallet shuttle fleets.
Frazier Industrial Company
Frazier is famous across the Americas as the premier structural steel pallet rack manufacturer, utilizing exclusively hot-rolled structural channel steel rather than roll-formed sheet. This grants their uprights and shelf beams exceptional abuse resistance against forklift impacts, making them the standard choice for refrigerated cold storage and heavy industrial environments.
Ridg-U-Rak, Inc.
Producing over 100 million pounds of cold-rolled steel racking annually, Ridg-U-Rak is one of the largest North American manufacturers. Known for proprietary column-reinforcing designs, heavy-duty baseplates, and advanced seismic isolation systems, they serve tier-one retail fulfillment, beverage hubs, and automotive supplier networks.
Daifuku Co., Ltd.
Consistently ranked among the top global automated material handling systems integrators, Daifuku provides ultra-high-bay rack-supported building structures (clad-rack) tightly coupled with high-speed crane AS/RS towers. Their high-tensile steel engineering delivers microscopic deflection tolerances demanded by automated stacker cranes operating at speeds exceeding 240 m/min in seismic zones across Asia, North America, and Europe.
Why Tier-1 Operations Source Direct from HEDA Shelves
With more than two decades of dedicated cold-roll forming, robotic automated welding, and multi-stage anti-corrosion coating, Guangzhou HEDA Shelves provides heavy-duty racking systems engineered to conquer demanding global logistics operational environments.
20+ Years Heavy Industrial Heritage
Founded in 2001, HEDA Shelves has completed over 10,000 warehouse projects across five continents. We solve structural layout bottlenecks for large distribution operations, third-party logistics (3PL) providers, and industrial assembly facilities.
Free 2D CAD & Full 3D Layout Simulation
Our dedicated structural engineering team develops full warehouse optimization layouts, column clearances, truck turning radii, and flue space safety envelopes at zero cost before order confirmation, ensuring zero field surprises.
Certified Metallurgy & Global Compliance
We work exclusively with certified prime structural cold-rolled steel coils. Our manufacturing processes carry verified CE Certification (No. 2435-CPR-8605159), ISO 9001:2015 Quality Management, and full RoHS eco-coating credentials.
Full 10-Stage Precision Fabrication Workflow
From automated roll-forming and CNC high-tonnage multi-hole column punching to robotic MIG beam welding, our internal line controls profile precision to sub-millimeter tolerances, ensuring structural plumb alignment on high bays.
Pickling, Phosphating & Anti-Corrosion Treatment
Steel components undergo an extensive chemical pickling and phosphating wash to strip micro-scale oxides before receiving high-build electrostatic powder curing. This provides lasting defense in harsh environments, from high coastal humidity to -30°C freezer rooms.
Export-Optimized Unitized Container Packing
Every beam tier, upright truss, and bracing pack is banded with protective corner guards, moisture wraps, and numeric pallet tags synced directly with project assembly blueprints, enabling quick container offloading and rapid jobsite erection.
Future Procurement Trends in Industrial Pallet Racking
As modern distribution shifts from manual forklift picking toward automated, algorithmically driven fulfillment, procurement teams must evaluate new technical factors before purchasing pallet storage systems.
AS/RS & 4-Way Shuttle Integration
Traditional static storage is rapidly giving way to dense automated channel setups. Modern tenders increasingly specify four-way shuttle-ready rail systems that support both semi-automated pallet shuttles and fully integrated autonomous mobile robot (AMR) platforms to decouple storage capacity from forklift operator constraints.
Digital Twins & Dynamic Deflection Sensors
Procurement teams are prioritizing structural frames capable of embedding IoT load sensors and strain gauges. These modules sync with enterprise Digital Twin software to monitor real-time beam deflection, detect unreported forklift impacts, and provide predictive maintenance alerts before structural fatigue can occur.
Low-Carbon Metallurgy & Solvent-Free Finishes
Global Scope 3 carbon accounting has turned the procurement spotlight on steel fabrication emissions. Buyers are requesting Environmental Product Declarations (EPDs), sustainably sourced scrap-blended electric arc furnace (EAF) steel coils, and zero-VOC electrostatic powder systems cured at optimized thermal cycles.
Unified Global Seismic & NFPA Compliance
With cross-border e-commerce hubs expanding across seismically active zones, buyers require unified structural compliance bridging EN 15512, RMI MH16.1, and AS 4084-2023. Layouts are pre-engineered around NFPA 13 in-rack sprinkler clearance envelopes and flue openings to streamline municipal occupancy permits.
Frequently Asked Questions on Heavy-Duty Pallet Racking Procurement
Key technical insights on steel specifications, seismic safety design, load capacities, and international regulatory compliance for warehouse engineering directors and procurement managers.
What are the key differences between cold-rolled steel and hot-rolled structural steel pallet racking? +
Cold-rolled steel pallet racking is roll-formed at room temperature from high-tensile sheet coils (such as Q235B or Q355). This allows for intricate profile shapes, variable slot configurations (like teardrop, diamond, or keyhole), high strength-to-weight ratios, and straightforward beam height adjustability. It represents the dominant standard worldwide for commercial warehouses and retail distribution hubs.
Hot-rolled structural channel racking (utilizing structural C-channels) is formed under high heat, yielding thicker webs and flanges. While substantially heavier and carrying higher initial material and freight costs, hot-rolled steel delivers higher resistance to heavy forklift impacts, making it popular for demanding cold-storage facilities, outdoor yards, and harsh industrial environments.
Which international structural design standards govern high-capacity pallet racking safety? +
Pallet racking engineering is governed by three primary global structural codes:
1. EN 15512 / EN 15620 / EN 15629 (Europe): Specifies the structural calculation parameters for steel static pallet racking, including partial load factors, beam-to-column rotational stiffness tests, and dynamic deformation tolerances under full service loads.
2. RMI (ANSI MH16.1) (North America): Developed by the Rack Manufacturers Institute, this standard mandates cold-formed steel structural design methodologies, seismic baseplate considerations, and safety factors for column uprights, baseplates, and load-bearing shelf beams.
3. AS 4084:2023 (Australia): The updated Australian standard governing steel storage racking, mandating strict design testing methods, seismic verification, and operational clearance boundaries.
How does local seismic zoning affect baseplate design, upright profiling, and floor anchor engineering? +
In high seismic zones (such as areas governed by IBC Seismic Design Categories D, E, or F), dynamic ground acceleration introduces significant horizontal shear forces and overturning moments into the racking structure. To absorb these forces safely:
• Baseplates are enlarged and thickened from standard 6 mm plates to heavy-duty 10–16 mm ductile plates to distribute tensile anchoring forces over a larger concrete slab footprint.
• Anchor bolts transition from mechanical wedge anchors to high-embedment epoxy chemical anchors to prevent shear pullout under cyclic loading.
• Upright profiles use heavier steel wall thicknesses and deeper section profiles to control story drift and frame sway, keeping system deflections within safe, ductile limits.
What anti-corrosion surface treatments are recommended for high-humidity coastal sites or cold-storage freezer operations? +
For standard temperature-controlled warehouses, a high-grade chemical pickling, phosphating, and thermoset electrostatic powder coating provides strong barrier protection. However, specialized environments require upgraded finishes:
• Deep Freeze Warehouses (-20°C to -30°C): Standard powder-coated steel performs reliably if pre-treated properly, but components must be manufactured using steel grades certified for low-temperature Charpy V-notch impact toughness to prevent cold-embrittlement fractures.
• High-Humidity Coastal or Fertilizer Facilities: Hot-dip galvanizing (HDG) per ASTM A123 or EN ISO 1461, providing 65–85 μm of metallurgical zinc-iron alloy bonding, provides long-term galvanic self-healing protection that prevents rust creep if the surface is scratched.
What parameters must be provided to complete an accurate 2D/3D warehouse layout and structural calculation? +
To design an efficient, code-compliant storage layout, our engineering team requires:
1. Architectural CAD drawing indicating clear height under roof joists, building column grid spacing, perimeter walls, dock doors, fire exits, and floor expansions.
2. Pallet dimensions and weight profiles, including width, depth, overall load height (including wooden/plastic skid), and maximum dynamic unit weight.
3. Material Handling Equipment (MHE) specs, including forklift model, turning radius (Aisle Width Minimum requirement), maximum mast lift height, and top-tier mast derating curves.
4. Fire Protection Details, specifying in-rack sprinkler supply plans, longitudinal and transverse flue space requirements (per NFPA 13 rules), and concrete slab compressive strength (F-min/FF/FL numbers).
How does HEDA Shelves coordinate international containerized shipping and on-site assembly validation? +
HEDA Shelves manages end-to-end logistics from factory container loading directly to major international container ports. Structural components are organized into unitized, weather-wrapped bundles tagged with individual barcode numbers matched to the engineering bill of materials (BOM).
Every shipment includes step-by-step 3D assembly shop drawings, torque tightening schedules for column-to-baseplate bolts, and remote video technical supervision. For major high-bay or mezzanine installations, certified factory project supervisors can be dispatched on-site to verify plumb tolerances and inspect mechanical beam locks prior to system hand-over.
Accelerate Your Warehouse Capacity Planning Today
Whether you are designing a high-density 4-way shuttle AS/RS hub, upgrading selective storage rows, or expanding your distribution network, our engineering team provides structural calculations and CAD layouts tailored to your exact specs.