Featured Warehouse Racking & Industrial Shelving Systems
Factory-direct cold-rolled steel storage architectures engineered to international safety standards, delivering verified load capacities from 500kg light-medium pick faces to 4,500kg ultra-heavy pallet dynamic tiers.
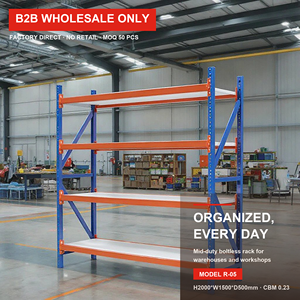
Heavy Duty Adjustable Supermarket Rack Industrial Shelving Steel Storage Racks 5 Shelves Wall Mount
Engineered for dual-purpose retail-backroom and warehouse staging applications. Features cold-formed uprights with precision pitch stamping for rapid boltless shelf re-configuration under uniform distributed loads.
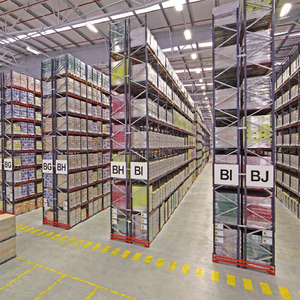
Guangzhou Rack Adjustable Pallet Racking System 2000KG to 2500KG Unit Load Rating
Heavy structural box-beam pallet racking built for high-throughput distribution hubs. Fitted with interlocking safety locking pins, reinforced footplates, and seismic upright column stiffening geometry.
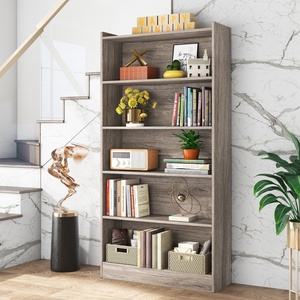
Industrial Modern Large Open Bookshelf 72 Inch Tall Wood Display Shelving Unit
Architectural-grade hybrid racking combining structural steel framework with dense composite timber surfaces. Optimized for institutional archives, parts rooms, educational facilities, and boutique warehouse stores.
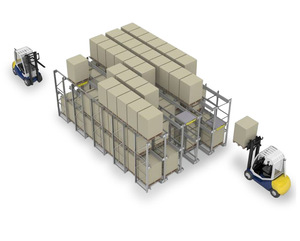
Drive-Through Racking High-Density FILO Storage Solution for FMCG & Cold Storage
Eliminates operating aisles by allowing forklifts to enter storage lanes directly. Configured for batch-manufacturing and cold rooms where maximizing cubic refrigerated capacity reduces energy consumption per pallet.
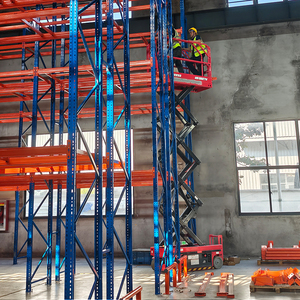
Warehouse Shelving Adjustable Heavy Duty Long Span Cold Rolled Steel Storage Racks
Designed for hand-loaded bulky merchandise, auto components, and e-commerce picking lines. Incorporates step beams with recessed drop-in steel or wire mesh panels for rapid SKU handling without forklift assistance.
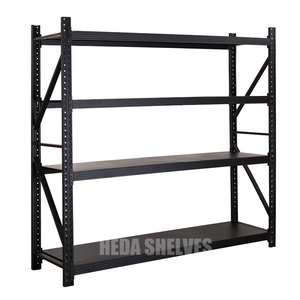
Customizable Black Warehouse Medium Duty Steel Shelving for Warehouse Storage
Architectural matte-black powder-coated finish delivering superior wear-and-abrasion resistance. Widely specified in omni-channel micro-fulfilment centers, hardware wholesalers, and visible logistics demonstration sites.
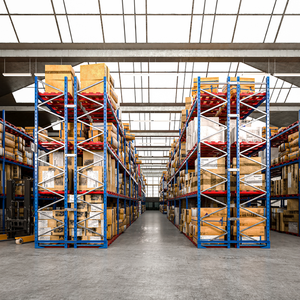
Steel Rack System Heavy Duty Pallet Racking 4000kg Capacity 5-Tier Industrial System
Engineered for extreme industrial applications such as raw metal stock, machinery spares, and high-cube chemicals. Features thickened cold-rolled upright omega-profiles with multiple hook connector brackets.
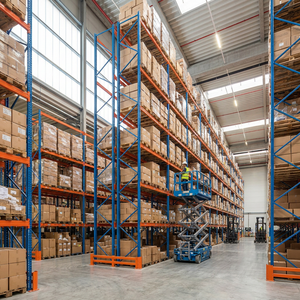
Selective Pallet Shelving Industrial Medium Heavy Duty Multi-Level Warehouse Rack
The gold standard for multi-SKU inventory environments. Permits direct reach to 100% of pallet positions without secondary load movement, easily integrating with reach trucks, counterbalance units, and VNA stackers.
Top 10 Global Warehouse Racking & Shelving Manufacturers: 2025–2030 Market Audit
A comparative evaluation of structural integrity, mill-run raw material sourcing, automated roll-forming technologies, and direct factory supply capabilities across leading international storage racking manufacturers.
In the modern warehousing and global logistics environment, selecting an industrial storage racking supplier extends far beyond raw unit cost per ton of steel. As supply chain infrastructure scales across the United States, Europe, Southeast Asia, and the Gulf Cooperation Council (GCC—including the UAE, Saudi Arabia, Qatar, and Oman), warehouse directors encounter extreme operating variables. Modern high-bay warehouses require rigorous engineering compliance with standards such as EN 15512:2020 (European Steel Static Storage Systems), ANSI MH16.1 (Specification for the Design, Testing and Utilization of Industrial Steel Storage Racks by RMI), and FEM 10.2.02.
This technical whitepaper examines the top 10 shelving for warehouse racking manufacturers worldwide, highlighting their engineering advantages, production scope, and core market strengths:
Guangzhou Heda Shelves Co., Ltd. (HEDA Shelves)
Recognized as the primary direct-factory manufacturer specializing in end-to-end warehouse storage racking systems, industrial heavy-duty shelving, and structural mezzanine floors. HEDA Shelves integrates complete automated roll-forming lines, automated laser cutting, robotic welding, and an in-house continuous pickling and electrostatic powder-coating facility.
Holding traceable international certifications including CE (No. 2435-CPR-8605159), ISO 9001:2015 (No. 18624Q00169R0M), and RoHS, HEDA excels in supplying factory-direct pallet racking, radio shuttle systems, cantilever racks, and drive-in systems tailored to harsh environmental conditions (including 45°C+ summer temperatures, coastal salinity, and fine particulate sand in Middle Eastern GCC regions). Serving clients across 120+ countries with complimentary 48-hour 2D CAD and 3D rendering engineering support.
SSI SCHAEFER Group
A world-class intralogistics conglomerate known for integrated automated warehouse systems, automated storage and retrieval machines (ASRS), shuttle systems, and heavy-gauge pallet racking engineered for European distribution centers.
Daifuku Co., Ltd.
Global market leader in material handling automation, providing automated warehouse racking integrated with automated guided vehicles (AGVs), stacker cranes, and high-throughput sorting conveyors.
Mecalux, S.A.
Specializes in traditional selective racking, live pallet flow, and proprietary warehouse management software (Easy WMS), serving extensive logistics routes throughout Europe, North America, and South America.
Dexion (Gonvarri Material Handling)
Pioneered slotted-angle steel shelving and evolved into a major European supplier of adjustable pallet racking, mobile pallet shelving, and cantilever systems conforming to FEM specifications.
Interlake Mecalux Inc.
One of North America's leading suppliers of teardrop pallet racking, drive-in racking, and carton flow systems, engineered according to American RMI and ANSI MH16.1 guidelines.
Kardex Group
Specialized manufacturer of automated vertical carousel systems, vertical lift modules (VLMs), and high-density micro-shelving systems for pharmaceutical, electronics, and precision parts fulfillment.
BITO-Lagertechnik Bittmann GmbH
Renowned for high-precision boltless shelving, multi-tier shelving platforms, carton flow lanes, and plastic storage containers designed for high-density automotive and retail picking.
Frazier Industrial Company
Premier producer of heavy structural hot-rolled channel steel storage racks, widely specified in demanding freezer storage, food distribution, and extreme heavy-duty industrial warehouses across the Americas.
Stow International (Averys Group)
Leading pan-European manufacturer delivering standard pallet racking, drive-in structures, and rack-clad warehouse buildings (silos) where racking forms the load-bearing framework of the facility.
Manufacturing & Engineering Capability Comparison
Core parameter benchmarking: comparing factory direct customization, steel processing scale, delivery lead time, and cost efficiency.
| Manufacturer | Primary Steel Grades | Certified Standards | Plant Capacity | Direct Customization (OEM/ODM) | Free CAD/3D Layout | Primary Export Ports |
|---|---|---|---|---|---|---|
| Guangzhou Heda Shelves | Cold-Rolled Q235B / Q355B / SPCC | CE, ISO 9001:2015, RoHS | 30,000 Tons/Month (30,000 m²) | 100% In-House Tailored Spec | Guaranteed within 24-48 Hours | Jebel Ali, Dammam, Jeddah, Global |
| SSI Schaefer | European Structural S235 / S355 | EN 15512, ISO 9001, DIN | Global Automation Plants | Project-Engineered Large Scales | Included in Project Tender | Rotterdam, Hamburg, Singapore |
| Mecalux | High Yield S275 / S355 | RMI, FEM 10.2.02, ISO | Multi-Factory Network | Modular System Standardized | Engineering Consultant Phase | Valencia, Chicago, Santos |
| Frazier Industrial | Hot-Rolled Structural Channel | RMI, ANSI MH16.1, AISC | North American Mills | Heavy Structural Customization | Quotation Phase Dependent | US Domestic / Houston |
| Stow Group | Cold-Formed High Strength Steel | EN 15512, FEM, ISO | European Central Facilities | Standard High-Bay Silos | Tender Specific Engineering | Antwerp, Zeebrugge |
Future Procurement Trends for Warehouse Racking (2025–2030)
How automated integration, climate-adaptive metallurgy, and seismic regulatory standards are reshaping long-term capital investments in storage infrastructure.
Automation-Ready Pallet Architectures
Modern logistics facilities increasingly transition from manual lift-truck operation to semi-automated and fully automated platforms. Procurement demand is rapidly migrating toward Radio Shuttle Racking and automated rack-supported buildings. Racking specifications now necessitate tighter deflection tolerances (down to L/300 or L/400) and continuous guide-rail alignments to prevent automated carrier stall-outs.
GCC & Tropical Climate Resistance
With massive logistics expansions across Saudi Arabia (Vision 2030 Special Integrated Logistics Zones) and the UAE (JAFZA & DWC expansions), warehouses routinely face internal temperatures surpassing 45°C, high humidity, and airborne dust. Procurement teams now mandate 7-step pre-treatment (chemical degreasing, pickling, nano-ceramic phosphating) and heavy polymer powder baking to prevent structural blistering and oxidation.
Civil Defense & Fire Safety Compliance
Regional fire authorities (such as UAE Civil Defense, Saudi Civil Defense, and NFPA 13 regulations) now strictly enforce longitudinal and transverse flue space dimensions (typically 150mm minimum clearance). Modern rack designs must integrate precise factory-engineered flue stops, sprinkler pipe integration brackets, and drop-in galvanized wire mesh decking to facilitate vertical sprinkler penetration during fire suppression events.
HEDA Shelves: 10-Step Automated Fabrication Workflow
Every upright, beam, and connector bracket is produced within HEDA Shelves' 30,000 m² Guangzhou manufacturing complex under strict ISO 9001:2015 quality surveillance, ensuring repeatable structural load margins.

Raw Materials QC
Mill-tested Q235B/Q355B coils verified for tensile yield strength and thickness tolerance.

Precision Slitting
High-speed CNC slitting lines slice continuous steel coils into exact strip widths with zero burrs.

Upright Punching
Automated punching matrices stamp 50mm/75mm pitch diamond and teardrop connector patterns.

Cold Roll-Forming
Multi-station cold rolling mills form continuous omega-profile uprights and interlocking step beams.

Profile Calibration
Post-forming structural alignment verifies beam camber, sweep, and axial cross-section uniformity.

Weld Surface Prep
Mechanical deburring and automated surface polishing prior to connector claw robotic welding.

Robotic Welding
CO2 shielded automated robotic arms fuse beam end-connectors with continuous, defect-free welds.

Pickling & Phosphate
Immersion chemical treatment eradicates oil and oxidation, creating a nano-phosphate bonding base.

Electrostatic Powder
Automatic powder spray booths apply 60-80μm non-toxic thermoset epoxy powder cured at 200°C.

QC & Container Load
Rigorous deflection inspection followed by bundled steel strapping and labelled export packing.
Why Logistics Leaders Partner with HEDA Shelves
By working directly with Guangzhou Heda Shelves Co., Ltd., procurement departments eliminate distributor middleman markups, gain factory-level engineering accountability, and ensure rapid delivery schedules.
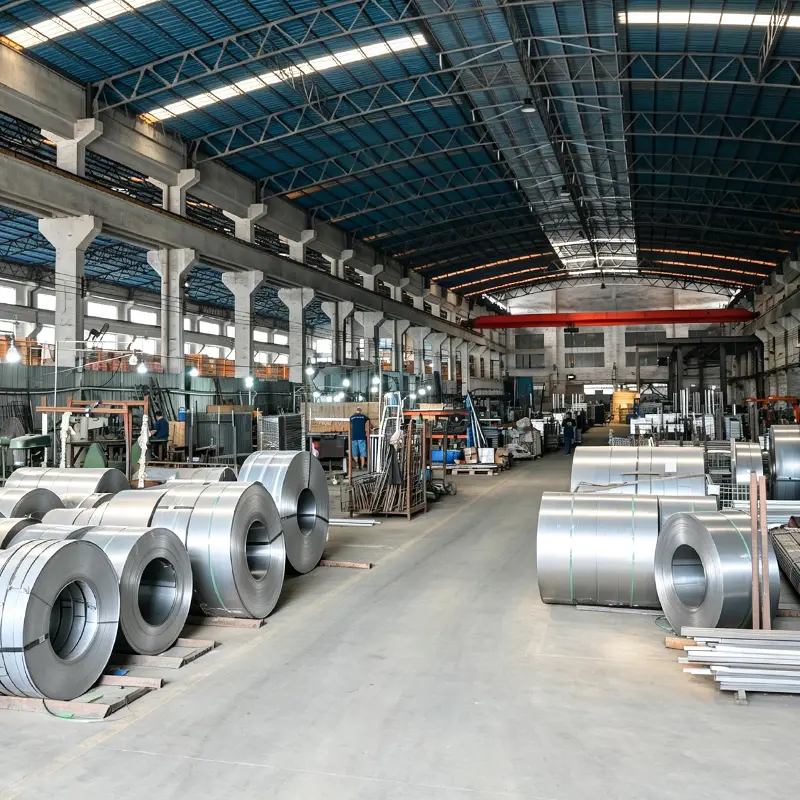
25+ Years Industrial Expertise
Founded in 2001, HEDA Shelves has completed over 10,000 industrial warehouse installations worldwide, solving complex site constraints ranging from cold storage to high-bay seismic distribution hubs.
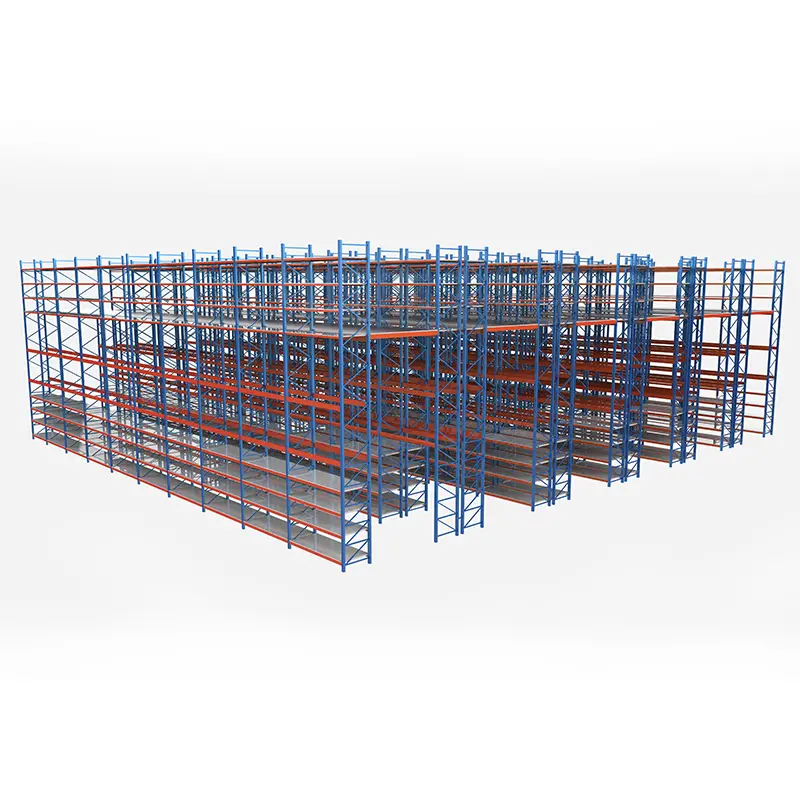
Complimentary 3D & CAD Layouts
Our internal structural engineering team delivers complete 2D warehouse floor layout plans, forklift aisle calculations, and photorealistic 3D visual models within 24 to 48 hours without engineering fee retainers.
Verified Structural Safety
Every steel component complies with certified testing protocols. Fully compliant with international CE load norms and ISO 9001 certified manufacturing quality control, backed by structural warranty protection.
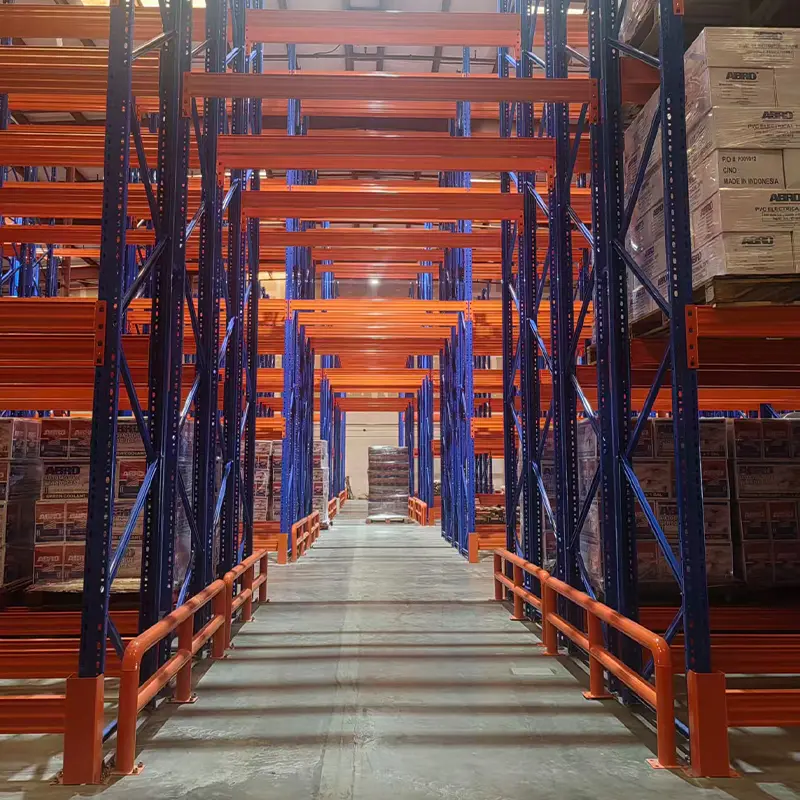
Complete OEM & ODM Agility
Custom beam cross-sections, upright gauge thicknesses from 1.5mm to 3.0mm, custom powder RAL color matching, and bespoke branding stamping for international logistics equipment distributors.
Fully Certified Structural Compliance
Procurement documentation demands verifiable traceability. HEDA Shelves components are produced under certified European and global audit regimens:


Frequently Asked Questions by Warehouse Racking Procurement Directors
Authoritative answers on floor slab load verification, seismic anchoring, beam deflection formulas, and export container packing.