Featured Industrial Track-Guided & Dynamic Pallet Rack Systems
Engineered in our 30,000 m² state-of-the-art manufacturing facility, our floor-track mobile bases and dynamic roller track solutions eliminate redundant aisles, expanding pallet capacity by up to 85%–100% while retaining continuous inventory accessibility.
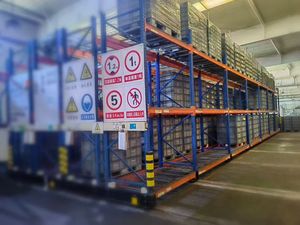
Mobile Pallet Racks Guided by Fixed Tracks (AR Mobile System)
Motorized mobile bases mounted on heavy-duty steel floor tracks. Eliminates static service aisles, opening a single moving access aisle on demand via remote control or automated warehouse management interface.
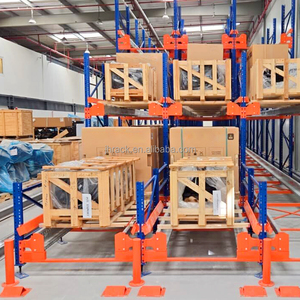
Automated Four-Way Pallet Shuttle & Radio Track Carrier Rack
Self-powered intelligent pallet shuttles traversing precision-formed structural steel running rails inside deep racking channels. Drastically reduces forklift operating cycles and eliminates in-rack structural collisions.
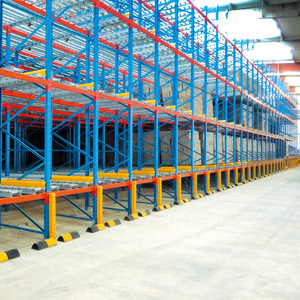
Heavy Duty Steel Gravity Pallet Racking with Adjustable Roller Track
High-throughput First-In, First-Out (FIFO) dynamic gravity system. Pallets glide down inclined steel roller tracks with integrated centrifugal brake rollers and entry-exit safety pallet separators for batch tracking.
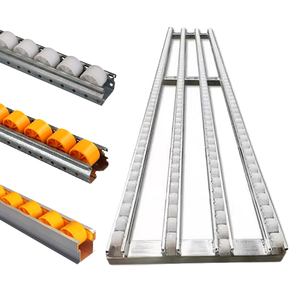
Industrial Aluminium Roller Track Pallet Flow & Heavy Rolling Rail Rack
Engineered extruded aluminium rolling tracks with reinforced multi-rib wheel assemblies. Designed for smooth, low-noise conveyance of Euro and GMA pallets across manufacturing buffer zones and order fulfillment areas.
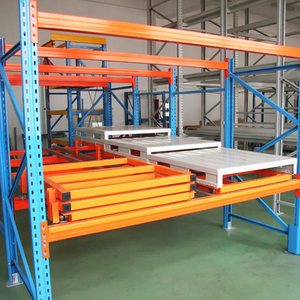
Q235B Push Back Pallet Racking with Nested Rolling Track Carts
Nested cart system riding on inclined structural steel channels. Front loading pushes back previously deposited unit loads along guiding tracks. Ideal for multi-SKU consolidation with immediate lane-level pick selectivity.
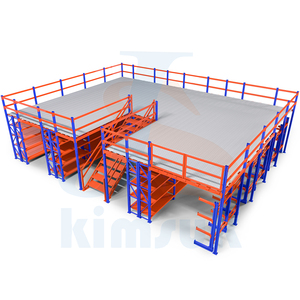
Rack-Supported Heavy Duty Steel Mezzanine & Attic Storage Platform
Converts unused vertical warehouse cubic space into fully operational multi-level picking floors supported by heavy-duty pallet racking frames. Features cold-rolled decking, integrated safety handrails, and pallet drop gates.
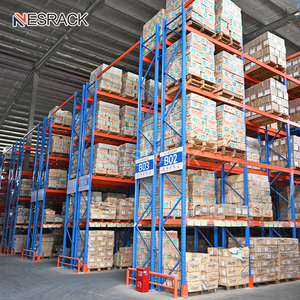
Adjustable Boltless Selective Industrial Pallet Racking System
The benchmark universal pallet handling system. Manufactured with cold-rolled upright omega sections and step box beams with 5-tooth connectors, offering structural stability for general manufacturing, 3PL, and retail distribution centers.
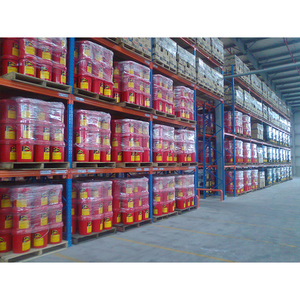
High-Capacity Structural Steel Beam Warehouse Logistics Rack System
Designed for heavy industrial environments requiring extreme weight distribution across wide spans. Compatible with wire mesh decks, pallet support crossbars, column protectors, and frame barrier safety systems.
Structural Principles & Mechanical Architecture of Pallet Racks on Floor Tracks
Modern intralogistics demands maximum cubic footprint density without sacrificing SKU accessibility. Conventional static selective racking configurations dedicate up to 65% of warehouse floor footprint to dead forklift transit aisles. Pallet racks on tracks—frequently classified as Motorized Mobile Racking (MOVO) or Dynamic Rail-Guided Track Storage—fundamentally transform structural logistics by mobilizing heavy-duty racking blocks on mechanical running wheels along floor-embedded guidance rails.
By consolidating entire racking banks into a compact, contiguous cluster, only a single dynamic operating aisle needs to be opened at any specific retrieval cycle. Floor-embedded guide tracks absorb massive localized dynamic wheel point loads (often exceeding 80 kN per wheel assembly) while maintaining horizontal track-gauge deflection tolerances below 1:1000 over extensive spans. This achieves a 100% increase in pallet storage volume within identical spatial parameters while drastically reducing operating overhead in temperature-controlled cold storage facilities.
Kinematic Track & Guidance Specifications
- Rail Profiles: Machined inverted crane rail (DIN 536 A45/A55) or grooved precision-milled steel guides.
- Base Drive Units: Direct-drive hollow-shaft geared motors with soft-start variable frequency inverters (VFD).
- Laser Floor Flatness: Concrete slab tolerances adhering strictly to DIN 18202 Group 4 / EN 15620 specifications.
- Safety Architecture: Integrated Class 4 optical light curtains, ultrasonic presence sensors, and physical crawl-stop trip bars.
Comparative Matrix: Storage Density, Capital Expenditure & Operating Kinematics
When evaluating mobile pallet racks on tracks against standard static systems and automated shuttle configurations, warehouse planners must weigh floor area utilization against handling cycle times and overall system capital expenditure (CAPEX).
| Racking Architecture | Floor Space Efficiency | Direct Selectivity | Cold Store Energy Savings | Civil Floor Requirements | Safety Integration Tier |
|---|---|---|---|---|---|
| Mobile Pallet Racks on Tracks | 85% – 92% (Maximum) | 100% Individual Pallet Access | 40% – 50% Reduction | Recessed Precision Tracks | Full Safety Light Curtains + PLC |
| Conventional Selective Rack | 35% – 45% (Low) | 100% Individual Pallet Access | 0% Baseline | Standard Industrial Slab | Passive Upright Protectors |
| Drive-In Pallet Racking | 65% – 75% (Moderate) | Strict LIFO (Poor) | 20% – 30% Reduction | Standard Floor Slab | Guide Rails on Uprights |
| Radio Pallet Shuttle on Rails | 80% – 88% (High) | Channel Level Access (FIFO/LIFO) | 35% – 45% Reduction | Level Industrial Slab | Autonomous Sensor Safety |
| Gravity Roller Pallet Flow | 70% – 82% (High) | Strict FIFO Rotation | 25% – 35% Reduction | Standard Level Floor | Centrifugal Speed Regulators |
Future Procurement & Technological Trends in Rail-Guided Pallet Racking (2025–2030)
Procurement directors and warehouse supply chain architects are shifting away from static racking assets toward responsive, automated, and energy-conscious storage infrastructures. The following strategic trends dictate modern capital equipment sourcing.
WMS/ERP IoT Interoperability
Next-generation pallet racks on tracks feature native PLC-to-WMS wireless integration. Aisle opening sequences are pre-calculated based on incoming picking batch waves, automated guided vehicle (AGV) dispatch paths, and enterprise inventory turnover velocities, cutting retrieval latency by 35%.
Cold Chain Energy Optimization
With electrical cooling costs representing over 65% of frozen logistics operational expenditures, compacting chilled storage space via motorized track racks reduces cubic refrigerated air volume by nearly half. Smart sleep-mode ventilation cycles maintain air circulation across parked racks during off-peak hours.
Dynamic Pre-Engineered Track Tolerances
Modern factories now deliver integrated dual-purpose guide rails that handle both heavy wheel rolling compression and seismic uplift moments. Laser-machined anchor channels and non-shrink self-leveling epoxies guarantee track longevity even under continuous multi-shift operations.
Green Steel Metallurgy & Carbon Accounting
Top global procurement teams require carbon disclosure certifications. Modern manufacturing utilizes premium cold-rolled Q235B and Q355B structural steel produced via electric arc furnace (EAF) recycling, cutting embodied carbon emissions while preserving tensile yield strengths exceeding 355 MPa.
Hybrid AGV-Rail Synergy
Modern facilities increasingly combine floor-track mobile systems with automated guided vehicles (AGVs) and autonomous mobile robots (AMRs). Photoelectric sensors synchronize with vehicle fleet dispatchers to ensure aisle readiness long before the transport robot arrives at the picking face.
Predictive Maintenance Sensor Arrays
Smart motor gearboxes embedded on mobile wheel chasses monitor mechanical vibration frequencies, wheel bearing heat thresholds, and motor amp spikes. Cloud diagnostics warn facilities managers of track debris or component fatigue long before any mechanical stoppage occurs.
Guangzhou HEDA Shelves: Enterprise Advantages & Precision Manufacturing
Since 2001, Guangzhou Heda Shelves Co., Ltd. has stood at the forefront of global warehouse storage engineering. With an enterprise footprint spanning over 30,000 square meters, a dedicated technical workforce exceeding 300 professionals, and a verified monthly production capability of 30,000 metric tons, we provide end-to-end turnkey OEM/ODM engineering across six continents.
Fully Traceable 10-Stage Production Sequence
Quality control is embedded directly into our automated fabrication cycle. Raw hot-rolled and cold-rolled steel coils undergo spectrographic chemical analysis before entering automated multi-station cold roll-forming lines. Profile precision punching maintains hole-pitch tolerances within ±0.1 mm over a 12-meter upright length.
Components undergo continuous robotic welding, followed by multi-stage chemical pretreatment: acid pickling, degreasing, and zinc phosphating. This guarantees deep electrostatic powder coating adhesion resistant to coastal salt fog and extreme humidity (tested up to 500 hours under ASTM B117 salt spray criteria).
Rigorous International Certifications
- ✔ CE Structural Certification: EN 1090-1 & No. 2435-CPR-8605159
- ✔ ISO 9001:2015 Quality System: Reg. No. 18624Q00169R0M
- ✔ RoHS Eco-Compliant: Heavy-metal-free thermosetting resin finishes
- ✔ FEM / RMI Compliance: Designed to FEM 10.2.07 & ANSI MH16.1 codes
Frequently Asked Technical & Procurement Questions (FAQ)
Clear, engineer-backed answers addressing civil floor slab tolerances, installation methodologies, safety interlocks, and international freight containerization.